CNC Machining Services China
CNC Turning Services
CNC turning for round, threaded and rotational metal parts — shafts, bushings, pins, sleeves and fittings. From drawing review and prototypes through repeat production.
Direct answer: CNC turning is used for rotational metal parts such as shafts, bushings, pins, sleeves and threaded fittings. Balford reviews material, datums, threads, grooves and production volume before quoting a prototype-to-production route. Non-rotational features are handled by milling, either with live tooling or in a coordinated second operation.
Typical Turned Parts
Shafts
OD/ID and length control with shared datum, runout check and straightness review.
Bushings & sleeves
Concentric bores, thin walls and press-fit tolerances reviewed against material and stock form.
Pins & fittings
Threaded and grooved fittings for fluid, valve and assembly applications.
Threaded components
Thread standard and class confirmed with the drawing before quoting.
Turning Design Checklist
- Critical OD/ID datums shared across features
- Thread standard and class (ISO metric, UNC/UNF, NPT)
- Groove geometry and tolerances
- Concentricity and runout requirements
- Surface finish (Ra and location)
- Material grade and hardness
Turning vs. Other Machining Processes
Use this quick decision aid when routing a new part:
- Rotational symmetry around one axis → CNC turning
- Non-rotational faces, pockets or holes → CNC milling or live-tool turning
- Complex cavities or multi-surface geometry → CNC milling
- Narrow slots, small corners or hardened material → wire EDM
Parts that mix rotational and prismatic features are often turned first, then milled. See combined CNC machining services.
Materials for Turned Parts
Stainless steel
Corrosion-resistant shafts, sleeves and fittings; work hardening is managed with controlled feeds. See stainless steel turned parts.
Aluminum
Lightweight rotational parts with good machinability; alloy and temper drive thread quality and anodizing. See aluminum turned parts.
Carbon and alloy steels
Shafts and structural parts with predictable machining; hardness and heat treatment set allowances. See carbon steel shafts and fittings.
Copper and brass
Conductive and fluid components with burr control on threads and seals. See copper turned components and brass turned components.
Applications
Automotive and mobility
Sensor sleeves, injector parts, fittings and motor components with repeatable concentricity. See automotive machining.
Fluid and valve systems
Threaded fittings, valve seats and sealing interfaces. See solenoid valve components.
Industrial equipment
Rotational machine components and tooling details. See industrial machining.
Electrical products
Brass and copper rotational parts for conductive assemblies. See electronics components.
Related Case Studies
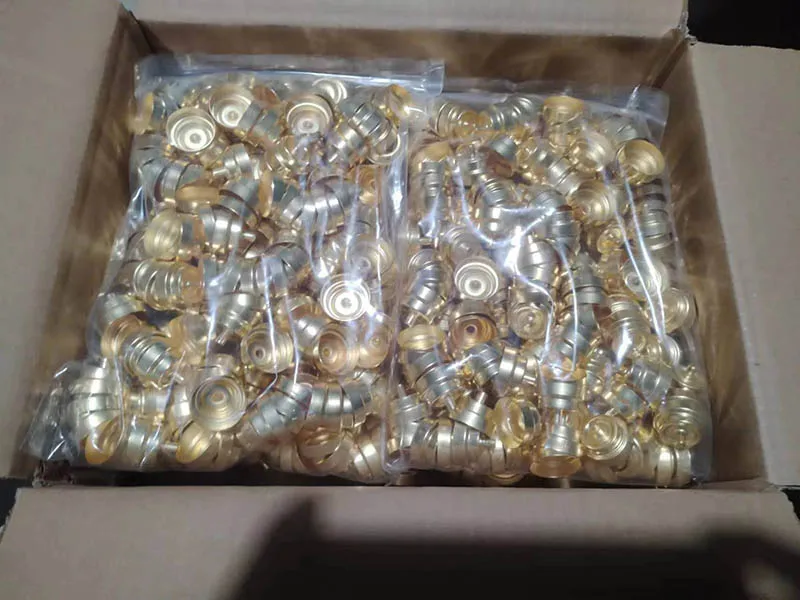
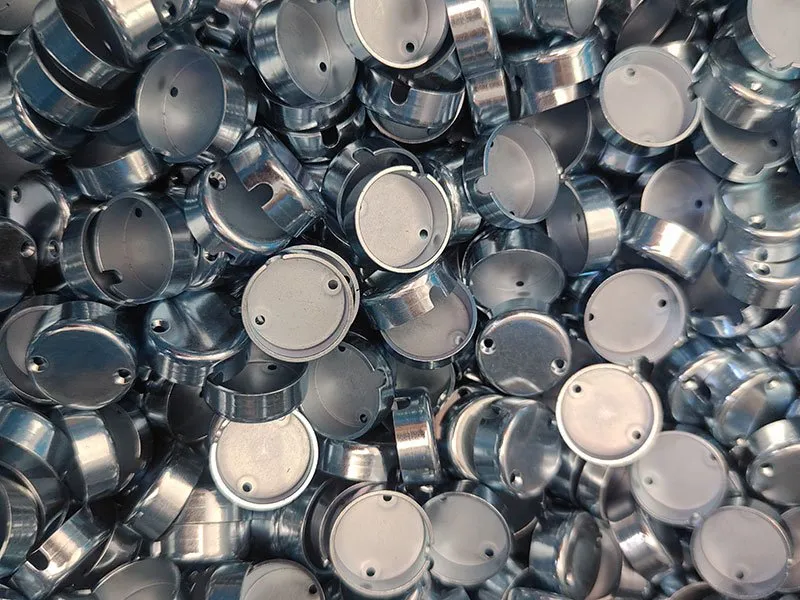
Selected turning-related projects from Balford’s production history; each case shows the machining step inside a full route.


Browse the full case study library →
Compliance and Quality
- Automotive material compliance — IMDS, REACH, RoHS and GADSL for automotive programs.
- Balford IMDS process — material data from quotation to delivery.
- IMDS compliance checklist — 15 steps for automotive suppliers.
- Quality and certifications — ISO 9001:2015 and IATF 16949-aligned controls.
Frequently Asked Questions
What parts are best for CNC turning?
Rotational parts: shafts, bushings, sleeves, pins, fittings and threaded components. If the geometry is round or rotational and most critical features share one axis, turning is usually the most efficient route; non-rotational features can be added by milling with live tooling or in a second operation.
What tolerances can CNC turning hold?
Tolerances are confirmed against the drawing during DFM review rather than quoted as blanket values. Feature-specific callouts for OD/ID, concentricity, runout, threads and surface finish are reviewed against the material, stock form and quantity before quoting.
Can you machine threads and grooves?
Yes. We review the thread standard and class (ISO metric, UNC/UNF, NPT where applicable), groove geometry and tolerances against the material properties so cycles stay repeatable part to part.
Which materials do you turn?
We machine aluminum, carbon and alloy steels, stainless steels, copper and brass, and selected engineering plastics and special alloys. Grade, hardness and stock form are confirmed per project.
Do you combine turning with other processes?
Yes. Turned parts can be completed with milling features (live tooling or second setup), grinding, knurling, surface treatment, heat treatment and assembly. We review the full route so the datum and setup plan stays clear.
What do you need to quote a turned part?
Matching 3D and 2D files at the same revision, material grade, finish, prototype quantity, expected batch size and annual demand. Mark critical diameters, threads and datums so the setup is built around the assembly.
Secure Project Review
Send Balford Your Drawing
NDA before detailed file exchange. Drawing-based DFM review. Prototype-to-production route. Check the RFQ checklist before sending files.
Round punches, core pins and other turned tooling components are produced in-house on Balford’s lathes.