CNC Machining Services China
Wire EDM Services
Precision wire EDM for hard materials, intricate profiles, narrow slots and tooling components. Low-force cutting with tight tolerances, from DFM review through repeat production.
Direct answer: Wire EDM services are used for features that a rotating cutter cannot reach economically: intricate through profiles, narrow slots, sharp internal corners, hardened tooling components and thin sections where cutting force would cause distortion. Balford reviews start hole, corner radius, taper, skim cuts and inspection access before quoting a prototype-to-production route, and combines wire EDM with milling where bulk removal comes first.
Typical Wire EDM Parts
Hardened tooling parts
Cut after heat treatment without annealing the material.
Narrow slots & intricate profiles
Features milling cannot reach with a practical tool.
Through features
Precise through profiles with controlled corner radius.
Low-force parts
Thin or delicate sections that would distort under cutting force.
Wire EDM Design Checklist
- Start hole position and diameter for internal profiles
- Corner radius requirement (sharp vs. practical)
- Profile complexity and taper requirements
- Skim passes for surface condition and tolerance
- Recast layer / surface condition expectations
- Inspection access for the finished contour
Wire EDM vs. Milling
Use this quick decision aid when routing a new part:
- Hard material or finished hardened part → wire EDM
- Sharp internal corner or narrow slot → wire EDM
- Large stock removal on an open profile → CNC milling
- Rotational geometry → CNC turning
For drawing-level guidance see the wire EDM machining guide.
Materials for Wire EDM
Hardened tool steel
Finished tooling components cut without annealing. See special alloy wire EDM.
Stainless steel
Precise profiles in corrosion-resistant material. See stainless steel wire EDM.
Conductive alloys
Copper, brass and conductive special alloys for electrode and connector work. See copper machining.
Carbide and hard materials
Evaluated per application; wire EDM is the practical route where milling cannot cut. See special alloys.
Applications
Tooling and dies
Profiles and details on tooling components that need burr-free, low-force cutting.
Automotive components
Precision contours and hardened parts in vehicle systems. See automotive machining.
Valve and fluid systems
Narrow slots and sealing features on valve components. See solenoid valve components.
Sensor and electronics parts
Small precision features in sensor and motor assemblies. See electronics components.
Related Case Studies
Selected projects that combine wire-cut or precision-contour work with other Balford processes; each case shows the machining or trimming step inside a full route.

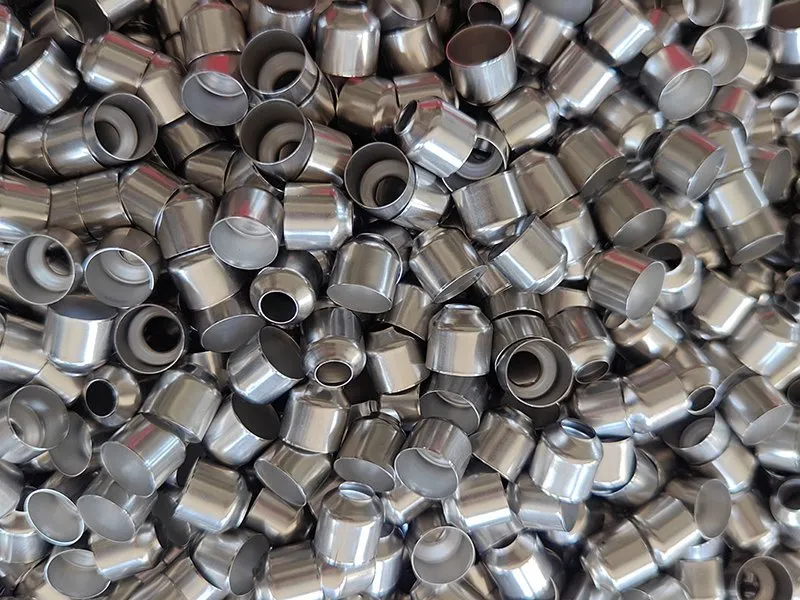
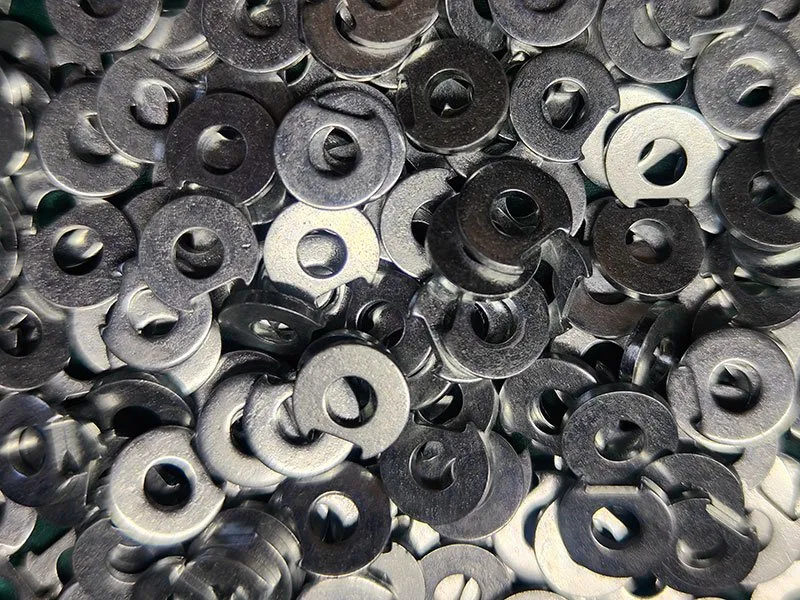

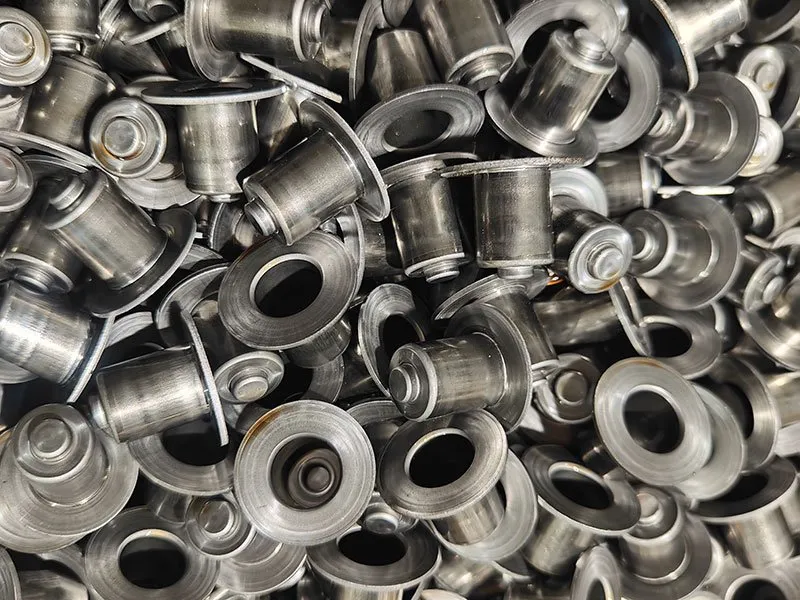
Browse the full case study library →
Compliance and Quality
- Automotive material compliance — IMDS, REACH, RoHS and GADSL for automotive programs.
- Balford IMDS process — material data from quotation to delivery.
- IMDS compliance checklist — 15 steps for automotive suppliers.
- Quality and certifications — ISO 9001:2015 and IATF 16949-aligned controls.
Frequently Asked Questions
What parts are best for wire EDM?
Parts with features a rotating cutter cannot reach economically: intricate through profiles, narrow slots, small corner radii, hardened material and thin sections where cutting force would cause distortion. Wire EDM cuts only electrically conductive materials.
Do I need a start hole?
For internal profiles, yes — the wire must pass through the material, so a start hole is required. For external contours the wire can start from outside the blank. We confirm the start-hole position and diameter during DFM review.
What corner radius can wire EDM hold?
Wire EDM can produce very small corner radii — far smaller than a milling cutter — which is why it is chosen for sharp internal corners. The practical limit depends on wire diameter and the number of passes; we confirm against the drawing rather than quoting a blanket value.
Can wire EDM cut hardened material?
Yes. Wire EDM cuts hardened tool steel and other hard conductive materials without annealing them, which makes it the standard route for finished tooling components and hardened parts. It also avoids the cutting forces that can distort thin or delicate sections.
What is a skim cut and when is it needed?
A skim cut is a low-energy finishing pass that improves surface condition, geometry and recast-layer control after the main cut. We plan skim passes when the drawing calls for tighter tolerance or better surface finish.
How does wire EDM compare with milling on open profiles?
For open profiles with large stock removal, milling is faster and cheaper. Wire EDM is selected when the feature is hard to reach, very narrow, needs a sharp corner, or is in hardened material. The two are often combined: milling removes bulk, wire EDM finishes the critical contour.
Secure Project Review
Send Balford Your Drawing
NDA before detailed file exchange. Drawing-based DFM review. Prototype-to-production route. Check the RFQ checklist before sending files.
Wire EDM capacity in the tool room, along with grinding, CNC and heat treatment, is listed on the equipment list.