
When Precision Stamping Makes Sense
Choose precision stamping when feature position, edge condition, flatness or formed geometry has a direct effect on how the part works.
Tight Feature Position
For holes, profiles and formed details where datum relationships matter.
Functional Edge
For parts where burr direction or smooth sheared edge affects assembly.
Repeat Production
For stable programs where dedicated tooling supports consistent output.
Flatness & Form
For components where distortion or local geometry affects function.
What We Make with Precision Stamping
Real part families produced through our precision stamping programs — each links to the relevant application page.
Shims
Precision shims blanked from spring or carbon steel with controlled profile, flatness and burr direction.
Washers
Flat, precision and special-shape washers with controlled tolerances across materials.
Retainers
Formed retainers and spring seats with consistent depth and feature relationships.
Terminals
Conductive terminals and contacts with controlled material, geometry and surface condition.
Brackets
Stamped brackets with repeatable hole positions for reliable assembly.
Sensor Components
Small functional parts for sensor assemblies where feature location drives performance.
Precision Stamping Process Options
The correct process balances functional requirements, edge quality, tooling investment and production volume.
Progressive Stamping
Progressive stations can combine closely related blanking and forming operations while maintaining strip control.
BEST SUITED FOR- Repeat production with multiple related features
- Stable material specification
Fine Blanking
Fine blanking uses controlled material support and tool conditions to produce a high proportion of smooth sheared edge on suitable parts.
BEST SUITED FOR- Parts requiring a high proportion of smooth sheared edge
- Reducing downstream edge machining where geometry and volume support it
Coining & Calibration
Localized pressure can refine thickness, flatness, radii or functional details, evaluated with material flow, tool load and dimensional measurement in mind.
BEST SUITED FOR- Localized geometry, flatness, thickness or functional detail
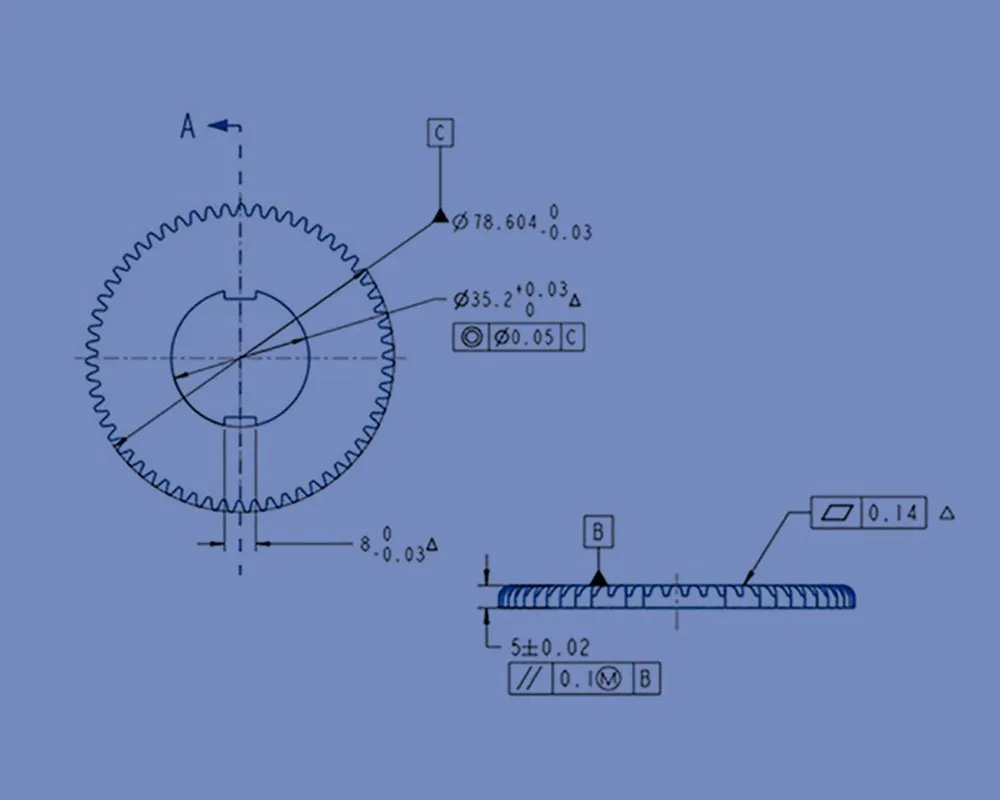
Precision Starts with the Right Datums
Tight drawings do not become capable processes by inspection alone. The tooling, material, datums and measurement plan must support the requirement. Balford has previously described precision work in the IT7 to IT9 range for suitable features — this is not applied as a blanket promise to every dimension. Actual capability depends on material, thickness, feature type, tooling route, datum strategy and measurement method, and is confirmed during project review and sampling.
How We Decide Whether Precision Stamping Is the Right Route
The decision is drawing-specific — feature position, edge condition, consistency, formed detail and part size are weighed together.
| Requirement | Precision Stamping Response | Alternative to Compare | Decision Point |
|---|---|---|---|
| Repeat feature position | Dedicated tooling locates related holes, edges and formed features | CNC machining or fabricated assembly | Volume, datum strategy and accumulated tolerance |
| Functional cut edge | Fine blanking or controlled shearing may improve edge condition | Blanking plus machining or grinding | Required smooth zone, burr limit and material |
| High part consistency | Controlled strip, tool guidance and in-process checks support repeat production | Manual fabrication | Quantity, change frequency and tooling economics |
| Complex formed detail | Coining, embossing or staged forming can integrate the feature | Secondary machining or assembly | Material strain, tool access and inspection |
| Thin or compact component | Precision tooling can combine small related features | Photo etching, laser cutting or machining | Material, edge quality, deformation and production scale |
These are the same factors we review when evaluating a drawing for tooling, inspection and production.
What Drives Precision and Edge Quality
Precision depends on tooling, material, datums and the measurement plan — not inspection alone.
Datum & Tolerance Strategy
Functional datums should represent how the part locates in the assembly. Position, profile, flatness and formed dimensions are reviewed against those datums so gauges and inspection reports describe real part function.
Tool Guidance & Clearance
Punch-to-die relationship affects burr, edge condition, dimensional stability and tool wear. Clearance is selected for the specified material and feature, while die guidance and maintenance protect the relationship during repeat production.
Flatness & Distortion
Cutting force, residual stress, coining, forming and part ejection can influence flatness. Restraining, pressure control, calibration and handling may be evaluated where a flat interface is critical.
Measurement & Capability
Inspection equipment is selected based on the specific feature and tolerance being verified. First-article reports, sample submissions, attribute gauging and in-process checks are all available — for agreed critical dimensions, capability expectations are defined up front.
Materials, Finishes, and Secondary Operations
Precision parts often go through plating, heat treatment or assembly after stamping — those downstream steps are factored into the tolerance stack and surface finish plan from day one.
Carbon & Spring Steels
Common for clips, washers, shims and functional parts. Hardness, heat treatment and coatings can pull flatness or shift dimensions — planned for in tooling and process.
Stainless Steels
Chosen for corrosion resistance and strength. Work hardening, burr formation, tool wear and surface protection all need attention in die design and secondary operations.
Copper & Copper Alloys
Good for conductive or spring applications. Grain direction, plating requirements, cleanliness and handling affect final performance — reviewed before locking the process.
Aluminum Alloys
Used where low mass and corrosion resistance matter. Temper has a direct effect on deformation, burr characteristics and springback — material condition is verified before tooling.
Brass
Formable option for precision stamped parts. Grain direction, surface protection and material cost are handled carefully during quoting and processing.
Plating, Coating & Assembly
Finish thickness, masking, hydrogen embrittlement concerns, press-fit features and mating parts are all reviewed before the production process is released.
Precision Stamped Part Applications
Where precision-stamped components are used across our production programs.
Automotive & Sensor Components
Shims, retainers, washers, housings and functional components that depend on repeatable interfaces and controlled production.
Electrical & Electronic Components
Terminals, shields, conductive parts and compact hardware requiring controlled material, geometry and surface condition.
Industrial Equipment
Locking parts, guides, brackets, wear components and assembly hardware made to specific drawings.
Specialized Components
Selected precision parts where material traceability, inspection rigor, cleanliness and confidentiality are defined by the project.
Precision Stamping Case Studies
Real parts, real materials, real manufacturing requirements — these examples show how drawing requirements become a practical, repeatable production plan.

65Mn Spring Steel Shim

Stainless Steel Nut Washer

Copper Base Plate
What We Review Before Tooling
During quoting, functional dimensions are separated from general tolerances so tooling and inspection costs stay in check without compromising assembly performance.
Functional Dimensions
We separate the dimensions that actually drive function from those that can fall under a general tolerance — keeping tooling and inspection costs in check without compromising assembly performance.
Datum Strategy
Your drawing is reviewed for features that need better datums, burr direction callouts or surface finish specs before tooling is committed.
Downstream Effects
Plating, heat treatment, hole position, radius and material temper changes are reviewed before a new revision — a small tweak can affect tool steel selection, piloting, gauging or assembly seating.
A Controlled Project Workflow
From critical features to repeat production — a defined sequence for every precision stamping program.
Define
Critical features, datum scheme, material, finish, annual volume and function.
Select
Process route weighed across progressive, fine blanking, coining and secondary ops.
Develop
Tooling plan and inspection approach locked for the features that matter.
Verify
Samples measured; edge, surface, fit and corrective actions closed out.
Release
Setup, material, tool maintenance, inspection and revisions controlled.
Precision Stamping Process Envelope
Stated plainly, so you can judge fit before you send a file. Anything outside this envelope is reviewed individually.
| Parameter | What Balford works to |
|---|---|
| Maximum press tonnage | 350 t |
| Maximum deep-drawn diameter | Ø250 mm |
| Tooling | Progressive, transfer and single-operation dies designed and built in our own tool room; only slow-wire EDM is subcontracted |
| Materials | Stainless steel, carbon steel, aluminium, copper, brass, electrical pure iron and selected special alloys |
| Secondary operations | CNC turning and milling, wire EDM, in-die and secondary tapping, deburring and controlled cleaning |
| Outsourced operations | Production heat treatment and surface finishing, carried out by qualified partner plants |
| Inspection equipment | 2.5D optical projector, 3D scanner, roughness tester, Rockwell hardness tester, salt-spray tester, digital height gauge, micrometres and bore micrometres, go/no-go gauges, flash measuring instrument and concentricity gauge |
| Documentation | First article inspection and PPAP Level 3 packages |
Published tolerances depend on material, thickness and feature type — see our stamping tolerance reference and confirm against your drawing.
Precision Metal Stamping FAQ
Answers based on drawing review, because material, geometry and production volume all change what is actually practical.
Our largest press is 350 t, with deep drawing up to Ø250 mm. Tonnage is matched to the part rather than the other way round: strip layout, material yield strength, thickness and the number of stations decide which press a job runs on.
Yes. Level 3 is the submission level most of our automotive and industrial customers ask for, and it is the level we prepare by default. Packages typically include the process flow, control plan, PFMEA, dimensional results, material and performance test results and the part submission warrant. Tell us your customer-specific requirements and we will confirm what we can sign against.
Yes — progressive, transfer and single-operation dies are designed and built in our own tool room. Conventional and CNC lathes, CNC milling, medium and fast wire EDM, tapping, drilling, surface grinding, cold welding and tool maintenance are all in-house; only slow-wire EDM is subcontracted.
Precision stamping puts much more emphasis on tool guidance, datum relationships, edge condition, flatness and measuring the features that affect function. Depending on the drawing and volume, we might use progressive tooling, fine blanking, coining or calibration.
We can hit IT7 to IT9 on suitable precision-stamped features, but it is not a blanket tolerance for every part. Material, geometry, feature type, distance from datums, tooling and measurement method all come into play. Capability is drawing-specific — we confirm what is achievable for your drawing during quoting and sampling.
Fine blanking makes sense when you need a high percentage of smooth sheared edge, better flatness, or a functional edge that would otherwise require machining. Geometry, material, thickness, volume and tooling cost all factor into whether it is the right route.
Yes, those operations can be coordinated when specified. Their effects on hardness, distortion, coating thickness, surface condition and hydrogen embrittlement risk are accounted for in both the process and inspection plan.
Burr direction is set by the punch and die orientation and marked on the drawing where it affects assembly, sealing, safety or appearance. The desired direction is reviewed against strip layout, part ejection and any downstream operations.
Send a controlled 2D drawing, a 3D model if available, material and temper, finish, annual and batch quantities, critical dimensions, edge or flatness requirements, inspection documentation and the assembly context.
Have a Drawing Ready?
Send your latest revision, material specification, quantity, finish and functional requirements. We will review the production route and identify any technical questions before quoting. We can sign an NDA before you share detailed project files.
Related Capabilities & Resources
Precision stamping connects to the full stamping cluster, materials, applications and case studies.
Precision Stamping Technical Articles
Fine Blanking Operations in Precision Stamping
How fine blanking improves edge condition for functional parts.
Standard Tolerances for Stamped Parts
What general tolerances apply and when drawing-specific control is needed.
Precision Stamped Parts: The Key Points
Key considerations for precision stamped components.
Related: ironing in deep drawing — how a thinned wall holds both the inside and the outside diameter · ironing instead of turning · ironing for solenoid valve housings (DT4E, DC04) · ironing tolerances and surface finish
Precision dies for tight-tolerance parts are made by Balford’s in-house tool room rather than a third-party die shop.
Press tonnage, maximum draw diameter and the full machine list are published on the equipment list page.
Capacity at a glance: press capacity up to 350 t · maximum deep draw diameter Ø250 mm · full machinery and inspection list.
Parts that are still being developed usually start on single-operation tooling — see prototyping and short-run stamping.
Where the precision requirement comes from a housing rather than a flat part, see solenoid valve housings and sensor housings.