Balford Tool Room · Zhuji, Zhejiang, China
Every die built here runs inside one of our stamping services; the commercial overview of that route is on the custom metal stamping services page.
In-House Tooling Design & Build
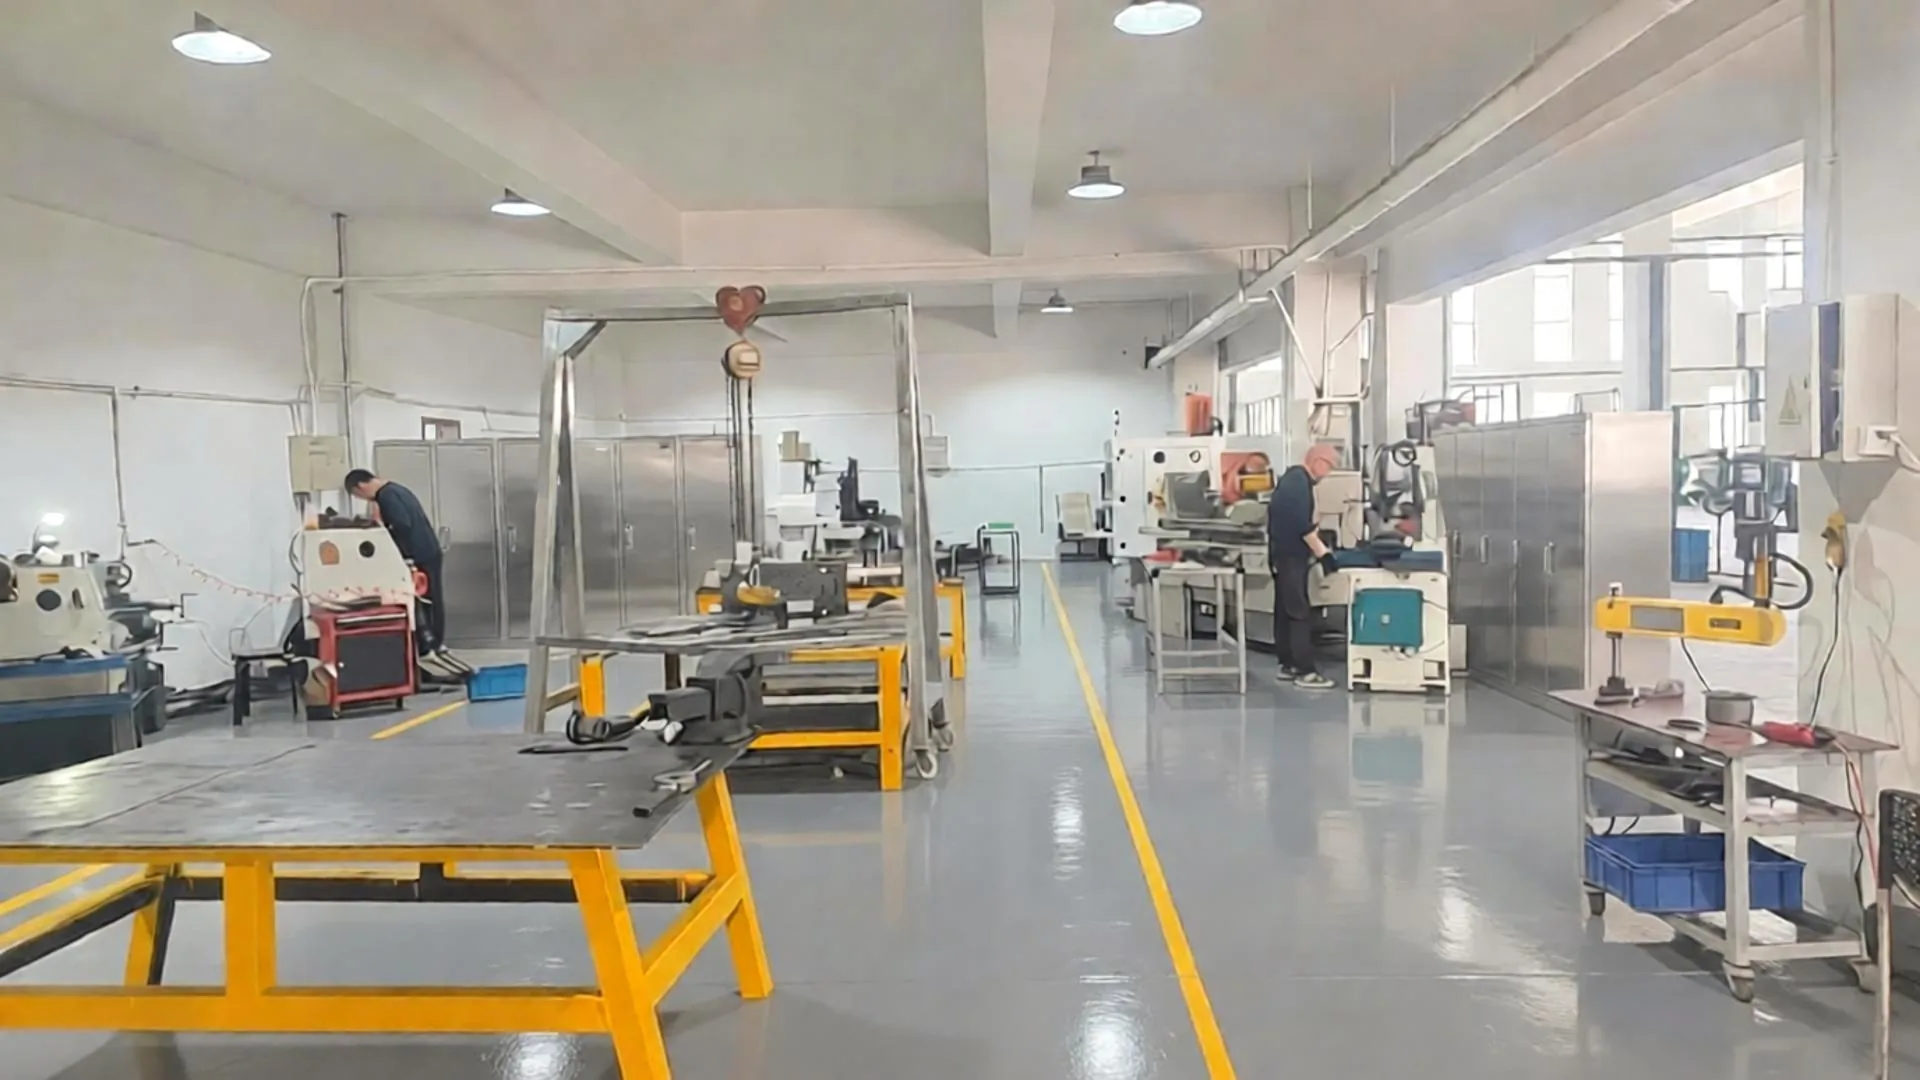
Balford designs and builds progressive, transfer and deep-draw stamping dies inside its own plant. From DFM review and tool steel selection through machining, wire EDM, assembly, tryout and PPAP samples, one in-house team owns the die. Only slow-wire EDM is outsourced — every other tool room operation is completed in-house.
What does in-house tooling design & build mean at Balford?
Buyers often source stamped parts from one factory and dies from another. Balford closes that gap: the same site that runs your production presses also designs, builds and maintains the tooling.
Which dies does Balford design and build?
Progressive dies
Multi-station strip dies for high-volume stamped parts: blanking, forming, drawing, piercing and tapping in one pass.
Progressive die stamping services →Deep-draw dies
Single and multi-stage draw tooling for cylindrical shells, housings, cans, sleeves and sensor enclosures in steel, stainless, aluminium and pure iron.
Deep draw metal stamping services →Transfer & form dies
Dies for larger or asymmetric parts where the blank is transferred between stations for drawing, restriking, trimming and flanging.
Custom metal stamping →Compound, blanking & bending tools
Single-operation tools for washers, caps, brackets and sheet metal parts, plus bending and forming dies used across production.
Sheet metal processing →What tooling equipment is inside Balford’s tool room?
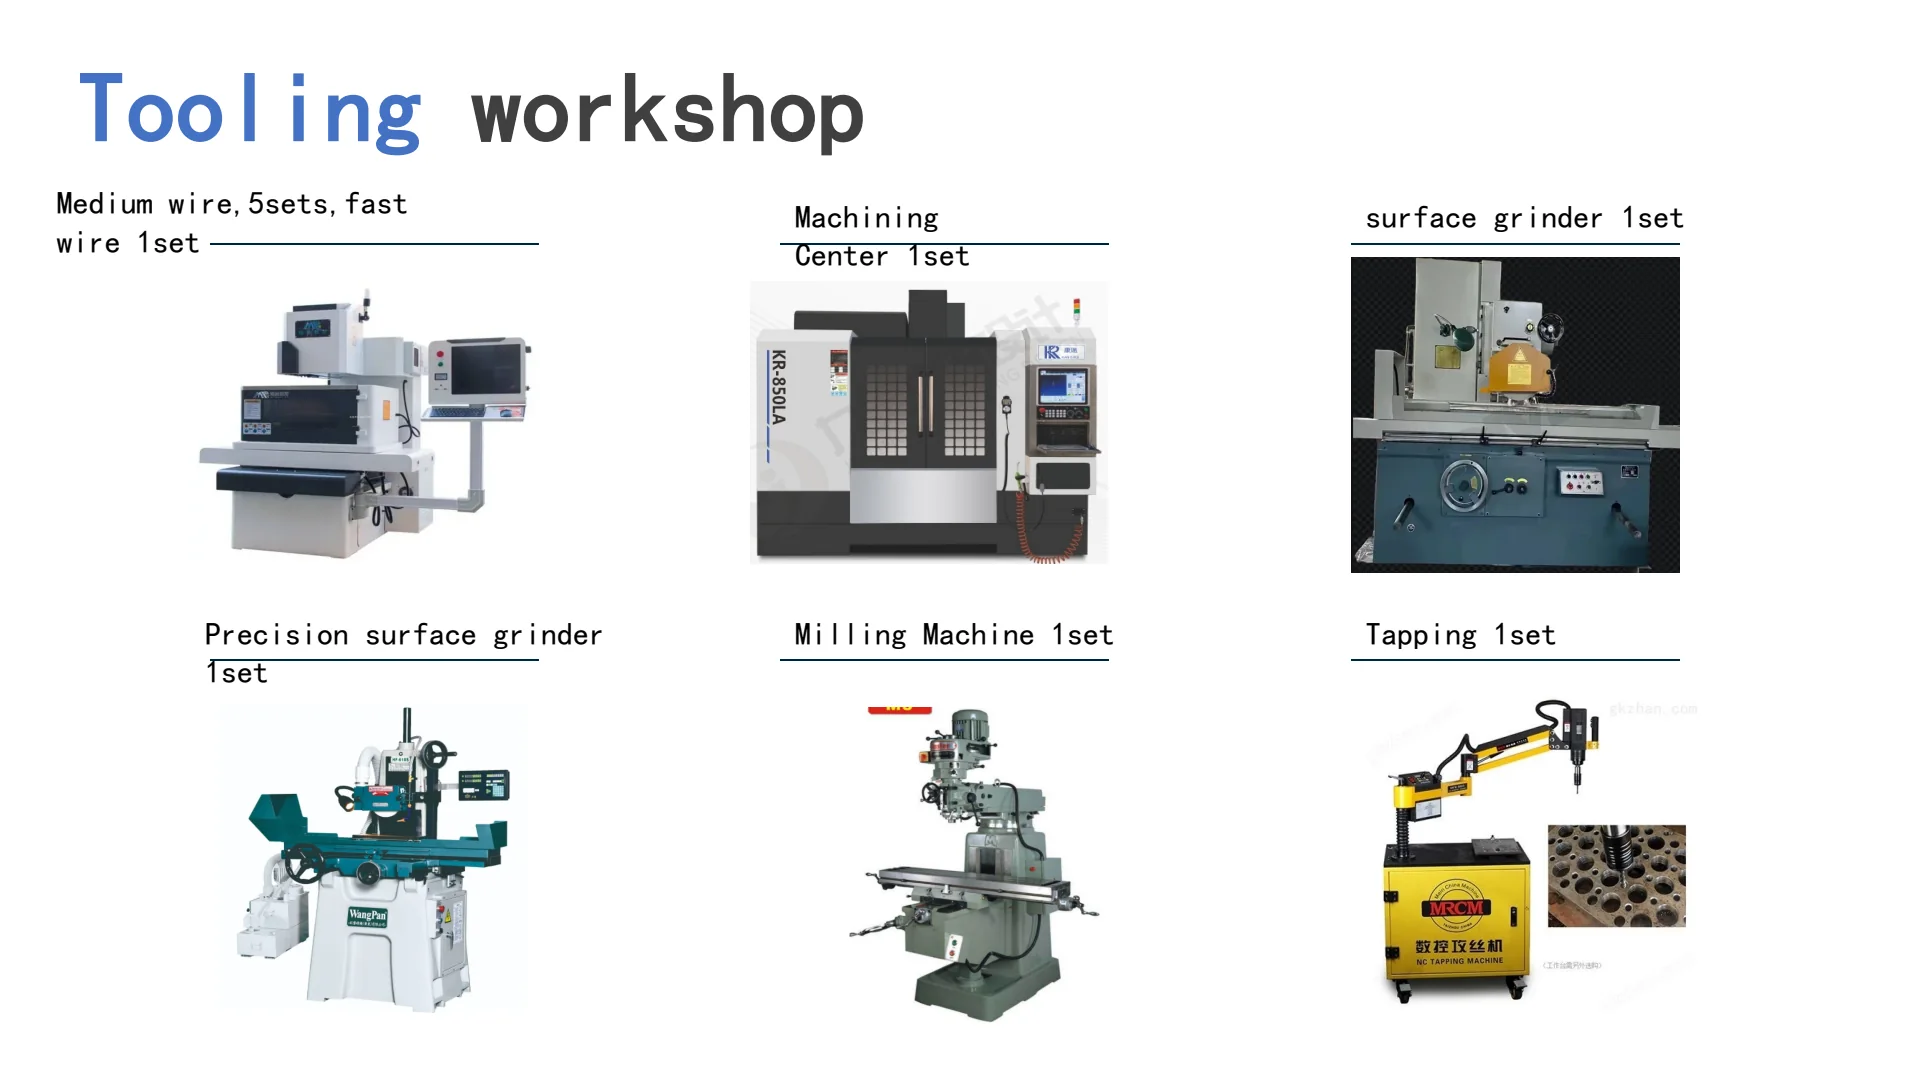
The tool room is equipped as a complete die shop. The table below is the machine list visitors see on the Balford workshop floor.
| Equipment | Role in die making | In-house status |
|---|---|---|
| Internal & external cylindrical grinders | Grinding round die components, punches, pilots, core pins and bushings to final size and finish. | In-house |
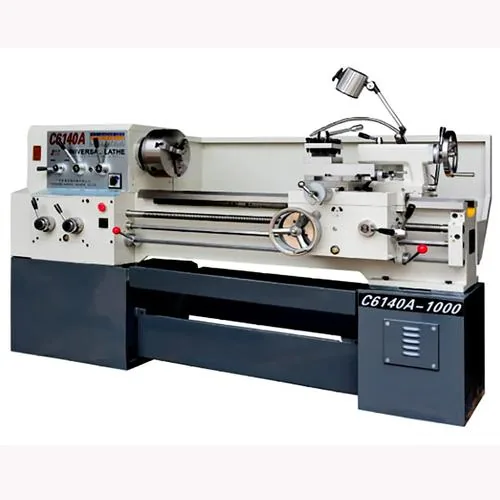
| Engine lathes ×3 | Turning punch blanks, ejector pins, guide posts and general tool room components. | In-house · 3 units |
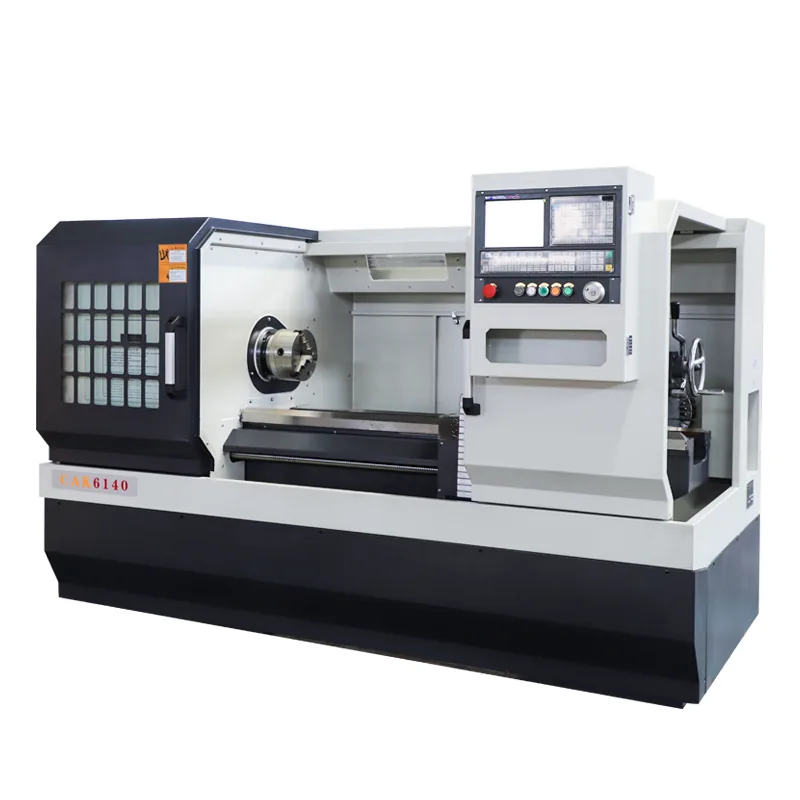
| CNC lathe ×1 | Precision turned components with repeatable geometry for die and mould assemblies. | In-house · 1 unit |
| CNC milling machines | Machining die plates, pockets, cavities and mounting features in hardened and pre-hardened steels. | In-house |
| Precision surface grinder | Flat grinding of die plates, strippers and inserts with tight parallelism and surface finish. | In-house |
| Large surface grinder | Grinding large die plates and big tool bodies that do not fit standard machines. | In-house |
| Drilling machines | Drilling dowel, screw and water-line holes across die sets and fixtures. | In-house |
| Medium-speed wire EDM ×5 | Cutting die openings, punch profiles and contoured sections with stable accuracy. | In-house · 5 units |
| Fast-speed wire EDM ×1 | High-speed roughing and vent/slot cutting where finish demand is lower. | In-house · 1 unit |
| EDM hole drilling (perforator) | Drilling start holes for wire EDM and small, deep precision holes in dies. | In-house |
| Slow-wire EDM | Ultra-fine finish and taper-critical wire cutting for special die details. | Outsourced partner |
| Automatic tapping machines | Threading die plates, strippers and parts with consistent pitch and depth. | In-house |
| Die cold welder | Cold-weld repair of die wear, chips and scratches without heat distortion. | In-house |
| Argon arc (TIG) welder | Building up worn edges and repairing tool steel components with controlled heat input. | In-house |
| Pneumatic die grinders | Bench and hand finishing of radii, fillets and draw surfaces. | In-house |
| Demagnetizer | Removing residual magnetism after grinding and EDM so swarf never sticks to die surfaces. | In-house |
| Heat treatment equipment | A small furnace is kept for emergency die repairs; bulk hardening and tempering of die components is carried out by audited heat-treatment partners, with hardness data returned to us. | In-house |
Tooling-related machining, grinding, EDM, welding and maintenance are carried out in-house. Two steps are subcontracted: slow-wire EDM for very fine finish or deep-taper details, and bulk heat treatment of die components — a small furnace is kept in-house for emergency repairs.
Why does in-house tooling matter for your project?
For stamped and deep-drawn parts, the die is where quality, cost and lead time are decided. Keeping tooling in-house changes how those three factors behave.
Faster DFM-to-tooling loop
Tooling engineers receive your drawing, flag draw ratio or formability issues, and adjust the die design in the same building — no design-to-outsider handoff.
Tryout on our own presses
Dies are fitted, adjusted and run on Balford production presses before release, so sample parts reflect actual serial conditions.
One accountable partner
Tooling price, timing, samples and PPAP documentation come from one supplier, with a single engineering contact from RFQ to production.
Tool life & maintenance
We keep die records and spare inserts, and repair wear in-house during the life of the program instead of shipping the die out.
Automotive-grade documentation
In-house inspection and FAI/PPAP-aligned documentation support part approval — learn more on the PPAP capability page.
IP stays protected
Customer-owned die designs are not shared across a supply chain; NDAs and protected tooling records are standard.
From drawing to production die: the in-house workflow
Inside the tool room
The dies that form these parts are designed and built metres away from the presses.
Tooling design & build — buyer questions answered
Do you design stamping dies in-house from my part drawing?
Yes. Balford’s tooling engineers run DFM on your 2D/3D drawing, define the strip or draw sequence, and design the die before any steel is cut. You receive design feedback on material, draw ratio, tolerances and cost drivers before tooling starts.
Which types of dies do you build?
Balford builds progressive dies, single and multi-stage deep-draw dies, transfer and form dies, plus compound, blanking and bending tools. They support solenoid valve housings, sensor housings, motor parts, sleeves, caps, cans and structural stampings.
What tool room machines do you have?
The tool room has internal and external cylindrical grinders, three engine lathes, one CNC lathe, CNC milling machines, precision and large surface grinders, drilling machines, five medium-wire EDM sets, one fast-wire EDM set, EDM hole drilling, automatic tapping, die cold welding, TIG welding, pneumatic grinders, a demagnetizer and a small heat-treatment furnace for emergency die repairs.
Which tool steels do you normally use for stamping dies?
Common choices include D2, Cr12MoV and similar cold-work die steels for stamping and blanking components, with wear inserts and punches selected by volume, material thickness and part finish. The design review recommends steel grade per station before machining starts.
Do you outsource any tooling work?
Only slow-wire EDM is outsourced, and only when a die detail needs ultra-fine finish or deep-taper cutting beyond the capability of our medium and fast wire machines. Design, machining, grinding, assembly, tryout and maintenance are all done in-house, with bulk heat treatment outsourced to an audited partner.
What is a typical tooling lead time?
For common single-operation or deep-draw tooling programs, in-house design and build typically runs 15–30 days; progressive and transfer dies take 30–60 days depending on station count and tryout iterations. Tooling repair and insert replacement are faster.
Can you run die tryouts and PPAP samples at your plant?
Yes. Dies are tried out on Balford production presses, first articles are inspected in-house, and PPAP-aligned documentation can be prepared for automotive programs, supported by the quality system and IMDS data process.
Do you maintain customer-owned tooling during serial production?
Yes. Customer-owned dies are stored, maintained and repaired in-house, with records of running hours, wear and spare inserts so the tool stays stable for the life of the program.
Get a DFM review before tooling starts
Send your drawing and target volume — Balford’s tooling and sales engineers normally respond within 24 hours with a forming feasibility review and a production quote.
Related die engineering resources
- Top-tier stamping die design: 13 checkpoints — what a die package should contain, from strip layout to tryout.
- Stamping die design engineering service — how Balford reviews and engineers a die before any steel is cut.
- Deep drawing capability — draw stages, wall control and the process envelope.
- DFM review — the manufacturability check that happens before tooling.
Transfer tooling is built here too — see the dedicated transfer press stamping page. Machine-by-machine detail, including the wire EDM units and grinding capacity, is listed on the equipment list.
Outsourced heat treatment and finishing are controlled under the same system — see metal finishing and secondary operations.
How the tool is validated before serial production: prototyping & first article inspection.
The same tool room builds the single-operation dies used for prototypes and short runs — see low volume stamping and prototyping.