Summary
At Balford, we believe transparency is the foundation of a successful partnership. To help you evaluate if we are the right fit for your project, we clearly define what we do not and cannot do. This guide outlines our capability boundaries in terms of part size, speed, tolerance, and cosmetic requirements, allowing you to assess fit quickly and accurately.do not and 1. We Do Not Run Micro-Stamping do. This guide outlines our capability boundaries in terms of part size, speed, tolerance, and cosmetic requirements, allowing you to assess fit quickly and accurately.
We do not accept projects where the blank size for deep drawing is less than 3mm or the final outer diameter is under 0.3mm.1. We Do Not Run Micro-Stamping
We do not accept projects where the blank size for deep drawing is less than 3mm or the final outer diameter is under 0.3mm.
Micro-stamping and micro-deep drawing demand specialized machines, ultra-precision tooling, and dedicated cleanroom conditions. These parts—common in medical implants or micro-connectors—operate at a scale where material behavior shifts significantly.Our equipment and expertise are geared toward larger, robust industrial components.
If your part measures under a few millimeters, we're not the right fit and will point you to a specialist.
2. We Don't Run Oversized Stamping

We can't process parts where the blank exceeds 600mm or the finished draw height goes past 200mm.600mm or the finished drawn height exceeds Our press line isn't set up for that scale. Oversized stamping typically requires massive, specialized presses (e.g., 800+ tons) and dedicated handling systems. Our equipment is built for high-precision, medium-sized components, which matches the automotive and industrial sectors we serve..
For parts beyond those dimensions, you'd need to work with a heavy-gauge stamping house.Our press line is not configured for parts of this scale. Oversized stamping often requires massive, specialized presses (e.g., 800+ tons) and handling systems . Our equipment is designed for high-precision, medium-sized components, which aligns with the needs of the automotive and industrial sectors we serve.
3. We Don't Do High-Speed StampingFor parts beyond this dimension, you would need to consult a heavy-gauge stamping house.
We run medium to low-speed stamping, with a max operating speed of 120 strokes per minute (SPM). We do not do high-speed stamping.
3. We Do Not Do High-Speed Stamping
High-speed stamping—often exceeding 200, 800, or even 2000 SPM—is a different manufacturing discipline. It requires specialized press designs, ultra-hard tooling (e.g., carbide), sophisticated feeding systems, and advanced vibration management to run reliably at those speeds.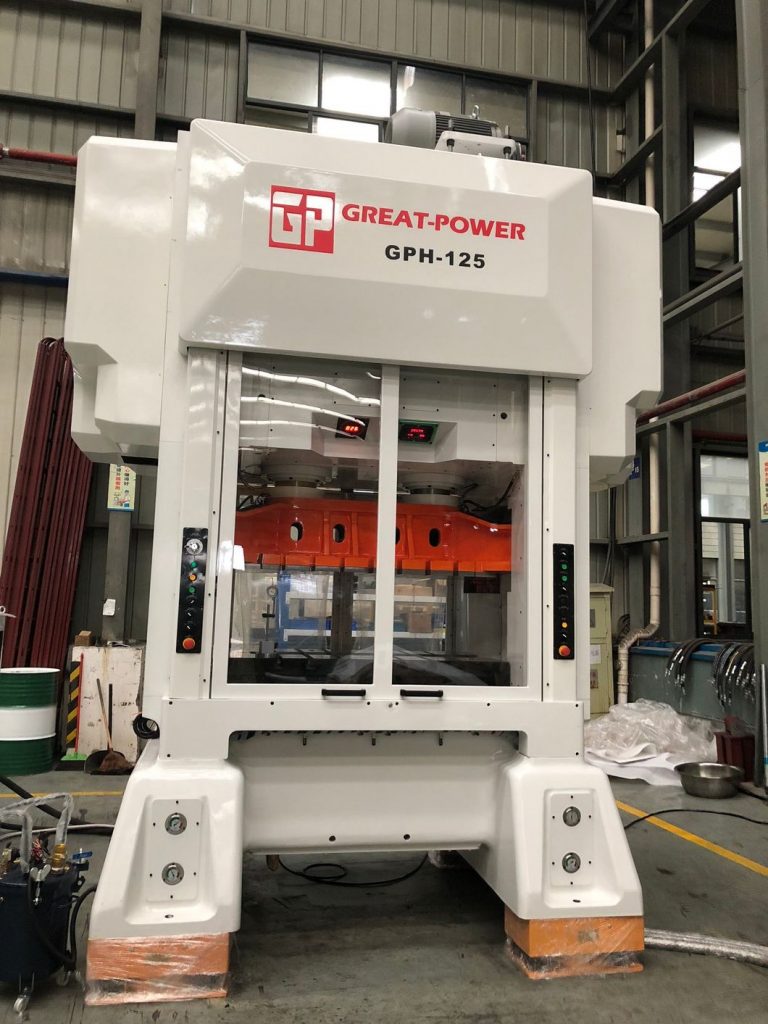
Our focus is on process stability and precision, not throughput. Medium-speed operation lets us maintain tighter control over material flow, reduce tool wear, and perform more rigorous in-process inspections—critical for the complex deep draws we specialize in.medium to low-speed stamping, with a maximum operating speed of 4. We Don't Do "Cosmetic-Grade" Finishes. We do not do high-speed stamping.
High-speed stamping, often exceeding 200, 800, or even 2000 SPM, is a distinct manufacturing discipline . It requires specialized press designs, ultra-hard tooling (e.g., carbide), sophisticated feeding systems, and advanced vibration management to function reliably at those speeds .
Our focus is on process stability and precision, not throughput. Medium-speed operation allows us to maintain tighter control over material flow, reduce tool wear, and perform more rigorous in-process inspections—critical for the complex deep draws we specialize in.
4. We Do Not Do “Cosmetic-Grade” Finishes
We donotproduce parts to a cosmetic-grade or artwork standard where the surface must be flawless and visually perfect.
Our manufacturing expertise is infunctionalcomponents, where dimensional accuracy, sealing performance, and mechanical properties are paramount. While our deep drawn surfaces are typically smooth and clean, they are not intended for applications where microscopic surface imperfections are unacceptable (e.g., visible exterior trim on luxury goods). Achieving that level of finish requires dedicated post-processing like electropolishing or hand-finishing in controlled environments, which is outside our standard process scope..
5. We Do Not Do Micron-Level Tolerances
5. We Do Not Do Micron-Level Tolerances
We donotaccept projects requiringmicron-leveldimensional or geometric tolerances (e.g., < ±0.01mm) as a standard capability. dimensional or geometric tolerances (e.g., < ±0.01mm) as a standard capability.
Precision stamping at that scale, often near ±0.001mm or ±0.0001 inches, requires a level of machine precision, environmental control (temperature and humidity), and measurement capability that is not part of our standard offering. Our standard precision tolerance is within ±0.05mm to ±0.25mm for deep drawn parts, which is industry-standard for robust engineering components.Precision stamping at that scale, often near ±0.001mm or ±0.0001 inches If your design requires extreme precision, we will be upfront about the need for a secondary, specialized operation like ironing, which is outside our core service..
Why We Define Our Boundaries
By clearly stating what we don’t do, we ensure we only take on projects where we can excel and deliver value. This focus allows us to:
Why We Define Our Boundaries
Maintain High Quality:We avoid the risk of failure on applications not suited to our equipment.
- Be Transparent:
- You can trust our quotes and lead times because they are based on realistic capabilities. We avoid the risk of failure on applications not suited to our equipment. Focus
- on Our Strengths:We dedicate our engineering and production resources to complex, mid-sized deep drawn and precision stamped parts where we have deep expertise.
- Focus on Our Strengths: We dedicate our engineering and production resources to complex, mid-sized deep drawn and precision stamped parts where we have deep expertise.
FAQ: Capability Questions
Q: What is the minimum wall thickness you can achieve?
A: That depends on the material grade and part geometry. As a rule of thumb, our process is set up for materials with good drawability—think low-carbon steel or aluminum. We typically run starting blank thicknesses from 0.5mm up to 3.0mm. If you're looking at thinner stock below 0.5mm, especially for complex deep draws, we're probably not the best fit—you'd be better off with a shop that specializes in micro-forming.
Q: What is your typical tolerance for a deep drawn part?
A: Our standard capability holds dimensional tolerances within a range of ±0.05mm to ±0.25mm on critical features, which aligns with common industry practice for deep drawing . That's tight enough for functional parts in automotive and industrial applications. If you need something tighter, we'll evaluate it on a case-by-case basis, but don't expect that as our default—it's not something we quote as standard.
Q: Can you produce a part with a very smooth, decorative surface?
A: We deliver parts with an as-drawn surface finish—clean, generally free of major defects, but you may see light tool marks from the draw process. If your application demands a flawless cosmetic surface, like for visible trim or consumer-facing components, we'd recommend sending that work to a shop that specializes in post-processing—electropolishing or fine polishing—because that's outside our core capability.