Prototyping · Short runs · Single-operation tooling
Low Volume Stamping and Prototyping
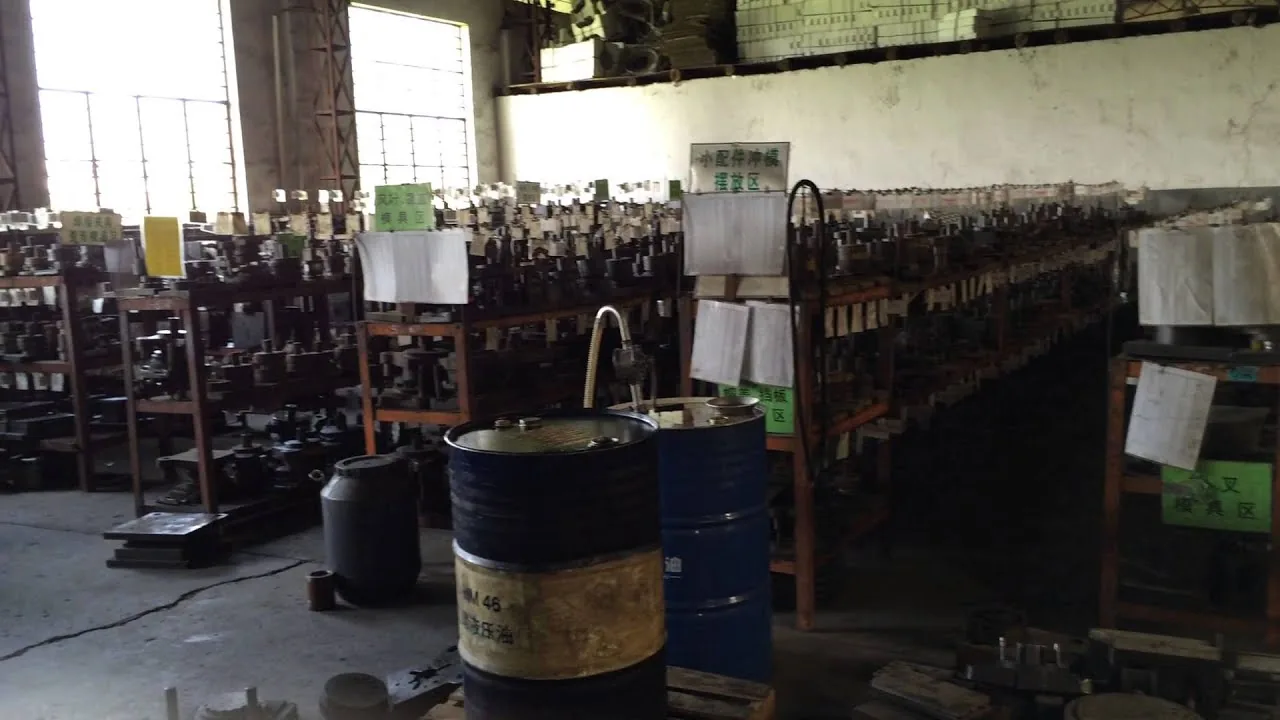
Balford holds more than 4,000 single-operation draw dies, accumulated since the first was cut in February 2000. That library is why a new cylindrical housing usually needs new tooling only where its geometry genuinely differs. From a handful of parts to a few thousand, without buying a progressive die before the volume justifies one.
What is low volume stamping?
Low volume stamping produces a small quantity of formed metal parts — from a single prototype up to a few thousand pieces — on single-operation tooling rather than on a progressive or transfer die. It exists because a multi-station die only pays for itself at volume: the die cost is spread across the parts it produces. Below that crossover, one forming station at a time is faster to build, cheaper to modify and far easier to iterate. In practice the decision is not about quality — the same presses and the same drawing engineering are used — it is about which tooling route stops you paying for volume you do not have yet.
Why single-operation tooling wins below about 10,000 pieces
A progressive die is not one tool. It is a strip layout, a carrier web, pilots, a station sequence and every forming operation cut at once. That is exactly what makes it fast and cheap per part at high volume, and exactly what makes it slow and expensive to change.
A single-operation tool is one forming station. For prototype and short-run work that difference decides three things:
Change is cheap
A revision means re-cutting a punch or re-grinding a die ring — not re-timing a strip, re-cutting stations and re-proving the whole tool. Iteration stays in days instead of weeks.
You change the part, not the layout
A prototype exists to find problems. Single-operation tooling lets the part move between iterations; a progressive die locks the geometry the moment the strip is committed.
Tooling cost starts low
You buy one forming station to answer the question “does this part form?” instead of buying an entire production tool to answer it.
| Tooling route | Typical fit | Cost to change | Volume band where it wins |
|---|---|---|---|
| Single-operation / single-hit | Prototypes, pilot batches, small series, and any part still being developed | Lowest — one punch or one die ring | Under roughly 10,000 pcs |
| Transfer press | Multi-stage forming where the part is carried between stations | Medium to high | Roughly 20,000–500,000 pcs |
| Progressive die | High-volume strip-fed parts with several operations combined | Highest — the strip layout is the tool | Above roughly 50,000 pcs |
The break-even is not a fixed number. It moves with geometry, material, wall thickness and how many forming stages the part needs. We calculate the route from your drawing rather than applying a table.
The die library: two decades of single-hit drawing dies
The first of those dies was cut in February 2000, when the family stamping shop opened in Tangxia Town, Rui’an — the automotive parts cluster in Zhejiang where Balford’s manufacturing history starts. Since then the plant has built single-operation drawing dies for motor housings, solenoid valve housings, sensor housings, cups, caps, bushings and shells, and kept them.
More than 4,000 single-operation draw dies are still held, maintained and re-used. Punches, die rings, blank holders and knock-outs accumulated across two decades of that work sit in the same tool room as the progressive and transfer tooling built after 2020.
This is the practical advantage. Those dies were built to common shank and die-set interfaces, so existing punches and die rings can often be re-combined into a new cylindrical profile. A new part then needs new tooling only where its geometry genuinely differs — a different radius, a different step, a different wall thickness — instead of a complete die set cut from scratch.
What that does to a prototype project:
- The schedule goes into drawing trials, not into die cutting. Where the geometry sits inside the existing library, the first trials can start from tooling that already exists.
- Risk moves earlier. You see wrinkles, tears, thinning and earing on real parts instead of in a discussion.
- The part can change. Because a single-operation tool is adjustable, a design revision does not invalidate the tooling investment.
Where this does not apply. The library is built around round, rotationally symmetric geometry. Heavily stepped, non-circular or asymmetric parts normally need new tooling, and we will say so before quoting. The reason it is still worth having is that most solenoid valve housings, sensor housings, bushings and caps are cylindrical — which is exactly where the library pays.
Prototype on single operation, correct it in the progressive die
This is how Balford runs a new programme, and it is the part of low volume work that pays off later.
- Drawing review and DFM. Material, thickness, critical tolerances, wall requirements and annual volume are read against the forming sequence. Draw ratio and the number of stages are established before anything is cut.
- Single-operation prototype tool. One forming station at a time, built to be adjusted. This is deliberately not the production tool.
- Trial parts, measured. The failure mode shows up on real parts: wrinkling from blank-holder force, tearing at the die radius, wall thinning above the radius, earing at the trimmed edge, springback on the diameter.
- Correct the parameter that caused it. Die radius, clearance, blank-holder pressure, blank diameter, lubrication, or an added redraw or inter-stage anneal.
- Only then design the progressive or transfer die — with the corrected sequence built in.
The commercial reason for that order is straightforward. On a progressive die, discovering the same problem after the tool is cut means re-cutting stations, re-timing the strip and re-proving the tool — measured in die steel and in weeks of lost production. Finding it on a single-operation tool costs a punch regrind or a new die ring.
That loop is also why the progressive and transfer tooling we have built since 2020 starts from known-good drawing parameters rather than assumptions: the problems were already found, on the cheaper tool, at the prototype stage.
See a drawn housing come off the press
Filmed at Balford: a mild-steel solenoid valve housing being deep drawn. Prototype and short-run parts like this are formed one stage at a time on the single-operation presses — the normal entry point for a housing that later moves to transfer or progressive production.
What we make this way
Solenoid valve housings
Deep drawn housings in DC04 and pure iron where magnetic performance matters, including the wall-thinning route when both the inside and outside diameter are functional.
Sensor housings
Stainless steel sensor housings and shells where corrosion resistance, wall consistency and clean seating faces drive the design. See the sensor housing page.
Bushings, sleeves and tubes
Round, thin-wall parts where concentricity and surface finish matter more than complexity.
Cups, caps and shells
Formed closures and drawn shells with trimmed edges and pierced or tapped features added as secondary operations.
Motor housings and end caps
The part family this plant started on in 2000, still produced for appliance, automotive and industrial programmes.
Second-operation work
Trimming, piercing, tapping, facing, deburring and annealing added to a drawn part after forming, rather than built into a strip.
Prototype in the material you will produce in
A prototype only tells the truth if it is made from the production grade. Balford draws prototypes in the same materials the production parts use — which matters most where the material carries the function rather than just the shape:
| Material | Typical prototype and short-run use |
|---|---|
| DC04 / low-carbon deep drawing steel | Solenoid valve housings, drawn shells and general cylindrical parts where drawability matters more than strength |
| Pure iron (DT4 / DT4C) | Soft-magnetic housings, sleeves and pole parts where permeability and coercivity are functional requirements |
| Stainless steel (304 / 316) | Sensor housings and parts exposed to moisture, coolant or chemicals; work-hardens fast, so the number of draws and any inter-stage anneal are decided early |
| Brass and copper | Electrical and thermal parts, terminals and fittings; highly formable, and a good choice when a prototype has to be soldered or brazed |
| Aluminium | Lightweight housings and enclosures; drawability varies widely by alloy, which is why the grade is confirmed before tooling |
Prototyping a solenoid housing in DC04 or pure iron rather than in a convenient substitute also means the magnetic results you measure are the results you will get in series production — the anneal and the magnetic properties carry across, because the material and the forming route did.
What low volume stamping does not do
It will not be the cheapest unit price
Single-operation work means more handling and more separate operations by definition. If your annual volume is already high and stable, a progressive or transfer die will beat it on unit cost — and we will tell you that, even though the tooling quote is larger.
It does not suit every geometry
The single-hit die library covers cylindrical profiles. Non-circular, asymmetric or heavily stepped parts normally need dedicated tooling.
Some steps are always outsourced
Slow-wire EDM and all heat treatment of production parts run through audited partners, with certificates returned to us. Everything else — tooling design and build, conventional and fast wire EDM, drawing, secondary operations and inspection — runs in-house.
It is not a substitute for a real DFM review
A prototype tool answers forming questions, not commercial ones. Wall thickness callouts, tolerance positions and which diameter is functional still have to be settled on the drawing.
Frequently asked questions
Balford quotes prototype and short-run deep drawing rather than requiring a production volume, so the question is not a minimum order quantity but which tooling route fits. If the geometry sits inside the existing single-operation die library, the first parts can be produced from tooling that already exists. If it needs new tooling, that is a tooling question rather than a quantity question, and we quote accordingly.
Yes, when the part is a known geometry or a repeat of something already in production. Where the draw ratio is aggressive, the wall callout is tight or the number of forming stages is uncertain, prototyping on single-operation tooling first is normally cheaper overall — the cost of a wrong strip layout is paid in die steel and in weeks, not in one punch.
Yes, and we recommend it. DC04, pure iron (DT4 / DT4C), stainless steel, brass, copper and aluminium are all drawn here. Producing a prototype in the production grade matters most for soft-magnetic housings, because the material and the forming route are what determine permeability and coercivity — a substitute material would make the measurements meaningless.
Presses run from 25 t to 350 t and the maximum deep draw diameter we quote is Ø250 mm. Whether a specific part fits depends on material grade, sheet thickness, depth-to-diameter ratio, wall requirement and how many draw stages the geometry allows. We confirm the sequence against your drawing before quoting, and the full machine list is published on the equipment list.
It depends on two things: whether the geometry is covered by the existing single-operation die library, and how many forming stages the part needs. A part that re-uses existing punches and die rings goes into drawing trials much sooner than one that needs a complete new die set. We confirm the schedule together with the DFM response, so you have a date before committing to tooling.
Enough to establish the forming sequence: drawing or 3D model, material grade, sheet thickness, the critical tolerances and which diameter is functional, expected quantity and whether the part is expected to move into series production later. Sending the drawing for a DFM review is the fastest way to get a route and a tooling concept rather than a number.
Yes. Prototype and first-article parts are inspected in-house with the same metrology used for production — 2.5D optical projector, micrometers and bore gauges, roughness tester, concentricity instruments, go / no-go gauges and hardness testing — and PPAP Level 3 documentation can be provided for new programmes.
Related pages: Deep draw metal stamping · Deep drawing: the complete technical guide · Progressive die stamping · Transfer press stamping · In-house tooling design & build · Equipment list · How to make deep drawn parts · How stamping parts are priced · Solenoid valve housings · PPAP
Send the drawing — we will tell you which tooling route fits
Include material grade, sheet thickness, quantity and the tolerance that actually matters. We will come back with the forming sequence, whether existing single-operation tooling covers the geometry, and what a prototype or short run would take.
Send your drawing for a DFM review