A stamped or deep-drawn part either assembles or it does not, and the difference is usually two or three dimensions. Balford's inspection lab exists to find those dimensions before the parts ship — and to produce the measured evidence that a PPAP submission, a first article inspection report or a customer complaint investigation is built on.
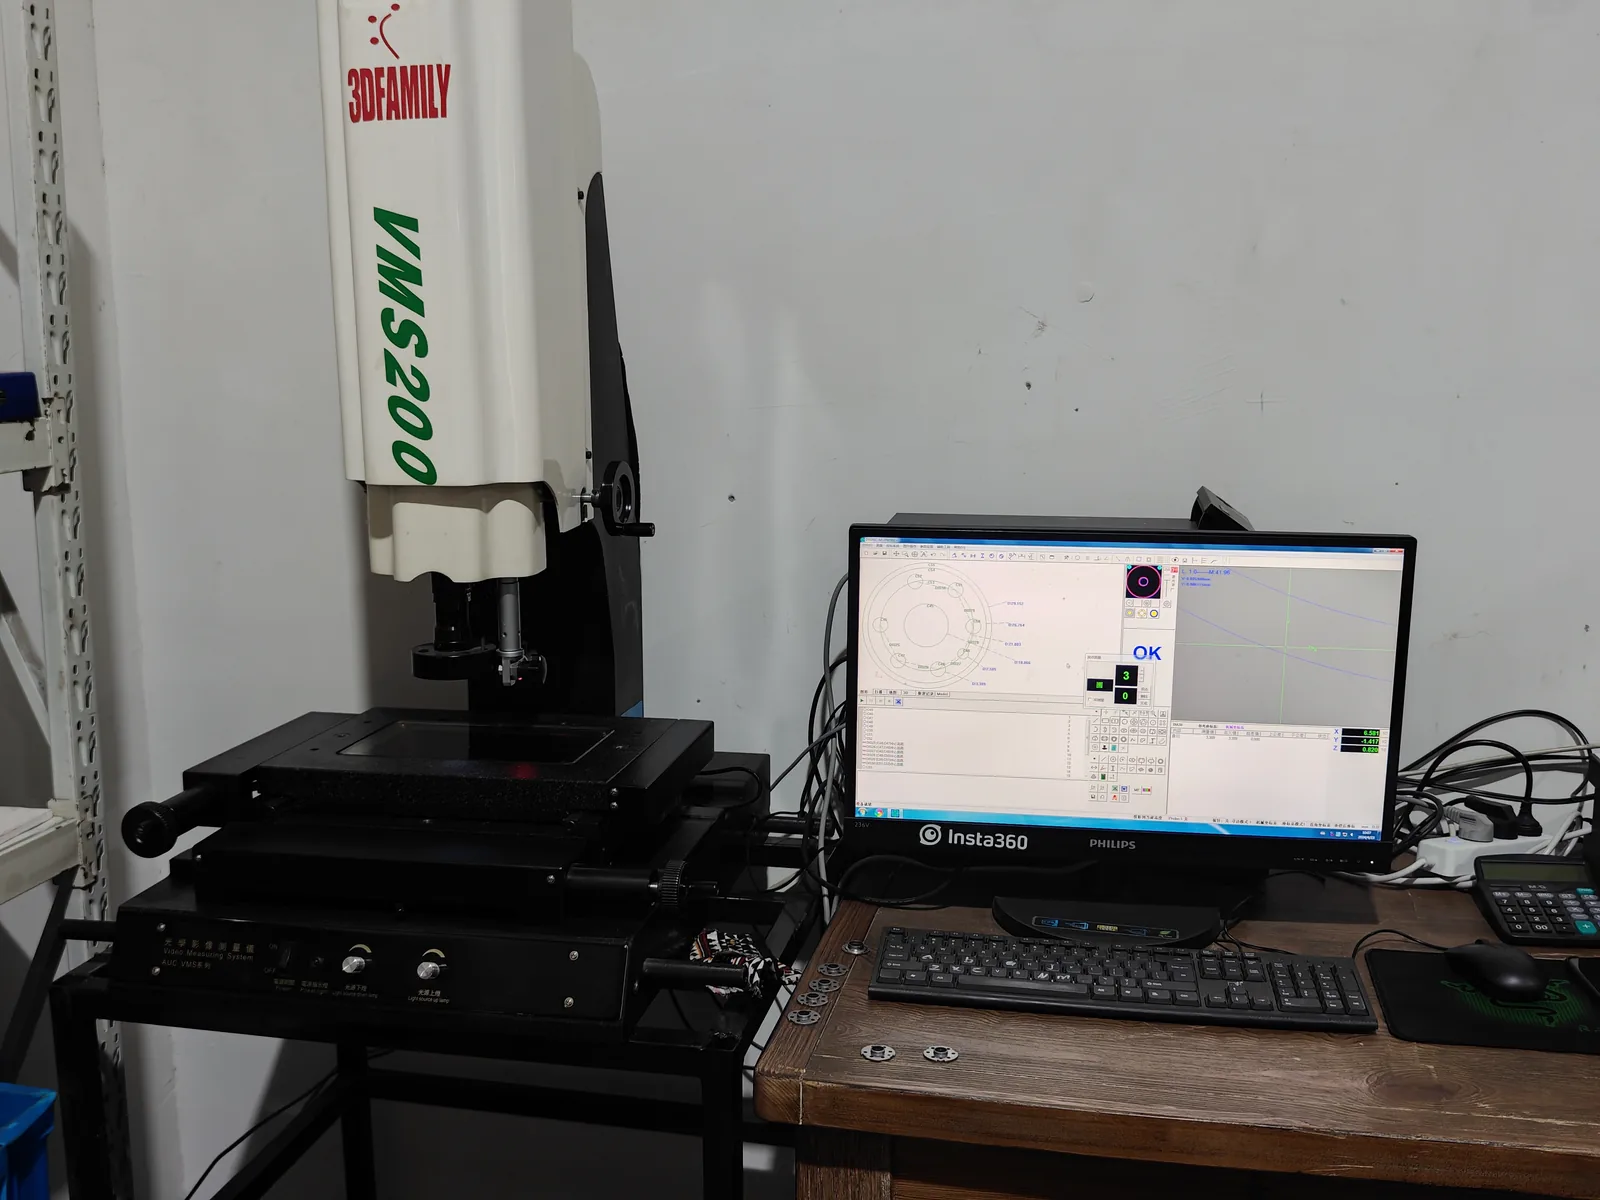
What the lab can measure
- Dimensional — outside and inside diameters, wall thickness, heights, depths, step positions, flange geometry.
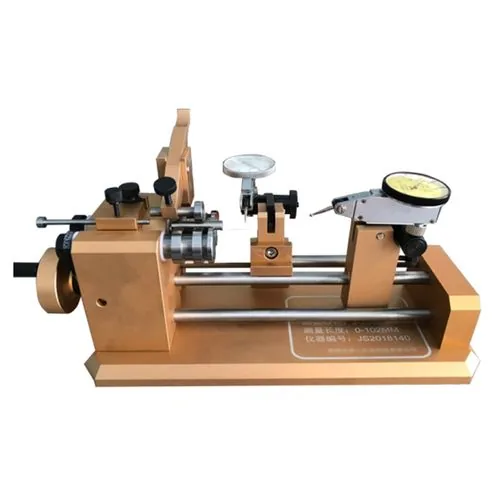
- Geometric — concentricity and runout on cylindrical housings, plus profile checks on drawn and stamped edges.
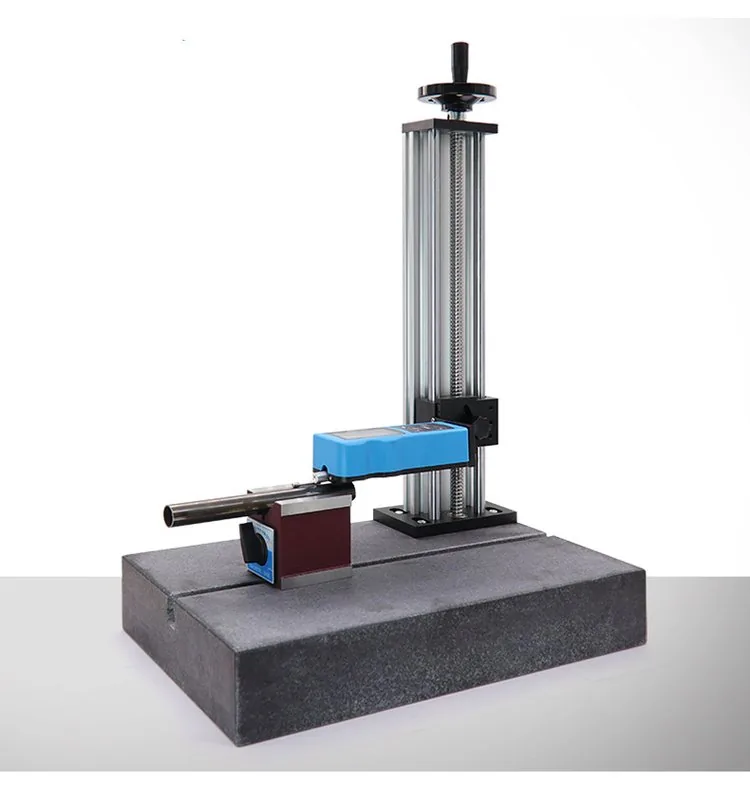
- Surface finish — Ra on formed and machined surfaces.
- Hardness — incoming material and formed parts, measured on a Rockwell tester.
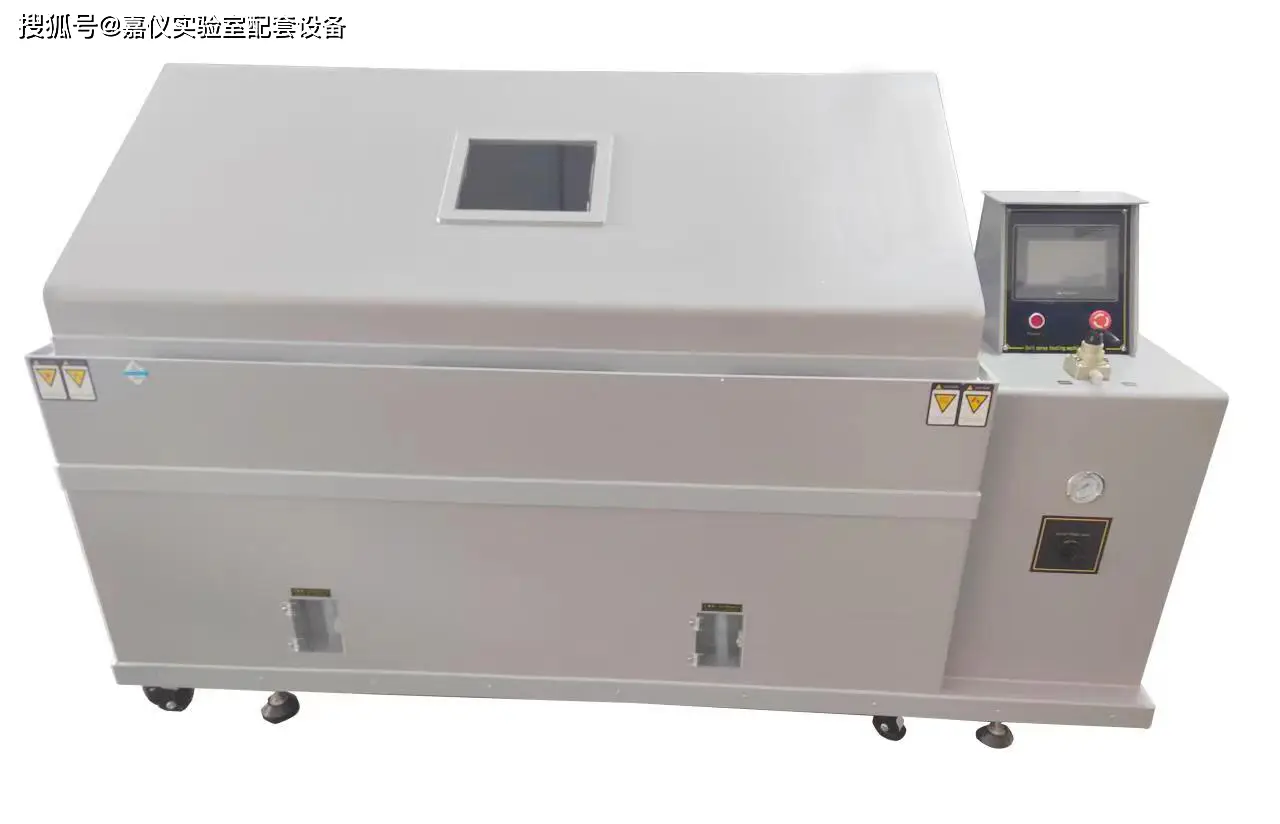
- Corrosion — salt spray testing on plated and passivated parts.
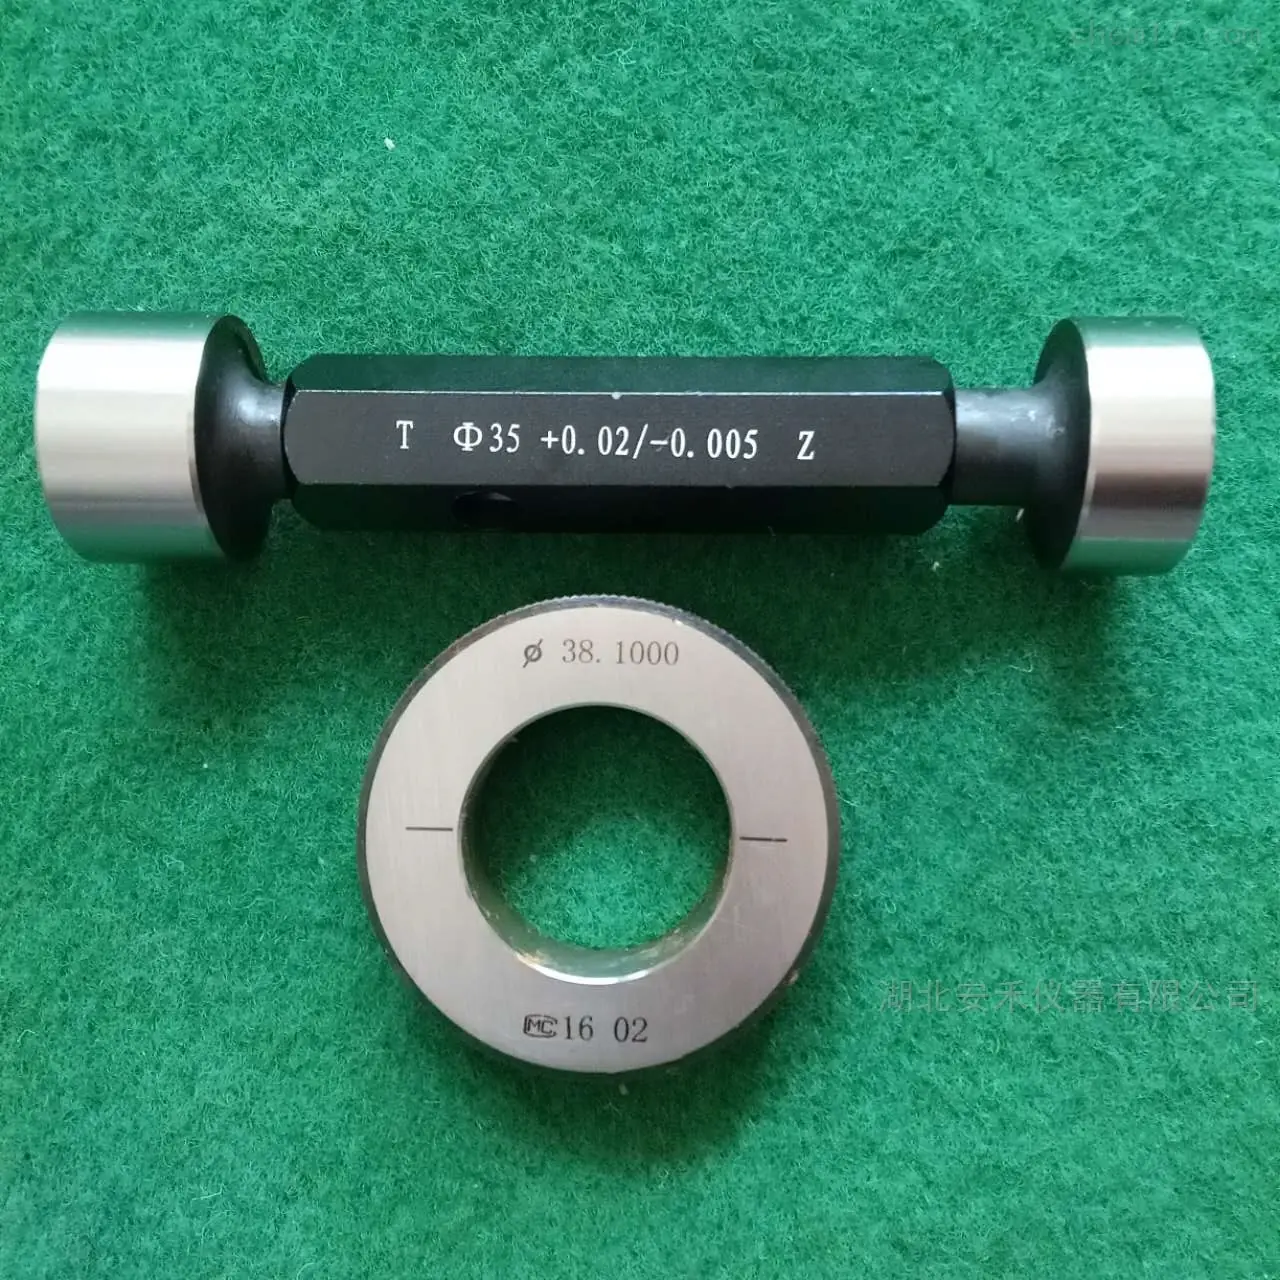
- Attribute checking — go/no-go gauging at the press for holes, slots and positions.
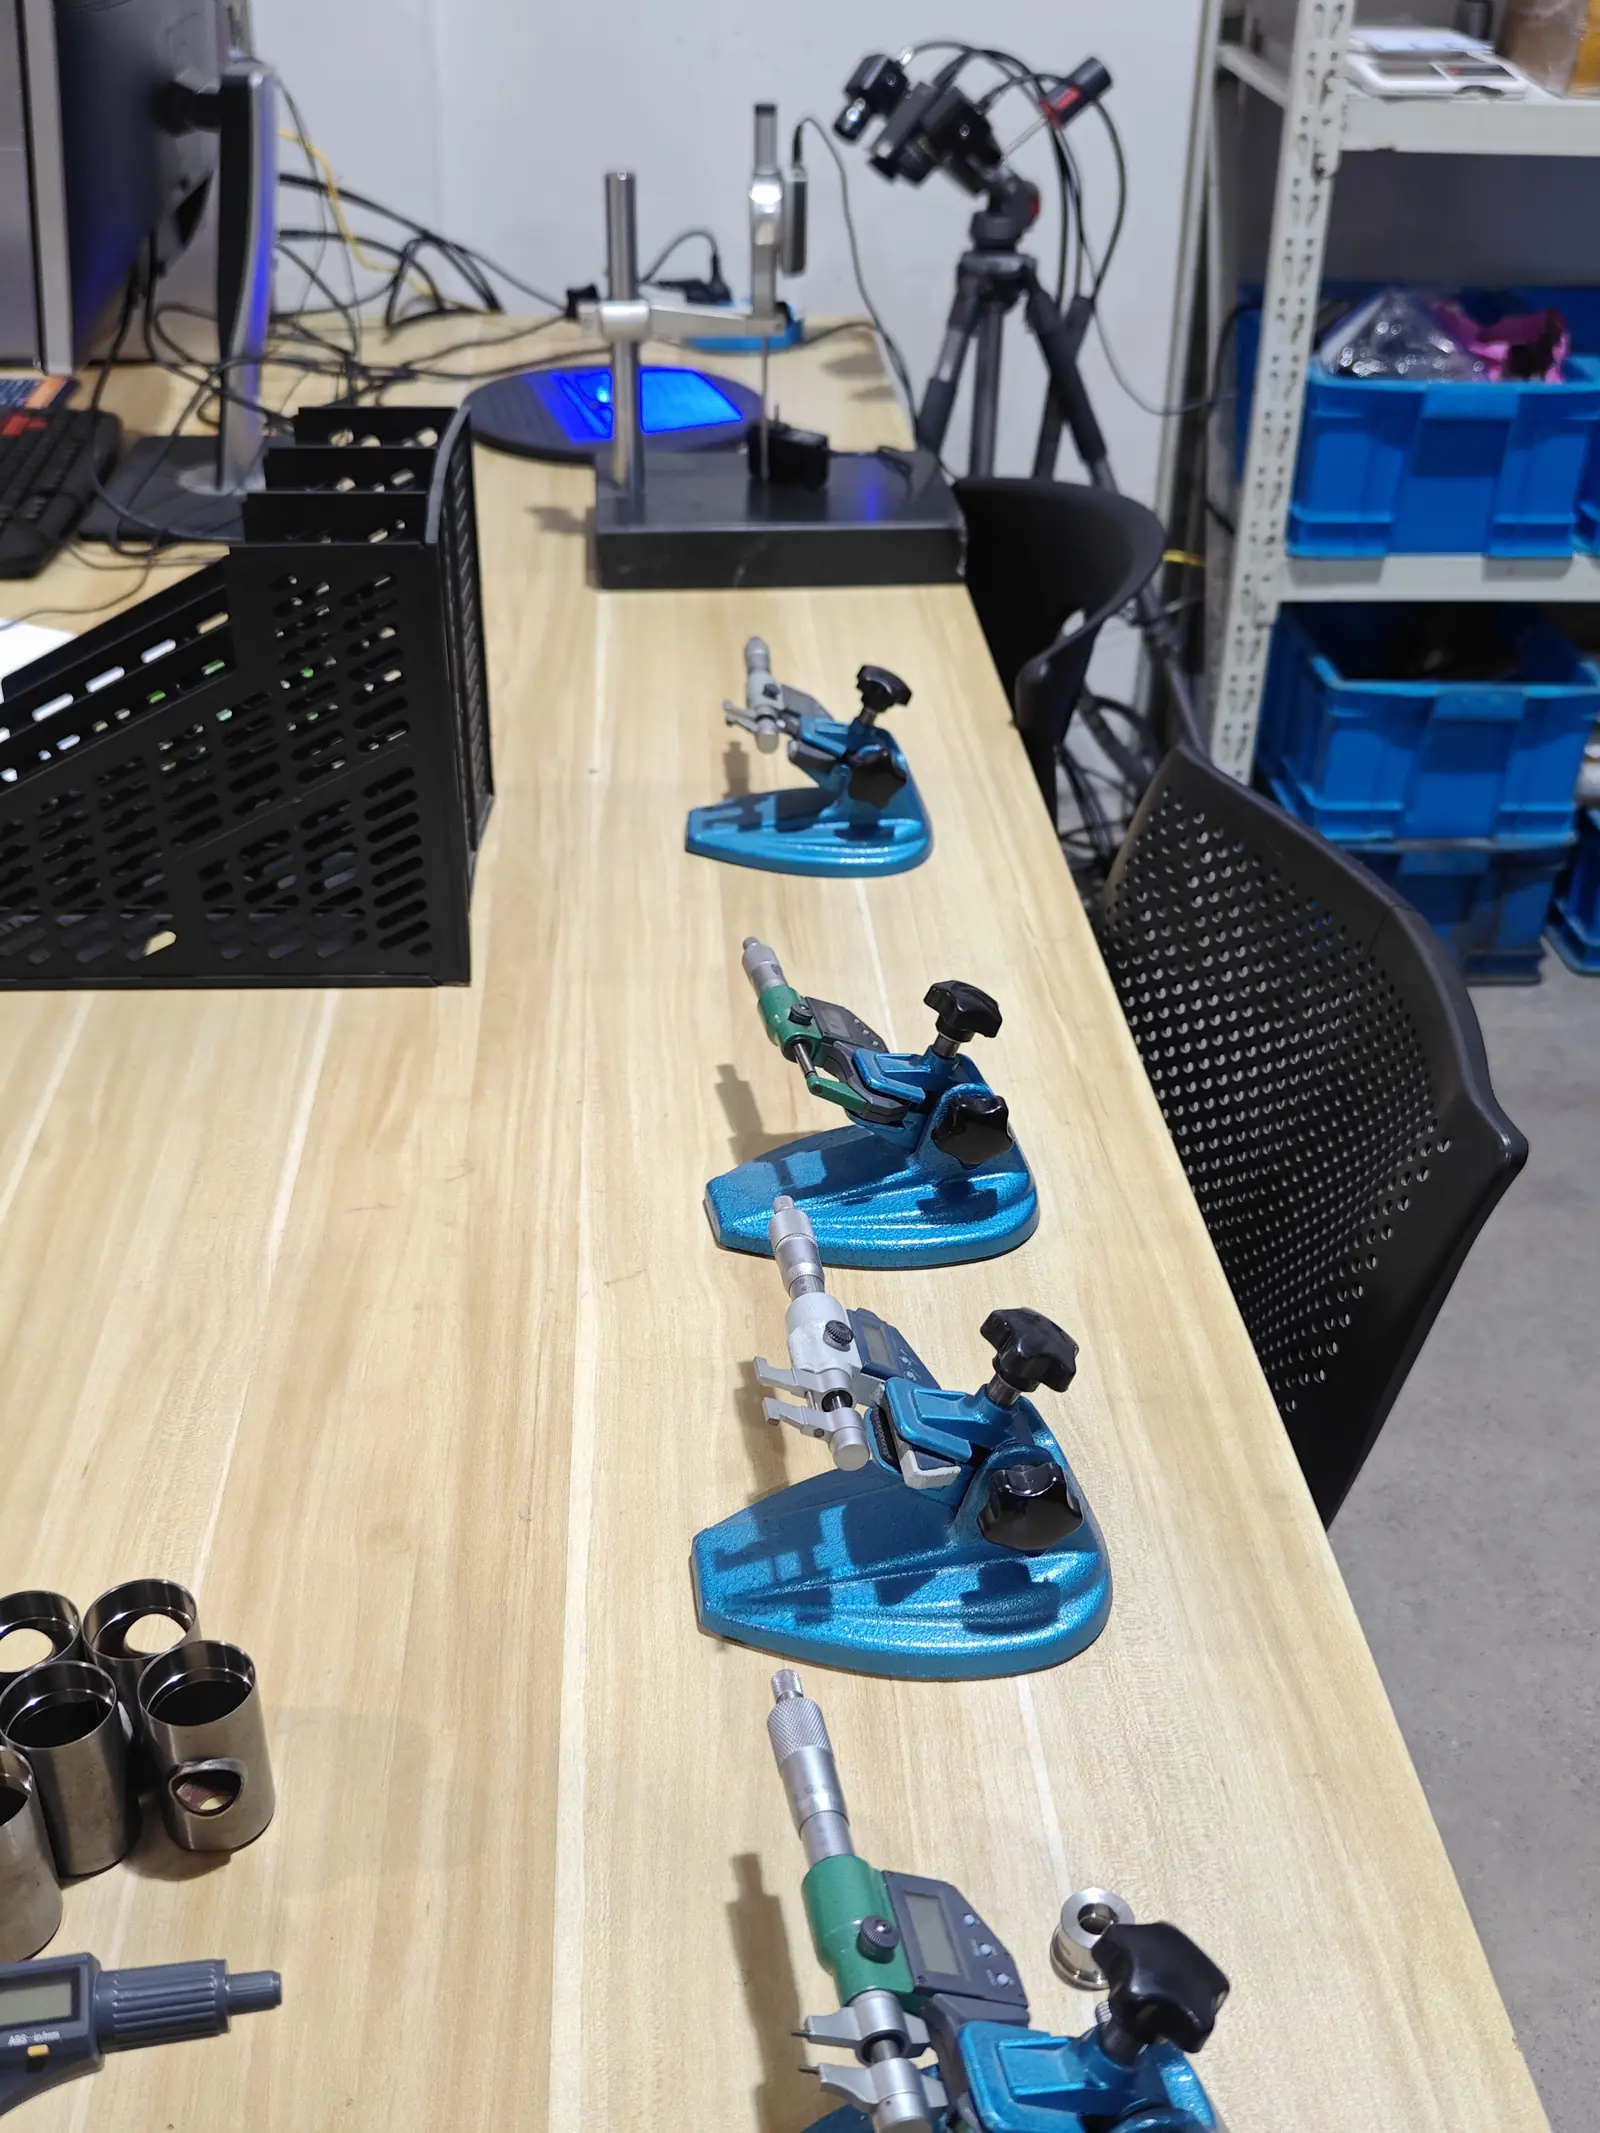
Equipment in the inspection lab
Also in the lab
- 3D scanner ×1 — for free-form geometry and first-article comparison against the model.
- Rockwell hardness tester ×1 — incoming material and formed-part hardness checks.
- Digital height gauge (0.001 mm resolution) — heights and step positions on flat and formed parts.
- Internal callipers and a full go/no-go gauge set for shop-floor attribute checking.
- Flash measuring instrument ×1 — fast batch measurement of high-volume features.
How first article inspection runs
- The drawing becomes a characteristic list. Every dimension with a tolerance becomes a numbered characteristic, with the critical ones flagged.
- Material and hardness are confirmed first — measuring a formed feature on the wrong material is wasted effort.
- The part is measured against the list, using the instrument that suits each feature: optical projection and micrometers for profiles and diameters, depth gauge for drawn depths, concentricity gauge for bore relationships, roughness tester for finishes.
- Results are recorded with the nominal, the tolerance and the actual value, so the report shows not only whether the part passed but how much margin it had.
- Anything out of tolerance goes back to the process before the production run continues, not after the batch is complete.
The same measurements, extended across the production run with control plans and in-process checks, are what make a Level 3 PPAP package possible. See PPAP capability for the documentation side.
What the lab does not do
Being precise about the boundary is more useful to a buyer than a longer equipment list:
- No coordinate measuring machine (CMM). For complex free-form geometry we use the 3D scanner, and for parts that need a formal CMM report we arrange measurement with a partner laboratory and say so before quoting.
- No in-house metallurgical laboratory. Hardness is checked here; full material certification comes from the mill, and heat treatment is carried out by qualified partner plants.
- Corrosion testing is verification, not qualification. The salt spray chamber confirms what our plated parts do; it does not replace the surface-treatment supplier's own qualification.
Metrology in use
Cylindricity on a deep drawn tube — the kind of measurement behind every first article inspection report.
Frequently asked
Do you provide a first article inspection report with the parts?
Yes. First article inspection is a standard step on a new tool, and the report lists each characteristic with its nominal, tolerance and measured value. It is normally issued before the production run is released.
Can I specify the measurement method for a critical dimension?
Yes, and it is better if you do. Tell us the characteristic, the method your drawing or control plan calls for, and the gauge to be used. Where the method is not specified, the DFM review proposes one and the control plan records it.
How do you handle a dimension that is out of tolerance?
The finding goes back into the process — tool adjustment, process parameter change or a correction in the sequence — and the part is re-measured. Nothing is shipped on the assumption that the next batch will be better.
Is the inspection lab used for incoming material too?
Yes. Incoming material is checked against the mill certificate and the grade on the drawing — dimensions, hardness where relevant, and material identification — before it is released to the press.
Can you measure parts made from someone else's tooling?
Yes. The lab inspects whatever comes through the plant, including parts from tooling transferred to Balford, and the measured results are reported the same way.