Metal Components for Hydraulic Systems: Deep Drawn Valve Housings
Balford manufactures deep-drawn and precision-stamped components for hydraulic systems — cartridge and proportional valve housings, solenoid valve bodies, sleeves, spring seats and brackets. Production follows ISO 9001:2015 with IATF 16949-aligned quality controls on a 12,000 m² facility with 500+ machines.
Why Balford for Hydraulic Components
- Pressure integrity through deep drawing. Seamless drawn housings and sleeves eliminate weld lines and leak paths, holding burst pressure and sealing faces consistently across the run.
- Material range matched to the circuit. Carbon steel for strength and cost, stainless steel for corrosion resistance, pure iron (DT4E) where solenoid actuation is integrated — grade is reviewed with your engineers before tooling.
- ISO 9001:2015 with IATF 16949-aligned quality management, with PPAP-aligned documentation, FAI reports and material certifications available on request.
- Secondary operations in-house: machining of sealing faces, plating coordination (zinc-nickel, nickel), annealing for magnetic requirements and assembly support.
Featured Case Studies
Selected hydraulic projects from Balford’s production history. Material, process and application data come from each case record.

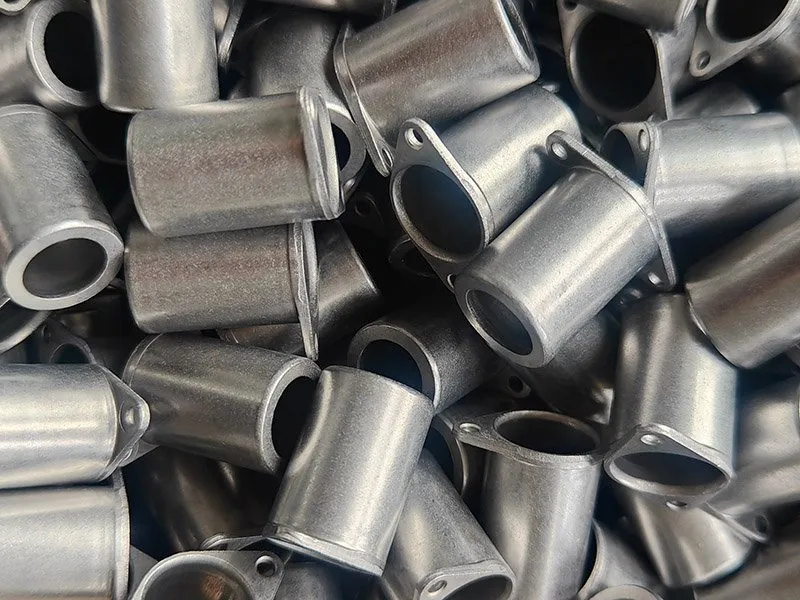

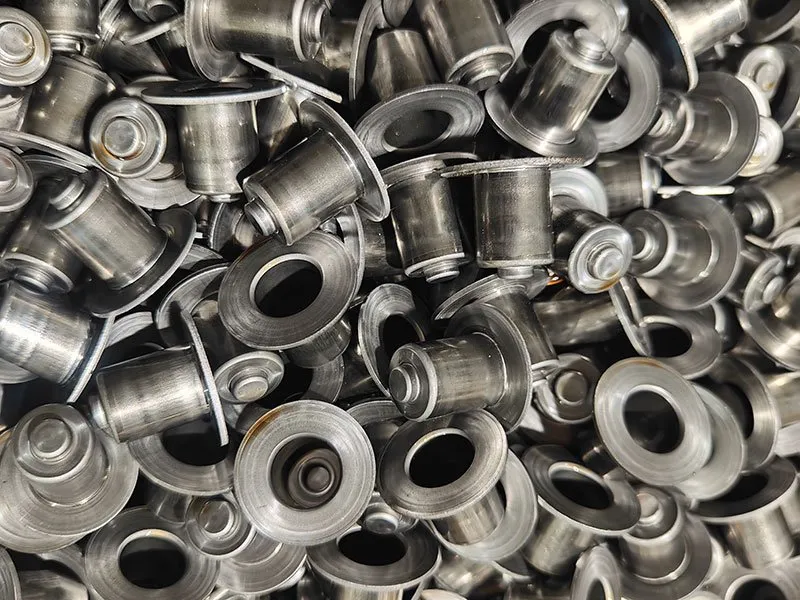
Manufacturing Capabilities by Part Type
| Part Type | Typical Process Route | Key Requirements |
|---|---|---|
| Cartridge valve housings | Deep drawing → machining | OD/ID control, clean surface, sealing face finish |
| Proportional valve housings | Deep drawing → anneal → machining → plating | No draw lines/scratches, magnetic & corrosion spec |
| Solenoid valve bodies (hydraulic) | Deep drawing (pure iron) → electroplating | Concentricity, ID tolerance, plating adhesion |
| Spring seats / cups | Stamping + drawing | Consistent depth, small R angles |
| Fittings, caps and brackets | Stamping, bending, secondary machining | Dimensional stability, batch consistency |
Press range 25 t to 350 t; coil-fed progressive lines for high volumes; CNC machining for sealing faces and threads.
Engineering & Quality Considerations
- Wall thickness and concentricity are controlled in the draw tool rather than by machining, which keeps costs predictable on valve bodies with thin walls.
- Sealing faces that must hold O-rings or cartridge seals are reviewed during DFM so that flatness, surface finish and edge breaks are achievable in the planned sequence.
- Corrosion protection for mobile and industrial hydraulics: zinc-nickel, nickel plating or passivation options are quoted with the part.
- Annealing after heavy draws restores ductility and, where the housing is part of a magnetic circuit, controls coercivity before assembly.
- Volume planning: prototype tooling first, then production progressive dies once the part design is frozen — same as our automotive valve work.
Frequently Asked Questions
Deep-drawn and stamped valve housings (cartridge, proportional, solenoid), sleeves, spring seats, caps, fittings and brackets for hydraulic circuits — typically in carbon steel, stainless steel or pure iron, with machining and plating as required.
Yes. Housing bores and seating faces that interface with cartridge valves are controlled through drawing + machining with in-process gauging; DFM review confirms achievable tolerances against your print before tooling starts.
Yes. Prototype tooling is used to validate the draw sequence and material, then production is transferred to progressive or transfer tooling sized for your annual volume.
Zinc-nickel, zinc, nickel and passivation are the common choices for hydraulic housings; we coordinate with qualified plating partners and verify coating thickness on request.
Yes. Balford exports valve housings and components to hydraulic and fluid-power OEMs in Europe, the Americas and Asia, with PPAP-aligned documentation on request.
Have a Drawing or 3D Model?
Send us your 2D drawing or STEP/IGES model. We will review material, tolerances, forming requirements and production volume before quoting.