Capacity & equipment
Machinery & Equipment List
The numbers buyers ask for first: up to 350 t, deep drawing up to Ø250 mm, transfer, progressive and deep-draw tooling, and a complete in-house tool room that machines, wire-cuts and welds its own dies — with a small furnace kept for emergency die repairs and bulk heat treatment handled by audited partners.
Forming and press capacity
| Item | Specification | Status |
|---|---|---|
| Press capacity | up to 350 t | In-house |
| Maximum deep draw diameter | Ø250 mm | In-house |
| Transfer press stamping | Multi-station transfer tooling, part carried between stations | In-house |
| Progressive die stamping | High-volume strip tooling with carrier web | In-house |
| Compound, blanking and bending dies | Washers, caps, brackets and formed sheet metal parts | In-house |
| Deep drawing stages | Multi-stage drawing with inter-stage annealing where needed | In-house |
| Materials | Carbon steel, stainless steel, brass, copper, aluminium, special alloys | In-house |
| Press list detail | Number of presses per tonnage band and bed sizes | Available on request |
Tool room equipment
| Equipment | Role in die making | Status |
|---|---|---|
| Internal / external cylindrical grinders | Grinding round die components, punches, pilots, core pins and bushings to final size | In-house |
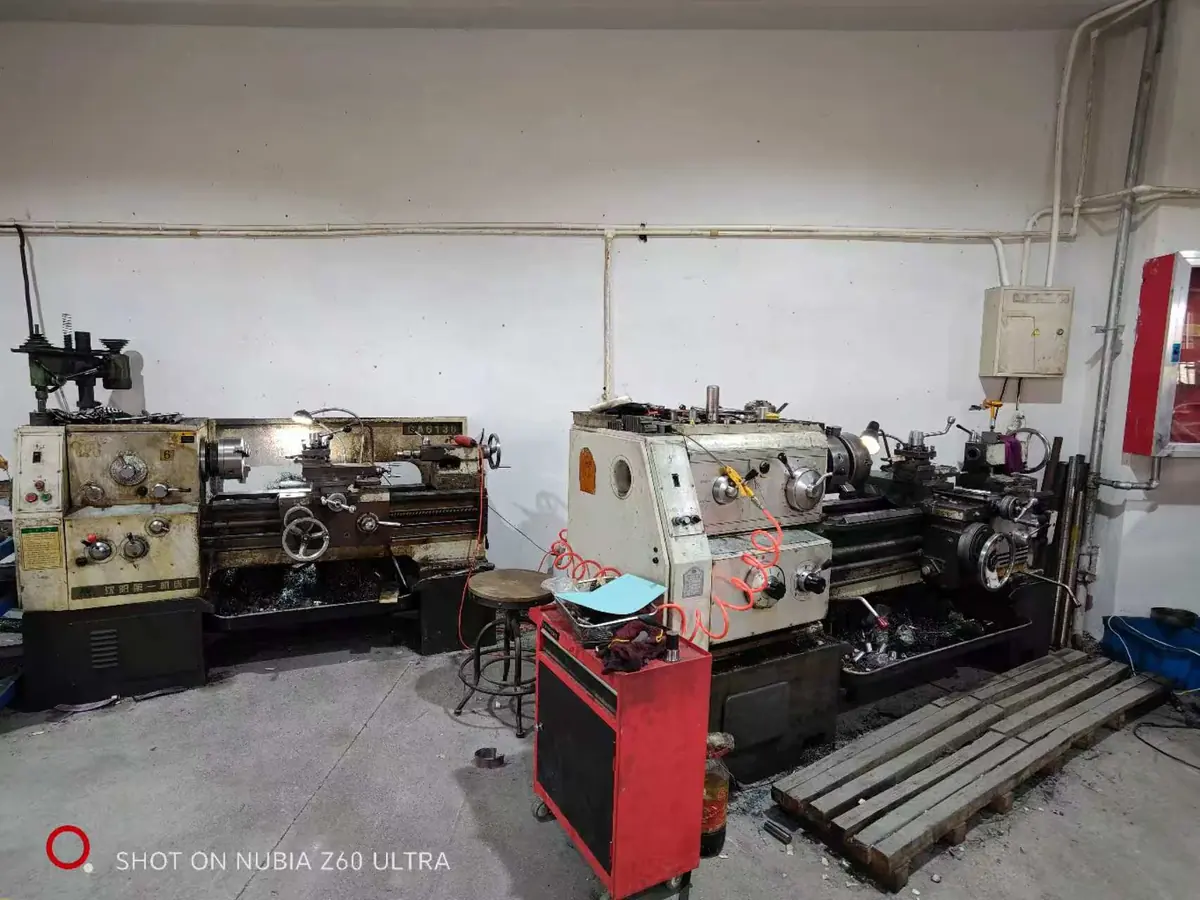
| Engine lathes (3 units) | Turning punch blanks, ejector pins, guide posts and tool room components | In-house |
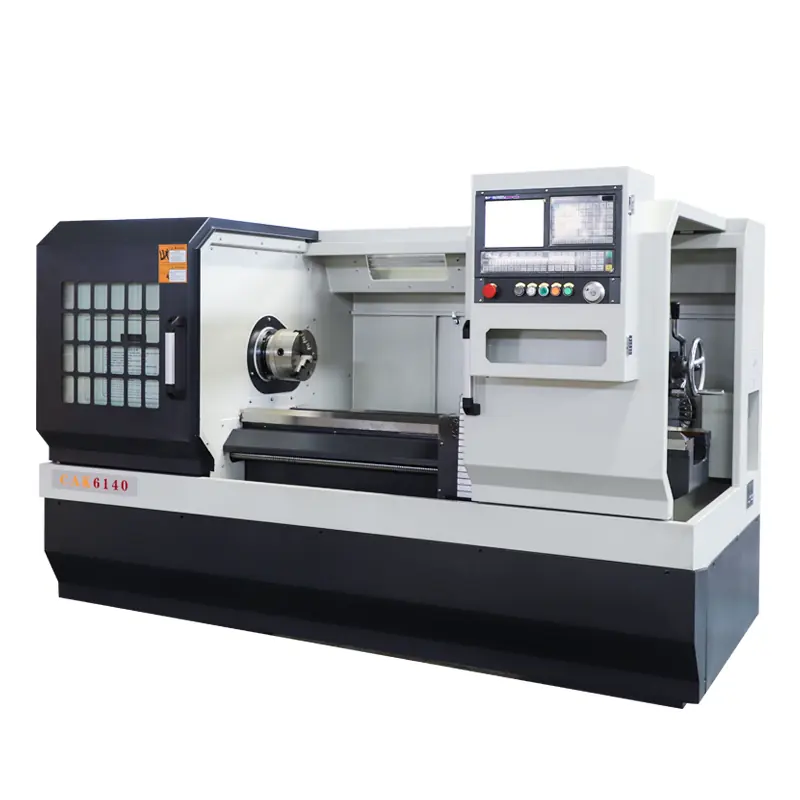
| CNC lathe (1 unit) | Precision turned components for die and mould assemblies | In-house |
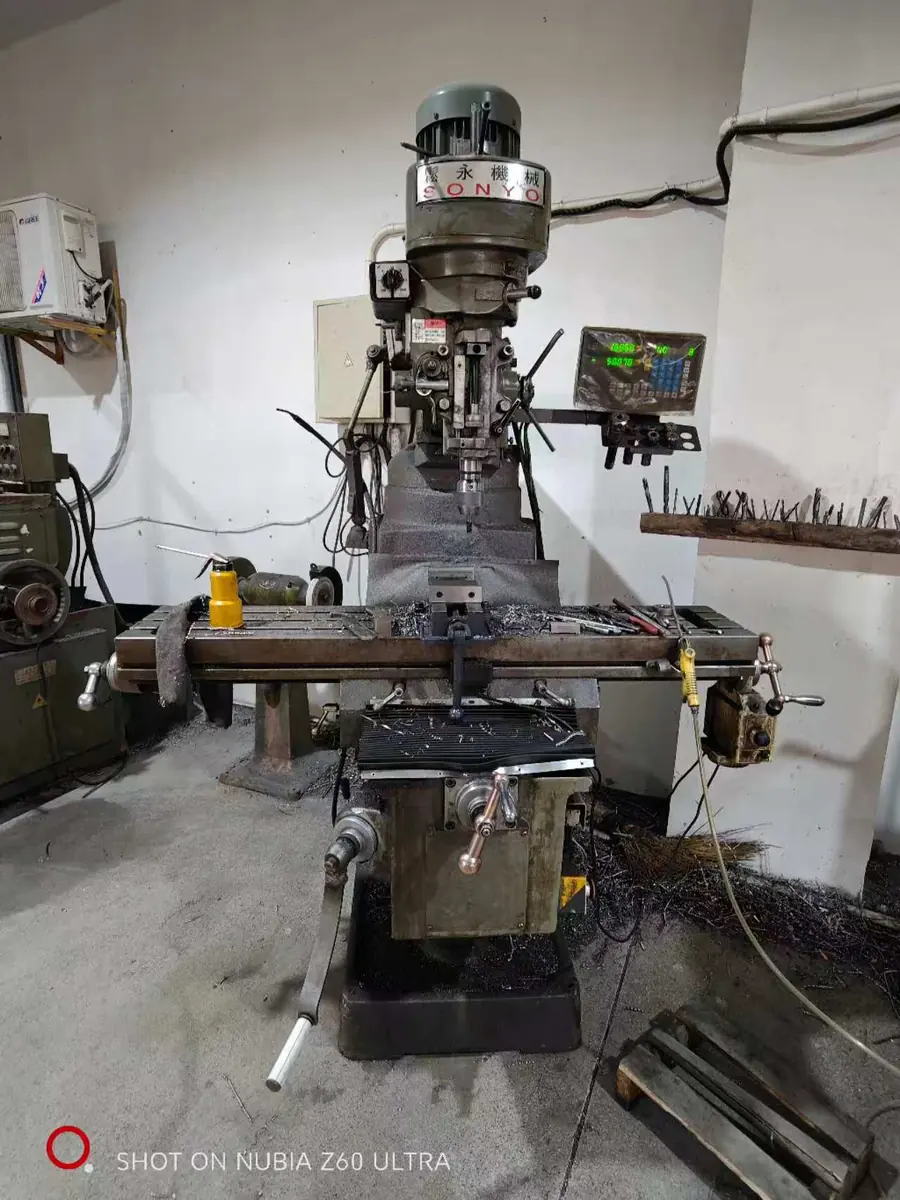
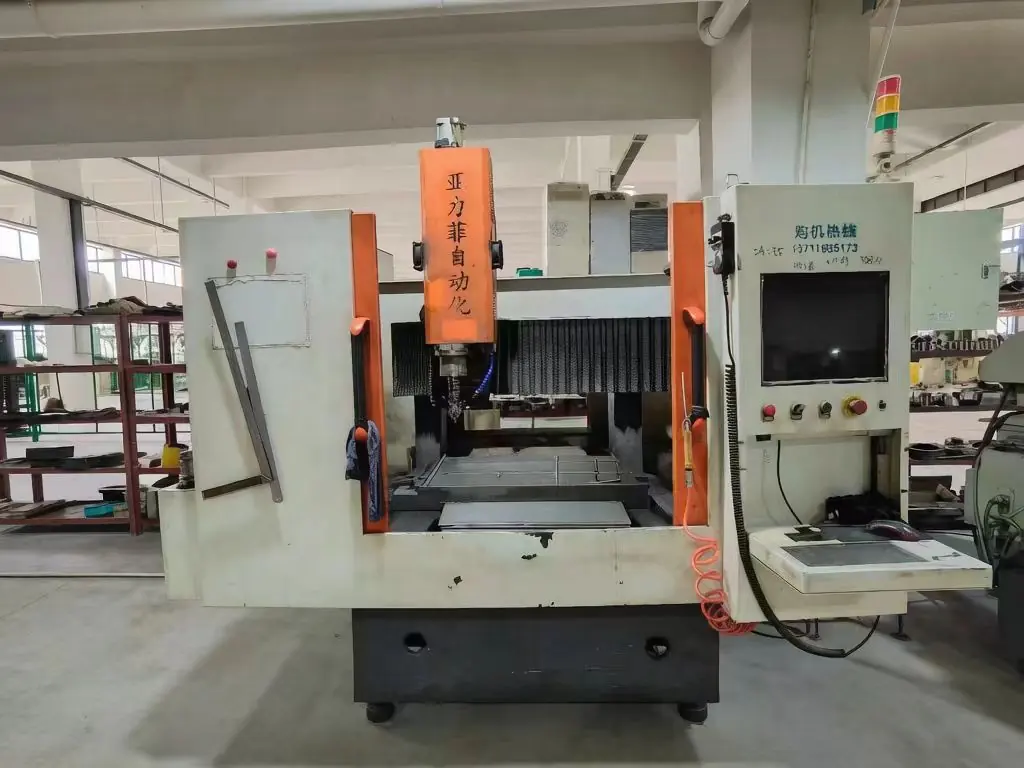
| CNC milling machines | Die plates, pockets, cavities and mounting features in hardened and pre-hardened steels | In-house |
| Precision surface grinder | Flat grinding of die plates, strippers and inserts to tight parallelism | In-house |
| Large surface grinder | Large die plates and tool bodies that do not fit standard machines | In-house |
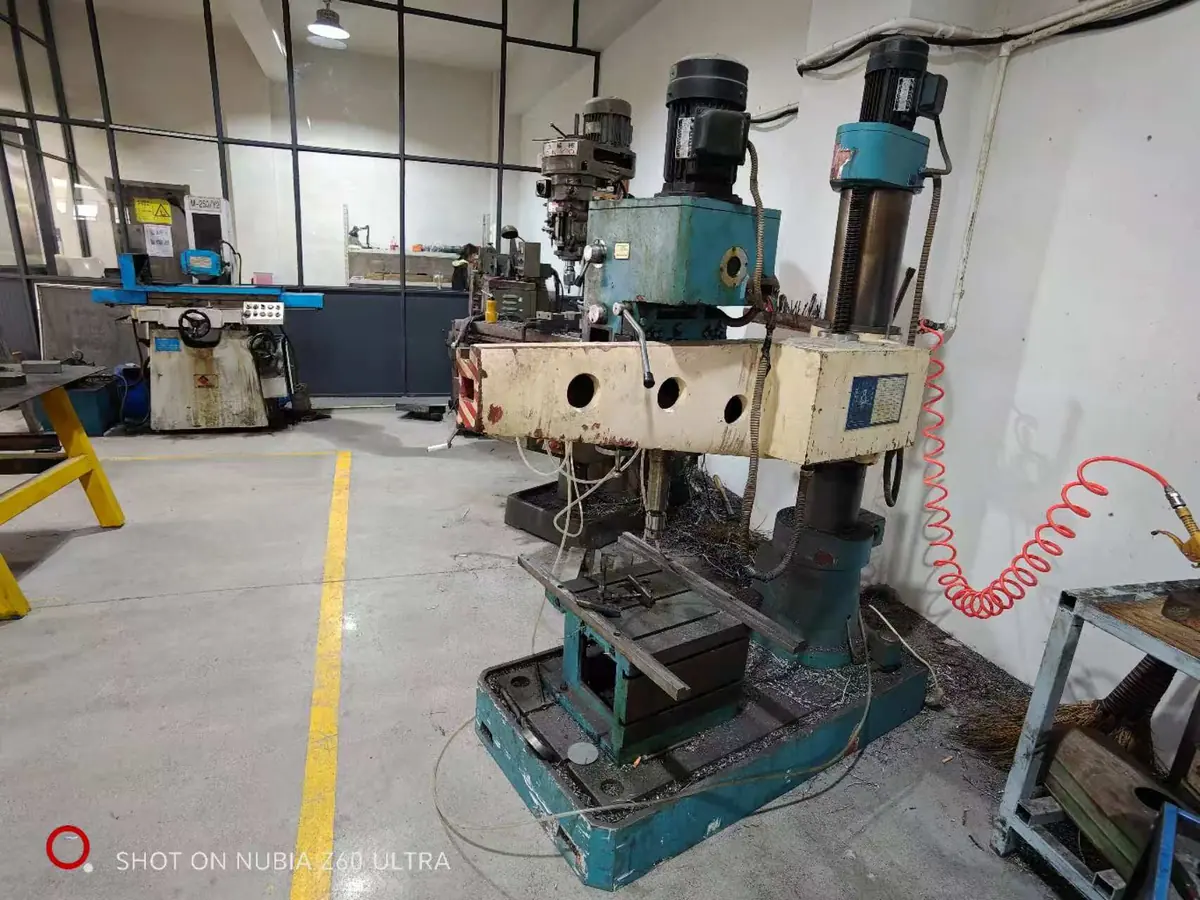
| Drilling machines | Dowel, screw and water-line holes across die sets and fixtures | In-house |
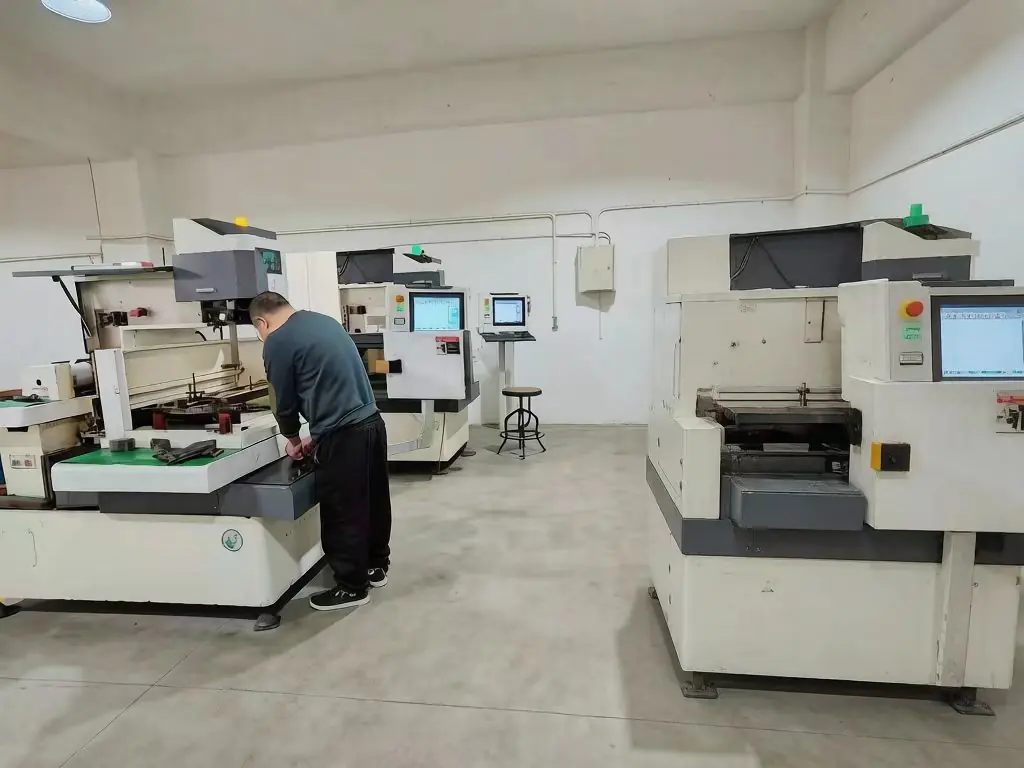
| Medium-speed wire EDM (5 units) | Die openings, punch profiles and contoured sections | In-house |
| Fast-speed wire EDM (1 unit) | Roughing and vent or slot cutting where finish demand is lower | In-house |
| EDM hole drilling / perforator | Start holes for wire EDM and small deep precision holes | In-house |
| Slow-wire EDM | Ultra-fine finish and taper-critical die details | Outsourced partner |
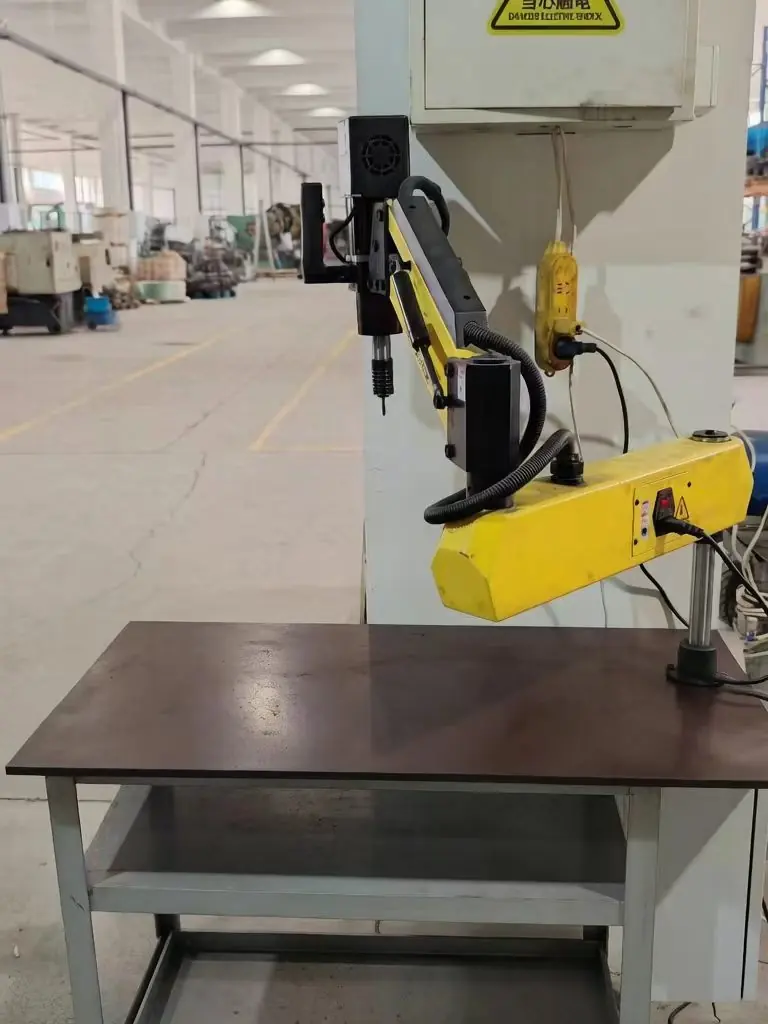
| Automatic tapping machines | Threading die plates, strippers and parts with consistent pitch and depth | In-house |
| Die cold welder | Cold-weld repair of die wear, chips and scratches without heat distortion | In-house |
| Argon arc (TIG) welder | Building up worn edges and repairing tool steel with controlled heat input | In-house |
| Pneumatic die grinders | Bench and hand finishing of radii, fillets and draw surfaces | In-house |
| Demagnetizer | Removing residual magnetism after grinding and EDM | In-house |
| Heat treatment furnace (small) | Emergency hardening and tempering of die components so a repair can be finished on site | In-house (emergency use) |
| Bulk die and tool heat treatment | Hardening and tempering of die components, with hardness and microstructure documentation returned to us | Outsourced partner |
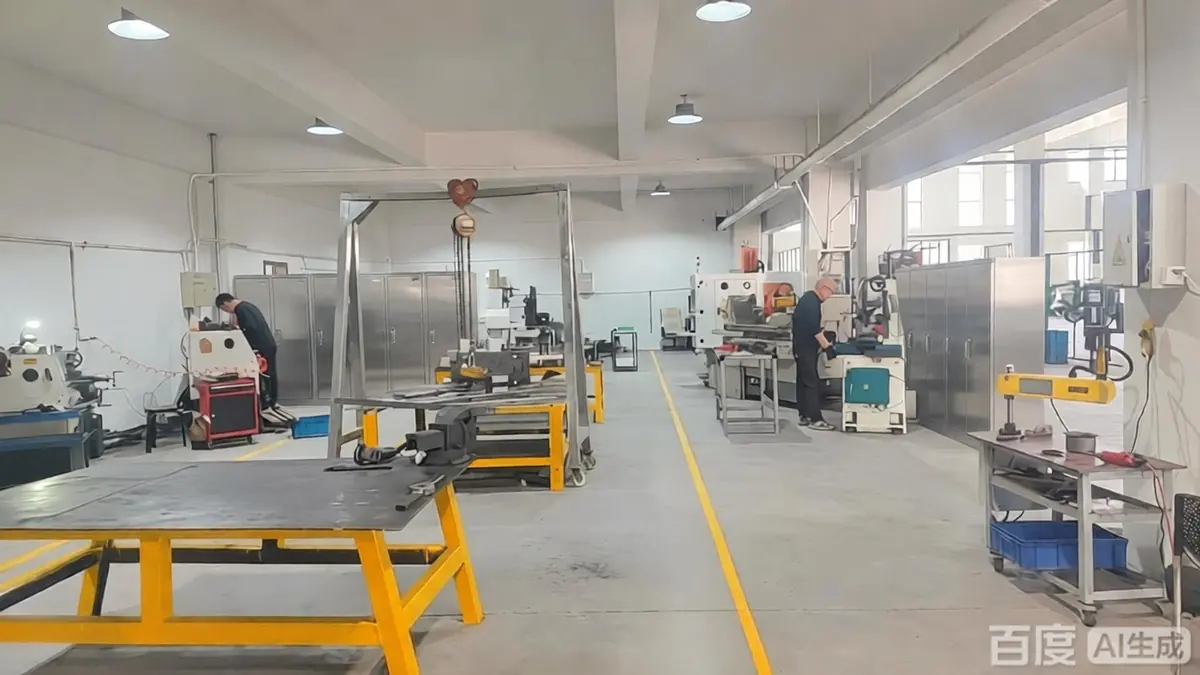
The tool room, photographed
Every machine in the table above stands in Balford's own tool room in Zhuji, Zhejiang. The photographs below were taken on our shop floor — this is the equipment your dies are built, maintained and repaired on.
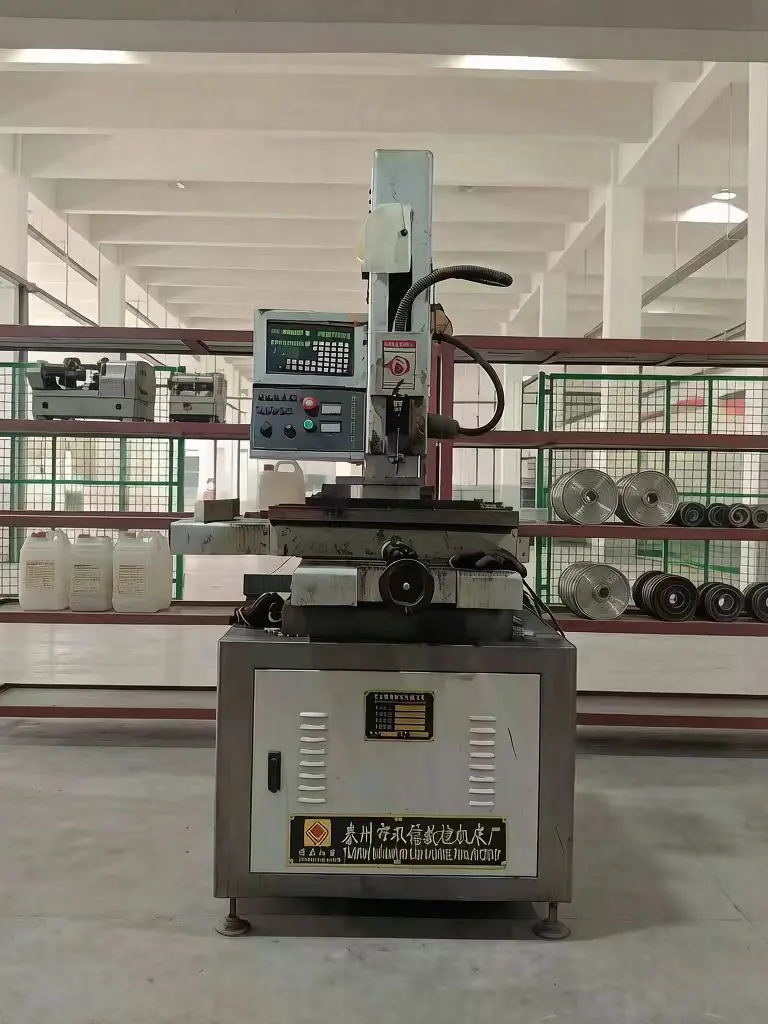
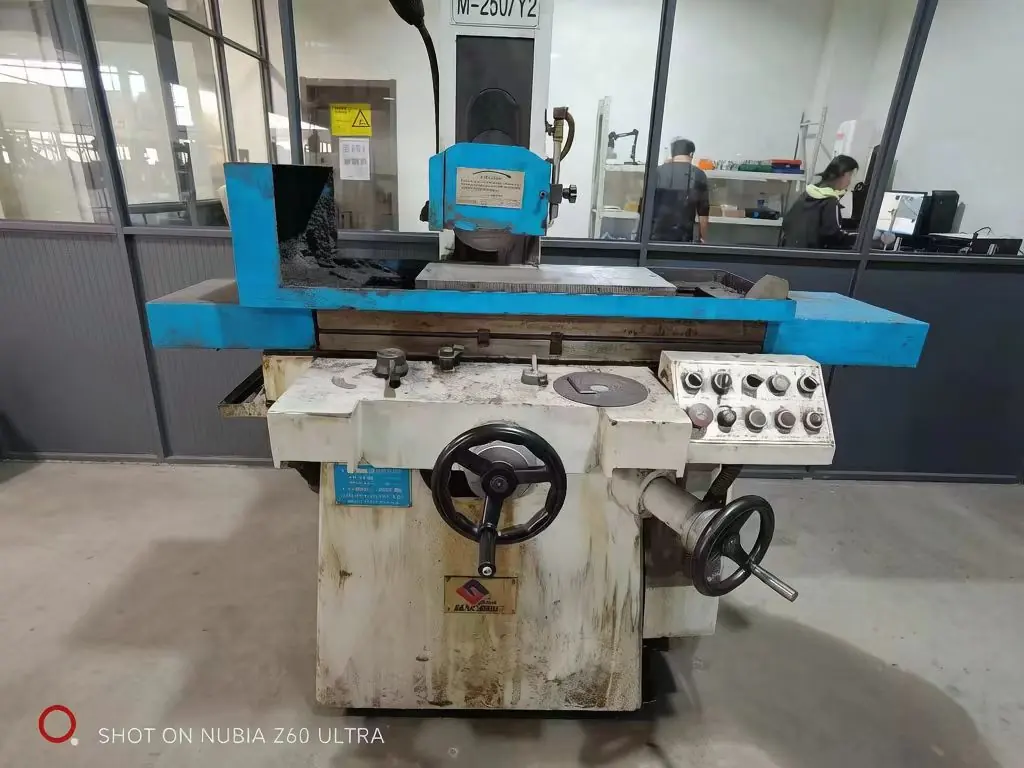
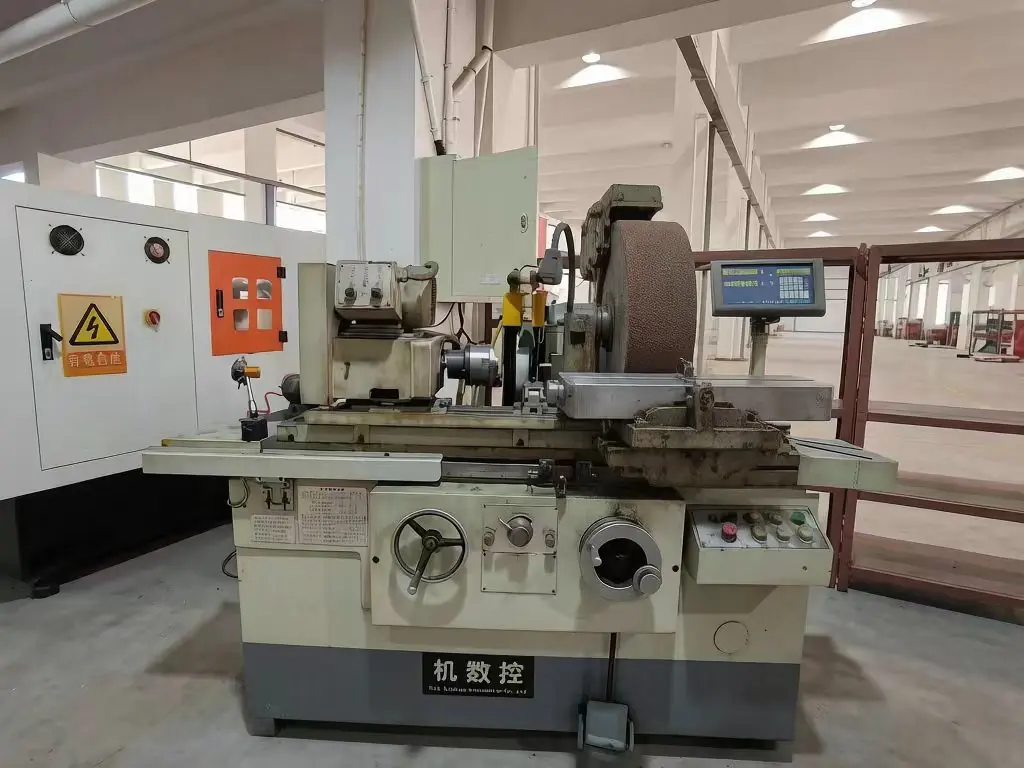
Finishing and secondary operations
| Operation | Where it runs | Why it matters |
|---|---|---|
| Deburring and edge break | In-house | Safe handling, coating adhesion and clean mating surfaces |
| Tapping (in-die or secondary) | In-house | Thread pitch and depth control without re-fixturing |
| CNC turning and milling | In-house | Sealing faces, bearing seats and concentricity after drawing |
| Grinding (tool room) | In-house | Die plates, punches and tooling components to final size |
| Hardening and tempering (production parts) | Outsourced — qualified partner | Hardness and toughness after forming, with certificates returned to us |
| Annealing and stress relief (production parts) | Outsourced — qualified partner | Restores ductility between draw stages |
| Demagnetisation (production parts) | Outsourced — qualified partner | Controls residual magnetism on solenoid and sensor parts |
| Emergency die heat treatment | In-house (small furnace) | Lets a die repair be finished on site without waiting for a partner |
| Passivation (stainless) | Outsourced — qualified partner | Restores corrosion resistance after drawing and machining |
| Electropolishing | Outsourced — qualified partner | Removes surface peaks, improves cleanability |
| Plating: zinc, zinc-nickel, nickel, chrome | Outsourced — qualified partner | Corrosion protection and conductive or decorative surfaces |
| Phosphating and pickling | Outsourced — qualified partner | Pre-treatment for bonding or further forming |
| Powder coating and painting | Outsourced — qualified partner | Colour, durability and electrical insulation |
Measuring and inspection equipment
| Instrument | What it verifies | Quantity |
|---|---|---|
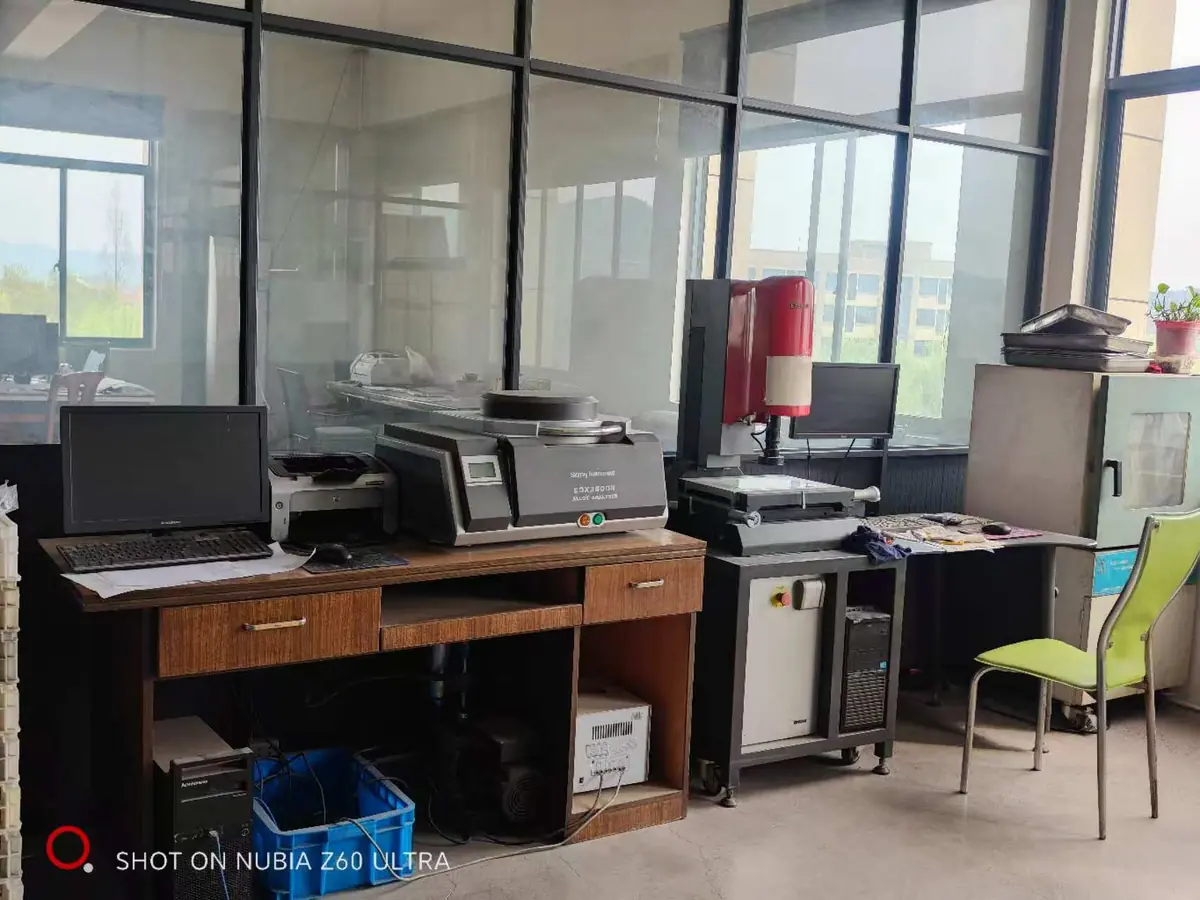
| 2.5D optical measuring projector (3D Family) | Profile, radius, angle and form on drawn and stamped features | 1 unit |
| Instant vision measuring system (flash measurement) | Rapid full-part dimensional checks on small components | In service |
| Digital height gauge, 0.001 mm resolution | Heights, steps and reference faces | In service |
| Portable surface roughness tester | Ra / Rz on sealing faces and machined surfaces | 1 unit |
| Rockwell hardness tester | Hardness verification after heat treatment | 1 unit |
| Salt spray test chamber (model 20) | Corrosion resistance on plated, passivated and coated parts | 1 unit |
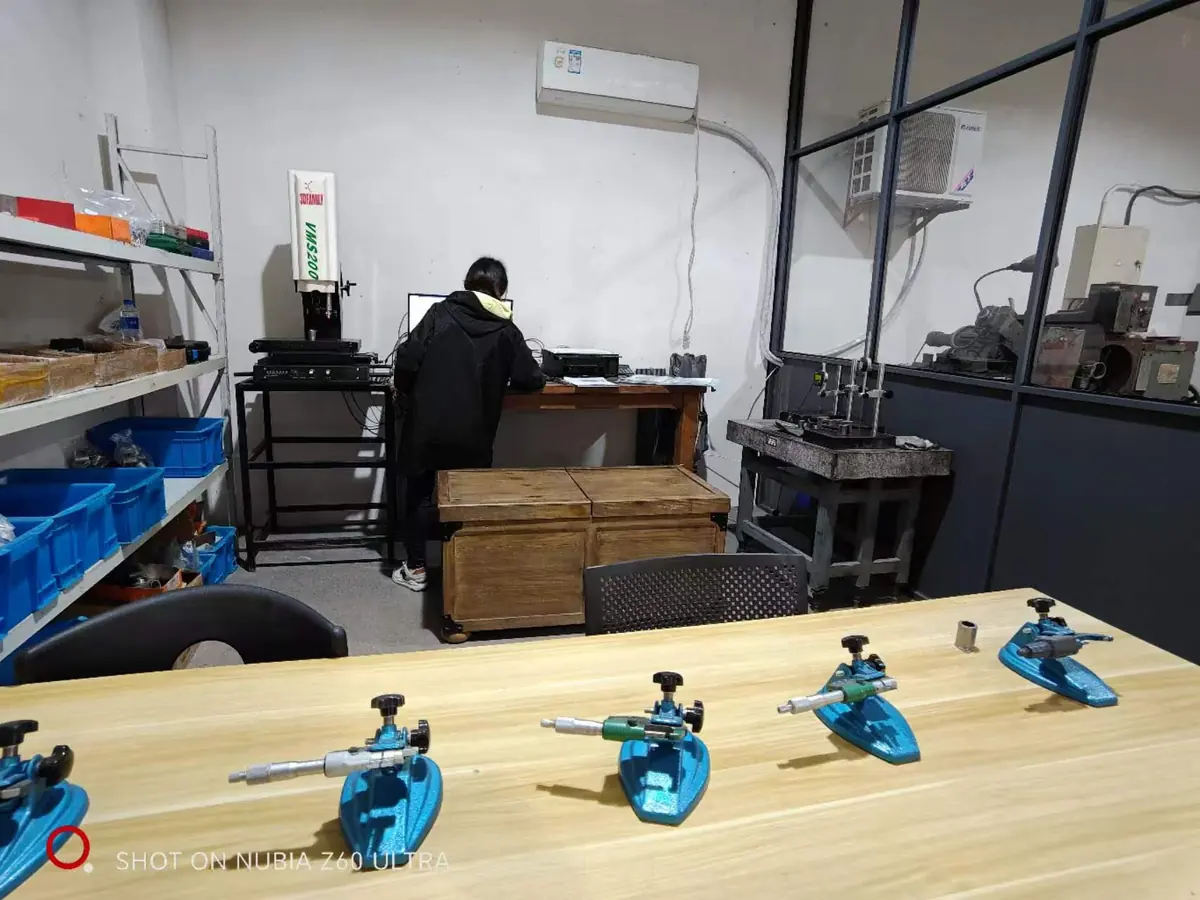
| Outside micrometers | External diameters and wall thickness | 10 units — 7 at the 50 mm range, 1 at the 100 mm range |
| Three-point bore micrometers | Internal diameters of drawn bores and sleeves | 5 units |
| Inside caliper gauges and plug / go-no-go gauges | Holes, slots and thread fits | Full sets |
| Concentricity gauge | Coaxiality and runout on housings and sleeves | In service |
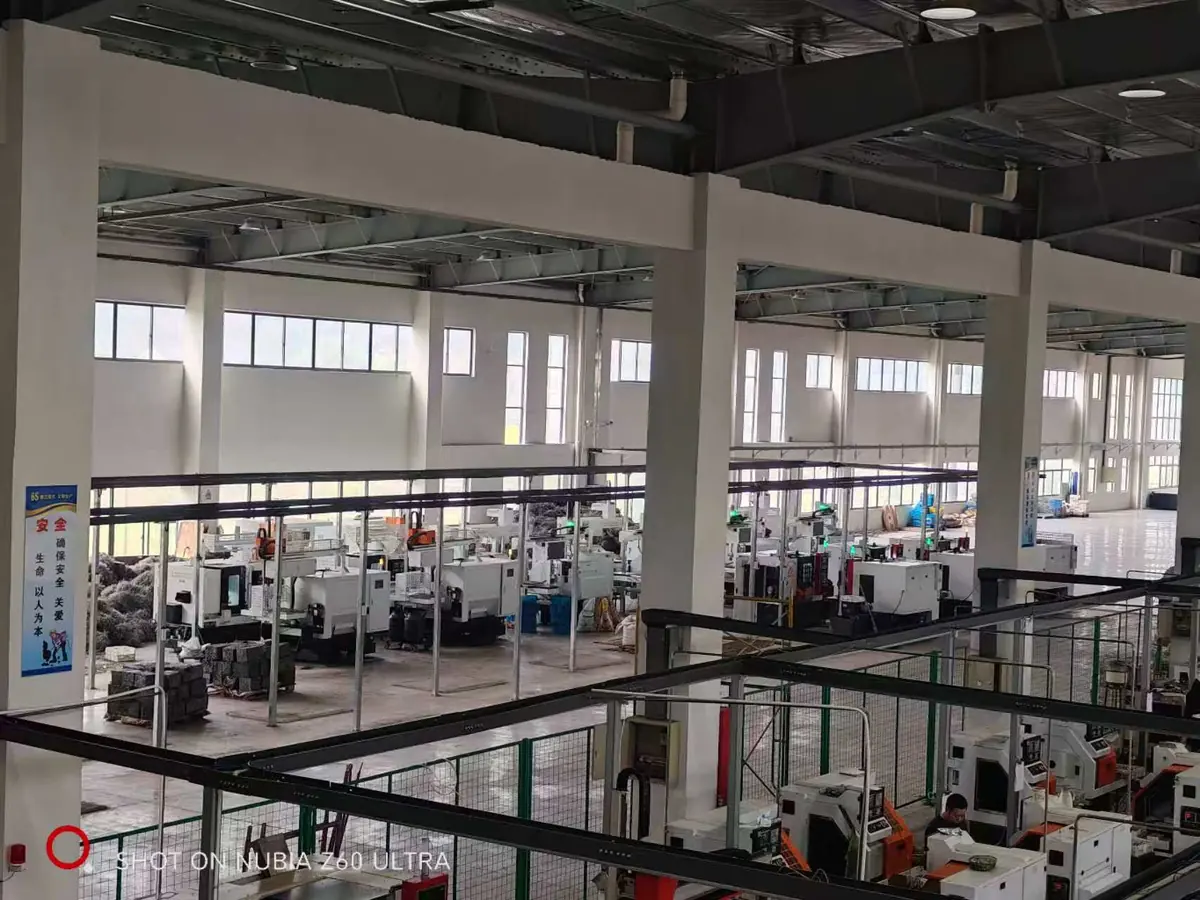
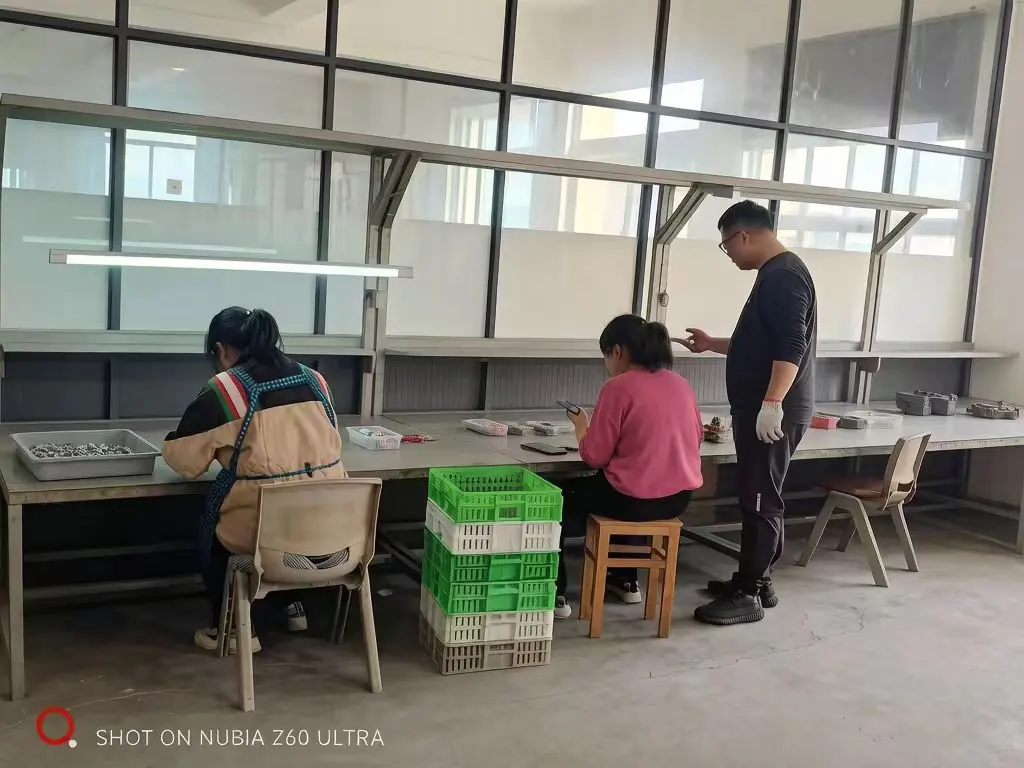
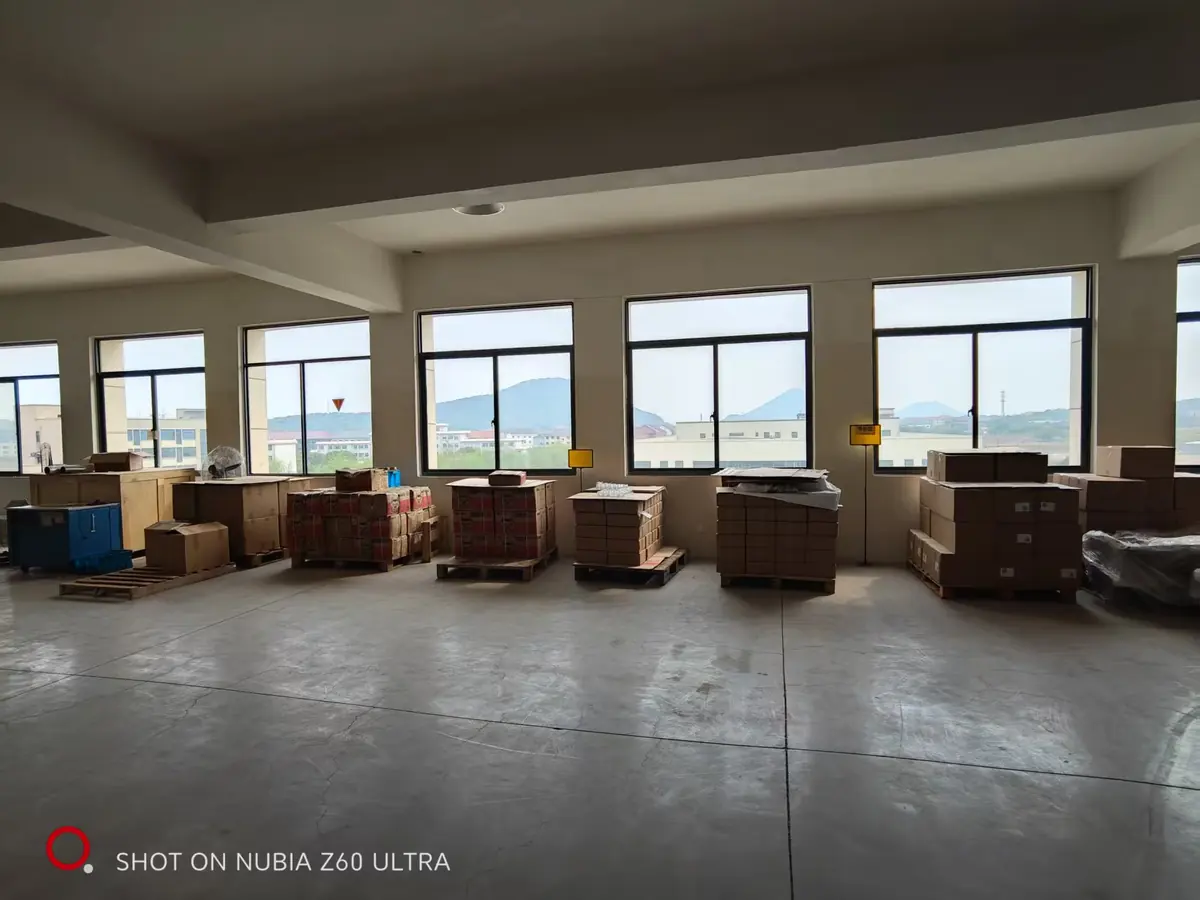
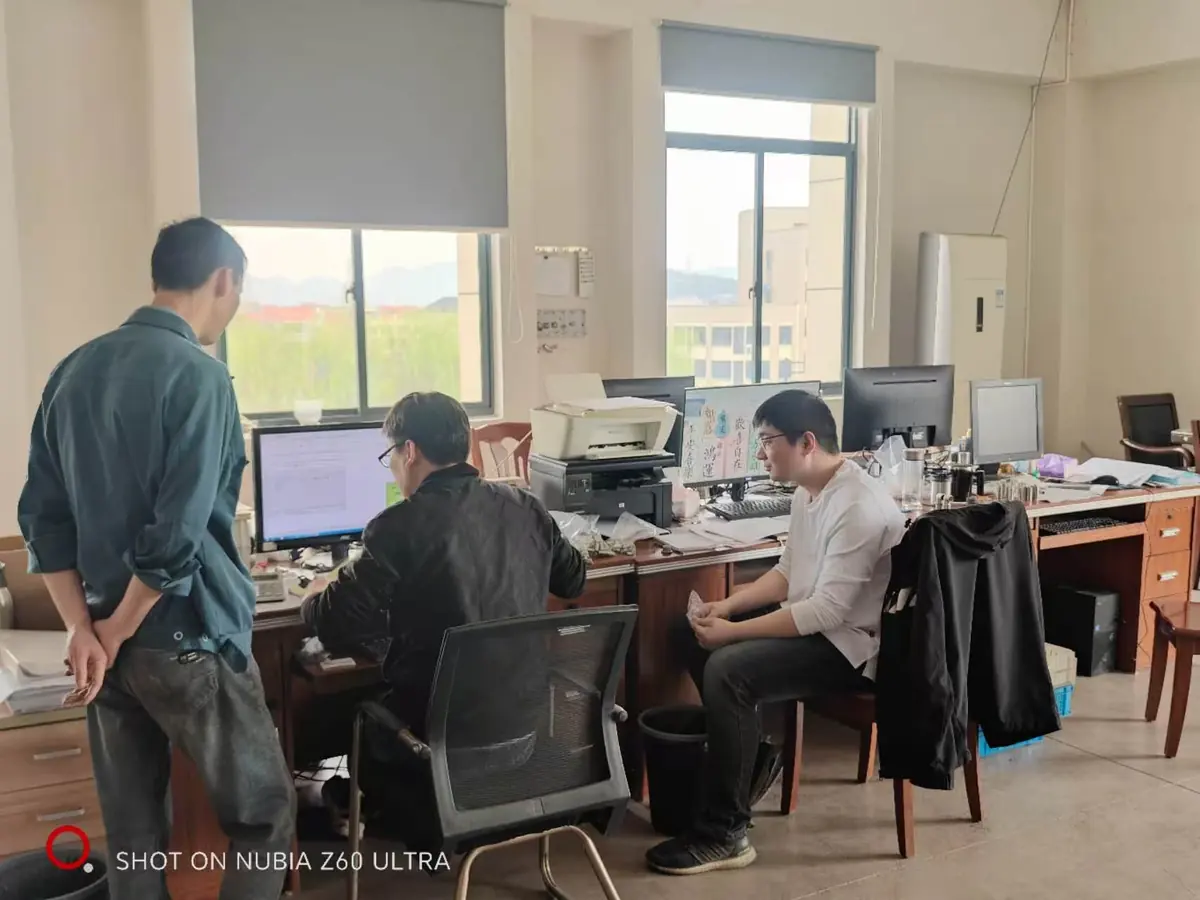
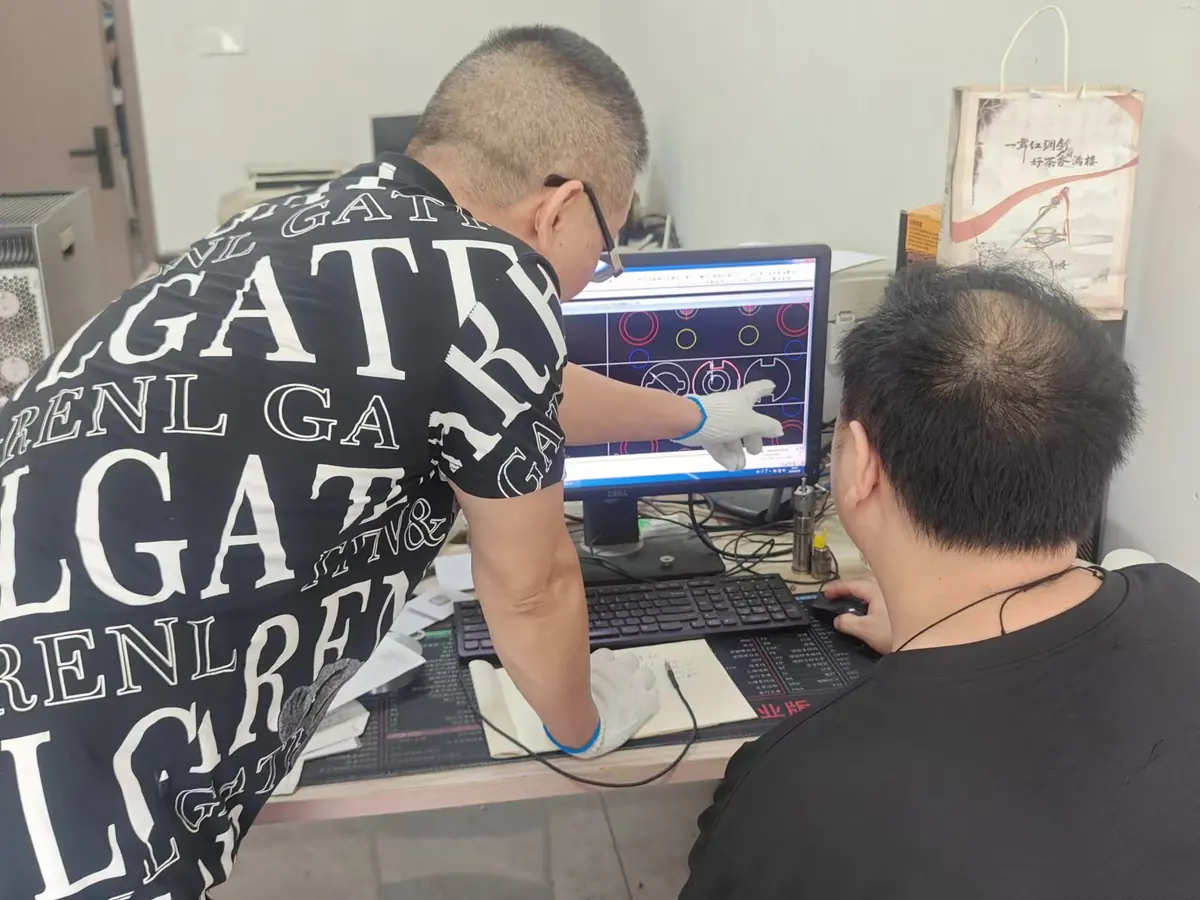
Inside the plant: inspection, stores and despatch
The areas a visiting buyer walks through, from in-process inspection to the loading bay. Approved projects are welcome to arrange a plant visit and see them in person.
Frequently asked questions
What is your maximum press tonnage?
Press capacity at Balford runs up to 350 t, which covers deep drawn housings and stamped parts where the required forming force is set by the draw ratio, material grade and wall thickness.
What is the largest diameter you can deep draw?
Maximum deep draw diameter is Ø250 mm. Above that, the limiting factor is usually the draw depth and material rather than the press, so the part is reviewed case by case during DFM.
Which steps are outsourced?
Heat treatment — hardening, tempering, annealing, stress relief and demagnetisation of production parts, plus bulk heat treatment of dies — and slow-wire EDM, passivation, electropolishing, plating, phosphating and painting. Machining, grinding, medium and fast wire EDM, tapping and welding of tooling run in-house, and a small furnace is kept on site for emergency die repairs.
Can I visit the workshop or see the equipment?
Yes. Equipment lists, tool room photos and — for qualified projects — factory visits or video walkthroughs of the press line and tool room can be arranged through the contact form.
What inspection equipment do you use?
A 2.5D optical measuring projector, an instant vision measuring system, a digital height gauge with 0.001 mm resolution, a portable surface roughness tester, a Rockwell hardness tester and a model 20 salt spray chamber, supported by outside micrometers, three-point bore micrometers, inside caliper gauges, plug and go-no-go gauges and a concentricity gauge.
Tell us the part, we will tell you which machine it runs on
Send the drawing with material, tolerance and annual volume and we will come back with the press, tooling route and estimated capacity for your project.
Send your drawing for a DFM reviewMeasuring and inspection equipment in detail
The instruments listed above are covered individually, with photographs and what each one is used for, on the inspection lab page.
Metrology detail, and which tolerances a drawn housing can hold, are covered under housing tolerances.
Prototype and short-run work uses the smaller end of the press range — see how single-operation tooling is used for prototyping.