CNC Machining Services China
CNC Milling Services
CNC milling for plates, blocks, housings, brackets and multi-surface metal parts with pockets, slots, holes and contoured profiles. From DFM review and prototypes through repeat production.
Direct answer: CNC milling is used for prismatic and multi-surface metal parts: plates, blocks, housings, brackets and tooling components with pockets, slots, holes and profiles. Balford reviews datum structure, tool access, internal corner radii, workholding and setup count before quoting a prototype-to-production route, and combines milling with turning or wire EDM where the part requires it.
Typical Milled Parts
Plates & blocks
Faces, holes and profiles with flatness and positional control.
Housings & brackets
Multi-surface parts with pockets, slots and mounting features.
Tooling components
Fixtures, jigs and inserts machined to controlled drawings.
Multi-surface parts
Features on several faces with a clear setup and datum plan.
Milling DFM Checklist
- Datum structure defined before tolerances are placed
- Internal corner radius vs. cutter reach
- Pocket depth vs. wall thickness
- Tool access for deep or angled features
- Workholding and clamping without distortion
- Setup count and datum continuity
- Tight tolerances applied only where function requires
Milling vs. Wire EDM
Use this quick decision aid when routing a new part:
- Tool can reach the feature → CNC milling
- Sharp internal corner, narrow slot or hardened material → wire EDM
- Round or rotational geometry → CNC turning
- Large open surface with high stock removal → milling first, wire EDM only for the finishing contour
For drawing-level guidance see the CNC milling design guide.
Materials for Milled Parts
Aluminum
Plates, housings and brackets with good machinability. See aluminum milling.
Stainless steel
Corrosion-resistant milled parts; heat and work hardening managed with tooling strategy. See stainless steel milling.
Carbon and alloy steels
Structural parts and tooling components with controlled hardness. See carbon steel milling.
Special alloys and plastics
Evaluated per application with certification and stability confirmed. See special alloy milling.
Applications
Automotive and mobility
Housings, brackets and precision interfaces with tight positional tolerances. See automotive machining.
Industrial equipment
Machine housings, plates and replacement parts from controlled drawings. See industrial machining.
Fluid and valve systems
Milled sealing faces and interfaces on valve components. See solenoid valve components.
Sensor and motor products
Milled features on housings for sensors and motors. See sensor housings and motor housings.
Related Case Studies
Selected milling-related projects from Balford’s production history; each case shows the machining step inside a full route.

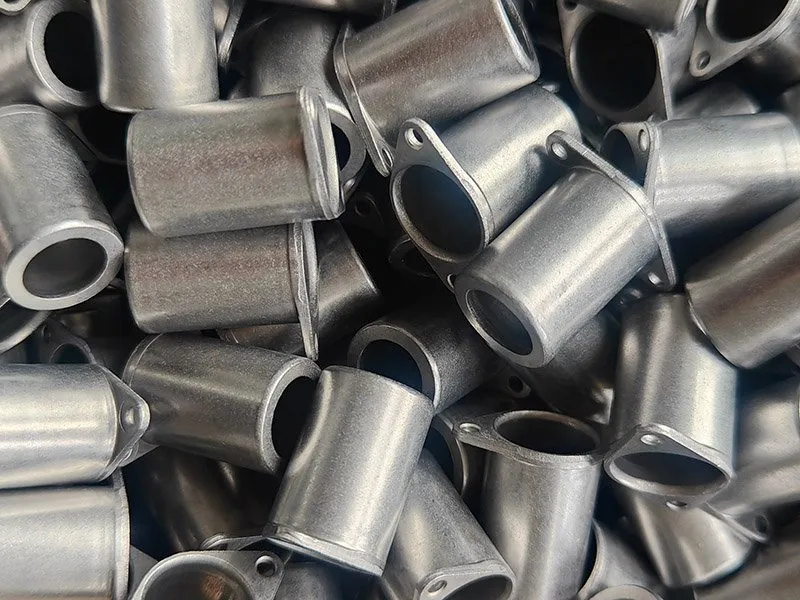

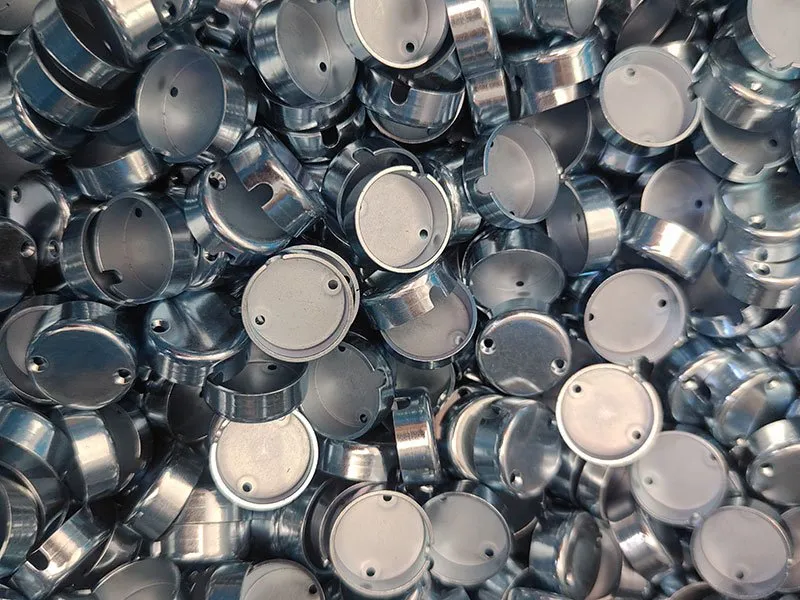
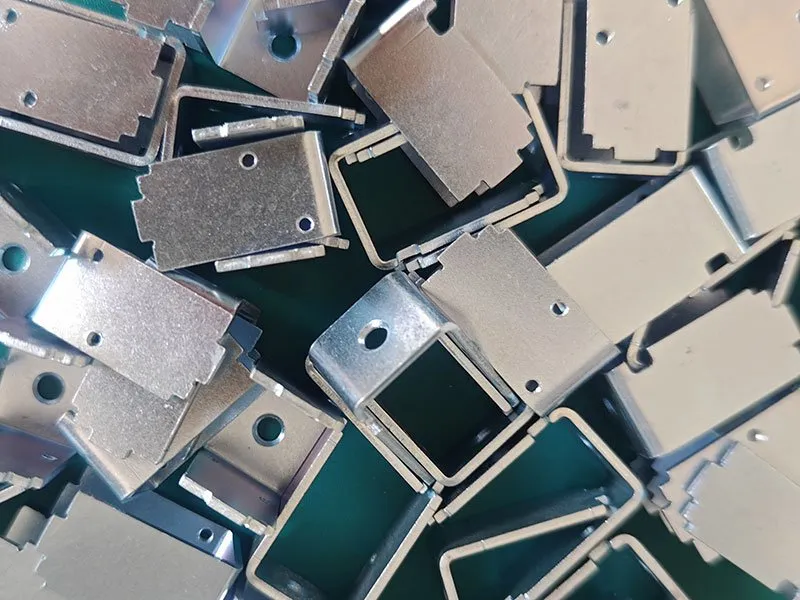
Browse the full case study library →
Compliance and Quality
- Automotive material compliance — IMDS, REACH, RoHS and GADSL for automotive programs.
- Balford IMDS process — material data from quotation to delivery.
- IMDS compliance checklist — 15 steps for automotive suppliers.
- Quality and certifications — ISO 9001:2015 and IATF 16949-aligned controls.
Frequently Asked Questions
What parts are best for CNC milling?
Prismatic parts: plates, blocks, housings, brackets, tooling components and multi-surface parts requiring pockets, slots, holes, faces or contoured profiles. If most features are on flat or orthogonal surfaces and need a rotating cutter, milling is the natural route.
What is the practical limit on internal corner radii?
A standard rotating cutter leaves a radius equal to its own. Deep pockets and small corners may need smaller tools (and therefore more passes) or a secondary process such as wire EDM for truly sharp corners. We review corner radius against function during DFM.
How do you control flatness and multi-setup accuracy?
Datum structure is defined first, then workholding (soft jaws or dedicated fixtures) keeps critical relationships in one setup where possible. Where a second setup is unavoidable, features are located from the same datums and verified with in-process inspection.
Can you machine thin walls?
Yes, within limits that depend on material, wall height and finish. We review wall thickness versus height early, because thin walls can deflect under cutting force; stock support and toolpath strategy are planned accordingly.
Which materials do you mill?
Aluminum, carbon and alloy steels, stainless steels, copper and brass, and selected engineering plastics and special alloys. Hardness and stock form are confirmed per project.
How do you combine milling with turning or stamping?
Rotational features can be added to a milled part by turning or live tooling; stamped or deep-drawn blanks can be milled where the forming process cannot hold an interface. The route is reviewed as one sequence so datum and setup stay consistent.
Secure Project Review
Send Balford Your Drawing
NDA before detailed file exchange. Drawing-based DFM review. Prototype-to-production route. Check the RFQ checklist before sending files.
Die plates and tooling components are machined in the same plant by the in-house tool room behind Balford’s dies.
Die plates and tooling components listed here are machined in the same plant — see the full equipment list.