Deep Drawn Stamping vs. Progressive Die Stamping: Process Selection for Precision Metal Components
Summary
Deep drawn stamping and progressive die stamping address fundamentally different manufacturing requirements. Deep drawing is the right choice for seamless, hollow components where wall thickness stays uniform and part depth exceeds diameter. Progressive die stamping is built for high-volume runs of flat or contoured parts, with features added sequentially as strip stock advances through the die. Your process choice directly affects part quality, tooling investment, scrap rates, and cycle efficiency. The deciding factor comes down to geometry—deep parts need controlled material flow; progressive dies handle multi-feature parts in one pass on coil-fed material.
What Is Deep Drawn Stamping
Deep drawn stamping is a metal forming process where a flat blank is pulled radially into a die cavity by a punch, producing a seamless, hollow part. The defining spec: the formed depth exceeds the part's diameter, which forces the material to flow rather than just bend.
The process runs through multiple stages, or draw reductions, to avoid tearing or wrinkling. Each pass works the material closer to final geometry while you manage thinning and work hardening. The metal behaves like a viscous fluid, giving you consistent wall thickness across the entire part—something you can't get with welded or multi-piece assemblies.
Advantages of Deep Drawing
Seamless Construction: Parts come off the press with no weld joints, seams, or fastener points. That's a critical requirement for fluid transfer components, pressure vessels, and housings where structural integrity is non-negotiable.
Uniform Wall Thickness: Deep drawing's material flow characteristics yield parts with consistent wall thickness and mechanical properties across the entire geometry.: The material flow characteristics of deep drawing produce parts with consistent wall thickness and mechanical properties throughout.
Complex Geometries: Produces deep, hollow shapes with intricate features that other methods can't handle efficiently—think multi-cavity housings or stepped cups.Complex GeometriesWork Hardening Benefits: Plastic deformation during the draw increases tensile strength, so finished parts deliver better strength-to-weight ratios than the original flat sheet.
Smooth Surface Finish: Drawn surfaces show fewer tool marks and interruptions than progressive stamping, making this process a solid pick for visible parts or any application where cosmetics matter.: Plastic deformation during drawing increases tensile strength, giving finished parts better strength-to-weight ratios than the flat sheet they originated from.
Limitations of Deep DrawingSmooth Surface FinishHigher Tooling Costs: Deep draw dies are more complex and pricier to build than progressive stamping tooling, especially when you're staging multiple draws.
Slower Production Speeds: Runs at moderate cycle rates versus progressive stamping, because you're dealing with multiple forming stages and controlled material flow.
Material Constraints: Needs highly ductile metals with elongation above 30% and yield-to-tensile ratios under 0.65. Brittle materials or high-strength alloys won't work without intermediate annealing steps.: Deep drawing dies are more complex and expensive to produce than progressive stamping tooling, particularly for multi-stage draws.
Specialized Equipment: Requires press and tooling setups specific to deep drawing, which limits the pool of shops that can actually run the process.Slower Production SpeedsCommon Defects in Deep Drawing
Material ConstraintsThinning: Predictable wall thickness reduction that you control by getting the draw reduction sequence right.
Wrinkling: Shows up when blank holder pressure is too low or draw ratios are off.: Requires presses and tooling configurations specific to deep drawing, limiting the number of factories capable of performing the process.
Earing: Driven by grain direction in the material relative to how you orient the blank.Common Defects in Deep Drawing
Tearing- Thinning: Predictable wall thickness reduction that must be controlled through proper draw reduction sequence
- Wrinkling: Caused by insufficient blank holder pressure or incorrect draw ratios
- Earing: Driven by material grain direction relative to the blank orientation
- Tearing: This happens when the total draw reduction exceeds what the material can handle, causing the metal to thin out or split at the draw radius.
What Is Progressive Die Stamping?

Progressive die stamping is a high-speed process where a continuous metal strip runs through a single tool with multiple stations. Each station performs a specific operation—blanking, piercing, bending, embossing, coining, or forming—so the part builds up step by step, and at the final station it's cut free from the carrier strip. die stamping is a high-speed manufacturing process where a strip of metal is fed through multiple stations within a single tool. Each station performs one or more operations—blanking, piercing, bending, embossing, coining, or forming—until a finished part emerges at the final station, where it is cut free from the carrier strip.
The key is precise strip advancement, usually controlled by pilots that locate into previously pierced holes to hold alignment within a few thousandths of an inch.The process relies on precise strip advancement, typically guided by pilots that engage previously pierced holes to ensure alignment within thousandths of an inch.
Advantages of Progressive Die StampingAdvantages of Progressive Die Stamping
High-Speed Production: For simple geometries, you can run at 800 parts per minute or more, which is hard to beat on volume.High-Speed ProductionCost Efficiency at Volume: Once the tooling is paid off, the per-part cost is substantially lower than deep drawing for parts that fit the process.
Complex Feature Combinations: You can build holes, bends, forms, and embossing into one tool, so you're not sending parts out for secondary work.: Once tooling is amortized, per-part costs are significantly lower than deep drawing for compatible geometries.
Lower Tooling Investment: For shallow parts, a progressive die typically costs less than multi-stage deep draw tooling.Complex Feature CombinationsConsistent Quality: With automated strip guidance and in-die sensors, you get repeatable results across long runs without constant operator intervention.
Limitations of Progressive Die Stamping: Progressive dies generally cost less than multi-stage deep draw tooling for parts with shallow features.
Depth Limitation: The practical limit for drawing in a progressive die is about 1.5 times the part diameter. Beyond that, the carrier strip can't feed enough material into the forming station, so you get thinning, tearing, or distortion.Consistent QualityCarrier Tab Witness Marks: Every part will have small marks where it broke off the strip. If you've got a cosmetic surface, those marks need to be hidden or you'll need a secondary finishing step.
Station Marks: The multiple forming stations can leave visible witness lines on the part surface, which may be a concern for exposed areas.
Depth Limitation: The general industry limit for progressive die drawing is approximately 1.5 times the part diameter. Beyond this ratio, the carrier strip connection starves the forming station of material, causing thinning, tearing, and distortion.
Carrier Tab Witness Marks: Each part carries small marks where it separated from the carrier strip. For decorative faces, these marks must be positioned away from view or require secondary finishing.
Station Marks: Multiple forming stations can leave visual witness marks on the part surface.
Material Restriction: Parts stay attached to the strip during forming, so operations that require the part to be free—like beading, necking, flange curling, or thread rolling—are not feasible in a progressive die.
Reduced Design Flexibility: Changing the part geometry usually means cutting new tooling, which adds both cost and lead time compared to the more iterative approach possible with deep draw tooling.
Common Defects in Progressive Stamping
- Burrs: Typically from worn punch edges or die clearance that's too generous for the material thickness.
- Misfeeds: Happen when strip alignment drifts, often due to pilot wear or improper feed timing.
- Distortion: Shows up when sequential forming steps build up internal stress without a relief station to control it.
Key Differences Comparison
| Feature | Deep Drawn Stamping | Progressive Die Stamping |
|---|---|---|
| Part Depth | Can exceed part diameter; deep, hollow geometries are standard | Shallow or contoured profiles; depth typically under 1.5× diameter |
| Production Speed | Moderate—each draw stage adds cycle time | High—up to 800+ parts per minute from coil-fed presses |
| Tooling Cost | High—complex multi-stage draw dies | Moderate to high—depends on feature count and station complexity |
| Wall Thickness | Uniform, with consistent mechanical properties throughout | Variable—thinning can occur at bends or formed features |
| Material Suitability | Ductile, formable alloys like aluminum, stainless, and copper | Broad range, including harder grades and pre-tempered materials |
| Seamless Construction | Yes—no joints or seams | No—features sequential forming |
| Surface Finish | Smooth, minimal tool marks | May have carrier tab marks, station marks |
| Application Fit | Housings, enclosures, fluid components, pressure vessels | Brackets, clips, connectors, multi-feature components |
| Scrap Rate | Lower when properly staged | Can be higher due to carrier strip waste |
| Design Flexibility | Greater for iterative changes | Limited after tooling is committed |
Applications by Industry
Deep Drawn Stamping Applications
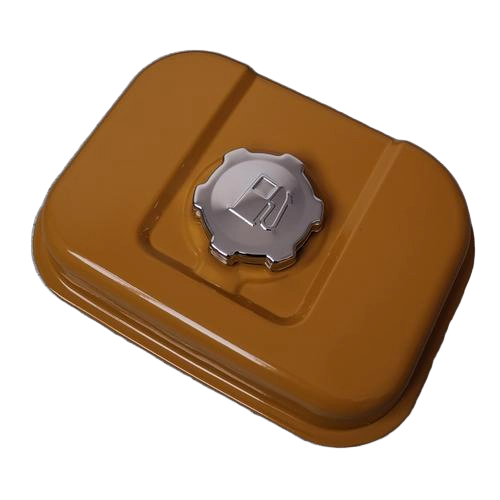
Automotive: Fuel tanks, EV battery housings, brake system components, structural parts exposed to pressure or vibration.: Fuel tanks, EV battery housings, brake system components, structural parts exposed to pressure or vibration.
Medical DevicesAerospace: Fuel system components, airframe parts, applications requiring strength-to-weight optimization.
Consumer Goods: Beverage cans, kitchen sinks, appliance housings requiring cosmetic finishes.: Fuel system components, airframe parts, applications requiring strength-to-weight optimization.
Fluid Systems: Hydraulic components, fluid transfer parts, pressure vessels.Consumer GoodsProgressive Die Stamping Applications
Automotive: Brackets, clips, fasteners, multi-feature stamped components with stable, high annual usage.: Hydraulic components, fluid transfer parts, pressure vessels.
Progressive Die Stamping Applications
Automotive: Brackets, clips, fasteners, multi-feature stamped components with stable, high annual usage.
Electronics: Connector shells, EMI shields, and precision components for consumer electronics—tight tolerances and consistent surface finish are standard here.: Connector shells, EMI shields, precision components for consumer electronics.
Industrial: Hardware, panels, and components that need piercing, bending, and forming in a single tool pass—ideal for high-volume runs where repeatability matters.IndustrialAerospace: Structural brackets and standard hardware items, with material certifications and traceability handled per your spec.
AerospaceDesign for Stamping: Critical Considerations
When to Select Deep Drawing
Design for Stamping: Critical Considerations
Part depth exceeds 1.5 times the diameter
- Seamless, hollow geometry is required
- Part depth exceeds 1.5 times the diameter Uniform wall thickness is critical
- Seamless, hollow geometry required Application demands pressure or fluid integrity
- Uniform wall thickness is critical Cosmetic finish is important
- Application demands pressure or fluid integrity
- When to Select Progressive Die Stamping
Part features are flat or slightly contoured
- Depth is less than 1.5 times the diameter
- Part features are flat or slightly contoured Multiple features (piercing, bending, embossing) are required
- Depth is less than 1.5 times the diameter Production volume is very high
- Multiple features (piercing, bending, embossing) are required Tooling cost must be minimized
- Production volume is very high
- Tooling cost must be minimized
General Design Principles
Material Selection: For deep drawing, you need materials with high anisotropy (r-value above 1.6) and elongation over 30%. Low yield-to-tensile strength ratios—below 0.65—give you the best formability and reduce cracking risk.: Deep drawing requires materials with high anisotropy (r-value above 1.6) and elongation above 30%. Materials with low yield-to-tensile strength ratios (below 0.65) perform best.
Punch and Die Radii: In deep draw tooling, the die entry radius should be 4 to 10 times the material thickness. This controls material flow into the cavity and minimizes stress concentration at the bend line.Punch and Die RadiiDraw Reduction Planning: You have to respect the material's limits at each draw stage. Over-aggressive reductions will tear the part; under-reducing adds cost because you're running extra stages you don't need.
Lubrication Strategy: Deep drawing depends on effective lubrication to drop the coefficient of friction from around 0.15 down to 0.05. That alone can cut punch load requirements by up to 30%, which extends tool life and improves part consistency.: Respect material limits for each draw stage. Aggressive reductions cause tearing; insufficient reductions increase cost through additional stages.
Tolerance Considerations: Progressive stamping can hold tight tolerances, but you've got to account for springback and tool wear over the run. Deep drawing gives you consistent dimensional accuracy, but the die design has to manage wall thinning carefully to stay in spec.Lubrication StrategyIndustry Standards: Reference ISO 2768 for general tolerance guidance. If you're in automotive, medical, or aerospace, you'll typically need a quality management system certification like IATF 16949 or ISO 13485 to meet customer requirements.
Tolerance ConsiderationsFAQ
What is the difference between deep drawing and progressive stamping?: Reference ISO 2768 for general tolerance guidance. Regulated industries (automotive, medical, aerospace) typically require specific quality management system certification.
Deep drawing is a metal forming process that produces seamless, hollow parts—depth exceeds diameter—by pulling material into a die cavity. Progressive stamping is a high-speed process where a coil-fed strip moves through multiple stations, each doing a specific operation like blanking, piercing, or forming, to make flat or contoured parts. The key difference is part depth: deep drawing gives you deep, hollow shapes, while progressive stamping is for shallow or contoured designs.Which process is better for deep, cylindrical parts?
Deep drawing is the right choice for deep, cylindrical parts. As a rule of thumb, if part depth exceeds about 1.5 times the diameter, a progressive die will struggle—the carrier strip restricts material flow, causing tearing and distortion. Deep drawing lets the blank move freely, pulling metal into the cavity through staged reductions, so you get a clean, consistent part.
What is the limiting draw ratio in deep drawing?
The limiting draw ratio (LDR) is the maximum blank diameter to punch diameter ratio you can achieve in a single draw operation without failure. For most ductile metals, LDR runs between 1.8 and 2.3 in one hit. If you need deeper parts, you're looking at multiple draw stages with intermediate annealing to restore formability.
Does deep drawing cost more than stamping?
Deep drawing typically has higher upfront tooling costs because the dies are more complex and you need specialized press equipment. But for the right geometry, deep drawing can be more cost-effective at production volumes once you factor in scrap rate, secondary operations, and part performance. Forcing deep parts through progressive stamping can push scrap rates to 40%, which quickly eats up any tooling savings.
The limiting draw ratio (LDR) is the maximum blank diameter to punch diameter ratio achievable in a single drawing operation without failure. For most ductile metals, LDR ranges from 1.8 to 2.3 in a single operation. Parts requiring deeper draws need multiple stages with intermediate annealing.
Does deep drawing cost more than stamping?
Deep drawing typically has higher initial tooling costs due to more complex dies and specialized equipment. However, for compatible geometries, deep drawing can produce parts more cost-effectively at production volumes when factors like scrap rate, secondary operations, and part performance are accounted for. Forcing deep parts through progressive stamping can cause 40% scrap rates, eroding any tooling savings.
What grades of material work best for deep drawing?
Deep drawing calls for metals with good ductility and formability. We typically run aluminum 1100 or 3003, 300-series stainless, copper alloys, low-carbon steel, plus select titanium and nickel grades. You want elongation above 30% and a low yield-to-tensile ratio—that keeps the material flowing evenly through the die without splitting or wrinkling.
How does the process choice affect surface finish?
Deep drawing gives you a smoother finish with fewer tool marks, which is why it's the go-to for visible housings and cosmetic parts. Progressive stamping leaves clean sheared edges, but you'll see carrier tab marks and station witness lines. If the part has a decorative face, we plan the tab location off the visible surface or add a secondary operation to clean it up.
Which process gives you higher throughput on large volumes?
Progressive stamping wins on speed—simple geometries can run over 800 parts per minute on a coil-fed press. Deep drawing is slower, typically 15 to 40 strokes per minute, because each stage controls material flow to avoid thinning or tearing. That's the trade-off: speed versus depth of form.