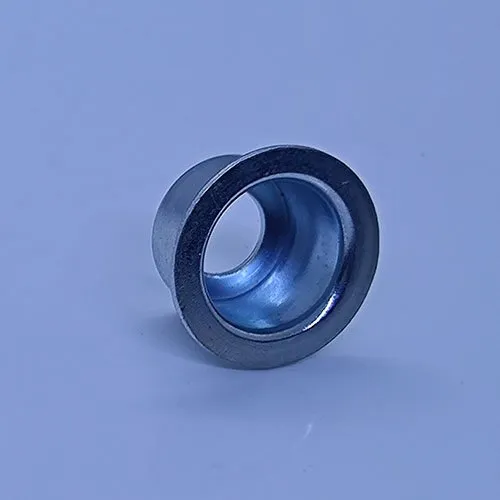
Valve Spring Seat – AISI 1045 Steel
What is this part? Valve Spring Seat is a Spring Seat manufactured from AISI 1045 steel by Balford. Production process: Deep Drawing → Heat Treatment → Surface Treatment. Finish: Zinc plating, applied after Annealing (mesh belt furnace, between hits). Key requirements: Deep drawing of medium-carbon AISI 1045 with inter-hit annealing to keep the material workable and hold cycle time and cost.
Deep Draw Metal Stamping
| Product Name | Valve Spring Seat |
|---|---|
| Category | Spring Seat |
| Process Flow | Deep Drawing→Heat Treatment→Surface Treatment |
| Material | AISI 1045 steel |
| Surface Treatment | Zinc plating |
| Heat Treatment | Annealing (mesh belt furnace, between hits) |
| Key requirements | Deep drawing of medium-carbon AISI 1045 with inter-hit annealing to keep the material workable and hold cycle time and cost |
Case Review
Saintbon Hydraulic and Hengli Hydraulic came to us with a valve spring seat job in AISI 1045 steel, specifying the deep drawing process for the part. We've run spring seats for two customers before. They asked for deep drawing on this part, even though AISI 1045 is a medium-carbon steel that doesn't typically lend itself to that kind of forming. Our edge is the mesh belt annealing furnace on the floor. When deep drawing gets marginal on a hard grade like this, we anneal between hits to keep the material workable. That lets us simplify the tooling sequence, hold better cycle times, and keep the per-part cost down. Their old route was cutting round bar and machining the whole seat from solid—slow and wasteful on material. Switching to deep draw stamping cut our raw material consumption and trimmed processing time significantly. The part also comes out with better strength and ductility, and we can hold tighter production schedules.