Temperature Sensor Housings for Coolant and Battery Thermal Management
A temperature sensor housing is the metal shell that holds the sensing element and seals it against the medium it measures — engine coolant in a combustion vehicle, or battery coolant in an electric one. Balford draws copper temperature sensor housings in multi-stage progressive dies: blank, draw, redraw, bore and trim run in one continuous tool, so the wall is formed without a longitudinal weld.
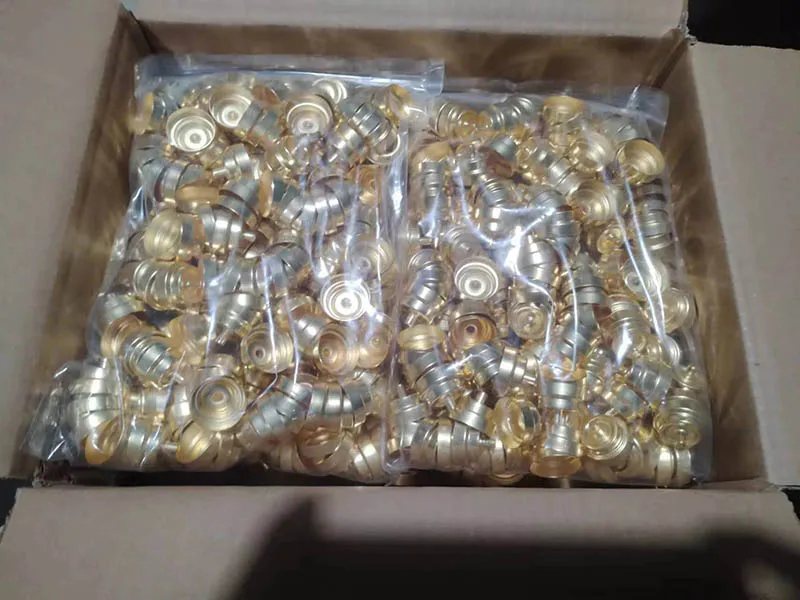
Where the Same Housing Ends Up: Two Coolant Circuits
The part looks similar in both cases, but the application decides the material, wall thickness and sealing method.
| Combustion coolant circuit | Battery thermal management loop | |
|---|---|---|
| What it measures | Engine coolant temperature | Battery coolant temperature, pack inlet and outlet |
| Typical location | Cylinder head, thermostat housing, radiator hose | Battery coolant plate, heat exchanger, chiller inlet and outlet |
| Signal use | Fuel and ignition correction, fan control, gauge | Cell temperature control, charge and discharge limits |
| Housings per vehicle | Usually one | Commonly two or more |
| Extra demand on the part | Coolant compatibility, thermal cycling | Wider temperature range, tighter sealing, faster response |
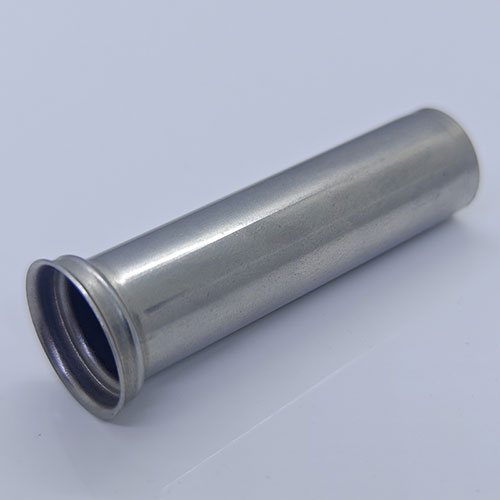
Progressive Die Drawing, on Tooling We Own
The twelve copper housings in our record were developed with a European engine-management customer: the drawing came from them, the progressive dies came from our toolroom to that drawing. The design belongs to the customer; the tooling is Balford's own investment.
Because we fund the die, the piece price does not carry tooling amortisation, and there is no third-party die owner to negotiate with before we quote. And because a die is built for one customer's part, it runs that part only — we do not produce a customer's part for anyone else, and we do not offer a customer's design to a second buyer.
Multiple drawing stages in one tool matter for copper: the material work-hardens quickly, so the reduction per stage has to be balanced against annealing between stages. Running the stages in a progressive die keeps the wall thickness consistent from part to part and avoids the handling damage that comes from moving soft copper between separate presses.
- Stages in one tool: blank → draw → redraw → bore → trim, controlled by pitch and strip feed in the die
- Wall thickness typically 0.8–3.0 mm; the drawing must state where the wall is measured, because it is a gradient along the height
- Presses 25–350 t; maximum draw diameter Ø250 mm; 4,000+ single-action draw dies built since 2000
- Dies designed and built in our own toolroom, financed by Balford
What We Have Actually Made
- Seven sensor families: oxygen, nitrogen-oxide (NOx), exhaust gas temperature, crankshaft, ABS wheel speed, coolant temperature and motorcycle sensors
- 115 housing and stamped part numbers in total
- 10 vehicle platforms across Europe and North America (7 European, 3 North American)
- Applications confirmed for both combustion coolant circuits and battery thermal management loops
What Changes for Battery Thermal Management Parts
Battery-loop housings face requirements that combustion parts usually do not: a wider working temperature range, coolant compatibility including glycol-water mixtures, tighter sealing at the sensor joint, and faster response. These push the design toward thinner walls, tighter bore concentricity and a defined sealing surface. We review the sealing geometry, the wall thickness measurement position and the material before quoting, because a housing that passes a combustion duty cycle can still fail on a battery loop.
Materials
Copper and brass are the first choice for temperature sensor housings: high thermal conductivity gives a faster response, and both resist the glycol-water coolant used in engine and battery loops. Depending on the duty cycle we also form the same housing geometry in carbon steel (10#), pure iron for magnetic or fast-response assemblies, and stainless steel 304 for aggressive coolants. Batch heat treatment, palladium passivation, electroplating, phosphating and powder coating are carried out by audited subcontractors with traceable process records; drawing, forming, machining, brazing, assembly and inspection are in-house.
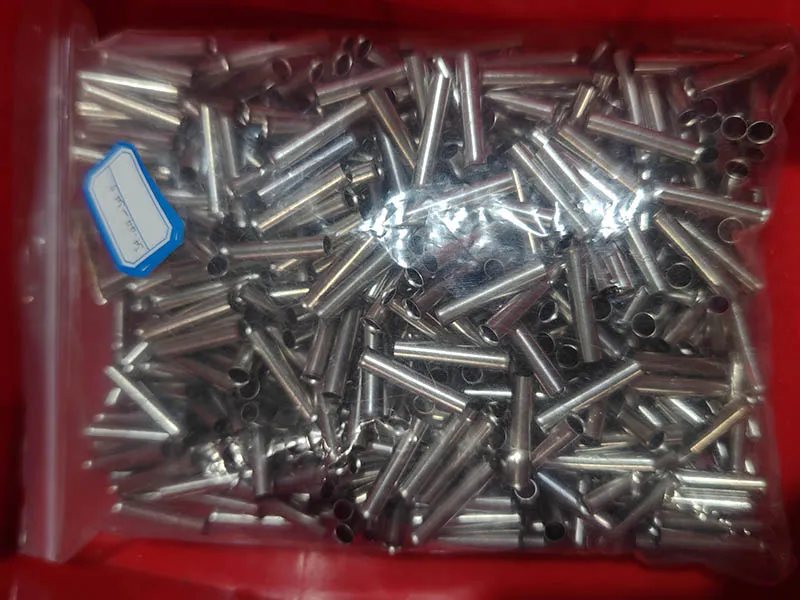
Temperature sensor housings by series
| Series / application | What it carries | Material we run | Wall |
|---|---|---|---|
| Coolant circuit housing | Engine coolant, glycol-water mixture | Copper C11000, drawn in a progressive die | 0.8–3.0 mm |
| Battery thermal management housing | Battery loop coolant, glycol-water mixture | Copper C11000, drawn; thinner walls and tighter bore concentricity than a combustion part | 0.8–3.0 mm |
| Retaining shell or stamped housing | Structural surround for the sensing element | DC04 or stainless strip, progressive die | to drawing |
| Threaded fitting or port on the same assembly | Sensor seat and thread | 304 / 430F stainless, turned | to drawing |
Twelve copper housings in our record were built for a European engine-management customer, and the same housing designs are confirmed for both combustion coolant circuits and battery thermal management loops.
By material
| Material | Why it is chosen | How we make it |
|---|---|---|
| Copper C11000 | Thermal conductivity first: the housing has to move heat to the sensing element quickly | Progressive die drawing, stages in one tool |
| 304 stainless | Coolant-side corrosion resistance, and a non-magnetic part for the assembly | Drawn or machined, depending on geometry |
| 430F stainless | Machinability where the part is turned rather than drawn | CNC turning from bar |
| PTFE (bought out) | Insulation and sealing where the part must not conduct | Purchased and supplied fitted |
Two questions come up whenever the material is discussed: whether the part is magnetic, and how it behaves in service — see what happens to copper over time and when stainless stains or pits.
By connection and finish
| Feature | Options we quote | Note |
|---|---|---|
| Connection | Threaded port (M12 to M27), smooth bore for a pressed-in element, flanged with mounting holes | The thread and the bore are produced from the same datum |
| Sealing face | Machined seat, chamfered lead-in, flat face for a gasket or O-ring | State the sealing method on the drawing; it drives the surface and the concentricity callout |
| As drawn copper | Bare copper, tarnish accepted | Normal for a housing whose outside is not a cosmetic surface |
| Plated or passivated | Zinc, nickel or passivation | Subcontracted; specified where contact resistance or appearance matters |
| Powder coated | RAL colour | In house for parts that fit our booth, with an external line for oversize work |
Frequently Asked Questions
What do you need to quote a sensor housing?
Drawing with the wall thickness measurement position marked, material, bore and thread tolerance, sealing method and annual volume. We return a DFM review before the price.
Can you supply both combustion and battery-loop versions from one drawing?
Usually yes, but the battery version is re-reviewed: wall thickness, sealing surface and material may change even when the outline does not.
How is wall thickness controlled on a drawn housing?
Wall thickness in a drawn part is a gradient along the height. The drawing must state where it is measured; we control it by die clearance and the number of drawing stages.
What is your capacity?
4,000+ single-action draw dies built since 2000, 500+ machines, 120+ engineering and production staff, approximately 50 million parts per year.
Related: sensor housings overview, deep drawn metal stamping, deep drawn sensor housings, pure iron, stainless steel.
Send your drawing for a DFM review before quoting → All Balford catalogues and data files are collected on the downloads page.
Automotive Sensor Hex Nuts & Plastic Accessories — product range, materials and dimensions (PDF)