Summary
On a deep drawn housing, coating thickness is a dimensional decision before it is a corrosion decision: plating adds material to the ID and the OD at the same time, so a two-sided coating spends twice its thickness out of any diametral tolerance band. Choose the thickness the drawing can absorb, sequence plating against joining, and treat salt-spray hours as the negotiated outcome rather than the starting point.
Plating thickness is a dimensional variable, not a finish choice
On a machined part, coating thickness is usually a rounding error against a tolerance of a tenth of a millimetre. On a deep drawn housing the relationship is different. The wall is thin, the features are drawn rather than cut, and the tolerance band on a bore or a mounting hole is often the same order of magnitude as the coating itself. Ten micrometres of zinc on a bore does not sit alongside the tolerance band — it consumes part of it.
That is why the order of decisions matters. Buyers normally open with the corrosion target, carry a salt-spray figure over from an earlier project, and ask what thickness will deliver it. The reliable order is the reverse: establish what the tolerance budget can absorb, find the coating system that reaches the corrosion number inside that budget, then check whether the geometry is platable.
Two cases show what getting that order wrong costs. A change from a zinc-nickel scheme at 8–13 µm to one at 80 µm and above is not a process tweak on a drawn shell; it moved the square-nut mounting hole dimensions far enough that the die had to be modified. Separately, over-thick zinc pushed an entire 150-piece lot outside tolerance and the lot was scrapped. Neither was a plating failure; both were dimensional failures caused by the coating.
The arithmetic: a coating on a bore costs twice its thickness
Every diametral feature moves by two coating thicknesses, because plating grows from both sides of the diameter. A bore measuring D before plating measures D minus 2t afterwards. An outside diameter measures D plus 2t. Wall thickness gains 2t. Only a masked, single-sided surface behaves as a one-to-one addition, and masking adds handling cost and coverage gaps.
Take a bore called out as ±0.05 mm. First settle whether that means a 0.05 mm or a 0.10 mm total band, because the answer changes the argument completely. On the tighter reading the band is 50 µm wide. A 10 µm coating removes 2 × 10 = 20 µm from the finished bore — 40% of the band, spent before the die has contributed anything. At 80 µm the same arithmetic removes 160 µm, more than three times the band. No tooling skill recovers that; the drawing is unbuildable as written.
| Feature as drawn | Tolerance band | 10 µm coating | 40 µm coating | 80 µm coating |
|---|---|---|---|---|
| Bore Ø12, band read as 0.05 mm | 50 µm | 20 µm — 40% of band | 80 µm — band exceeded | 160 µm — unbuildable |
| Bore Ø12, band read as 0.10 mm | 100 µm | 20% of band | 80% of band | 160% — unbuildable |
| Mounting hole Ø6, 0.10 mm band | 100 µm | 20% of band | 80% of band | fails |
| Outside diameter Ø30, 0.10 mm band | 100 µm | 20% of band | 80% of band | fails |
| Wall thickness 1.00 mm, ±0.03 mm | 60 µm | 20 µm added — 33% | 80 µm added — fails | fails |
Read that as a budget rather than a verdict. Where the coating takes 20% of the band, the die still has 80% to work with and the part is normally safe. Where it takes 80%, the die must sit in the middle of the band and hold it. The drawing may also need pre-compensation: the as-drawn bore is deliberately made oversize by 2t so the plated bore lands inside the band. That only works if the thickness is controlled within a range, not held to a nominal.
Choosing a coating system against the tolerance budget
The table follows the way the decision is actually made: start from the thickness the tolerance can absorb, then read across to what that thickness is worth in salt-spray hours. Treat the hours as ranges to confirm on the actual geometry, not as guaranteed values — the same coating behaves differently on a flat panel and inside a drawn recess. The finishing routes we run in-house are listed under surface treatment.
| Coating system | Typical thickness per surface | Salt-spray hours typically quoted | Diametral loss (2 × t) | Where it fits |
|---|---|---|---|---|
| Barrel zinc, clear or blue passivate | 5–8 µm | 24 h; 48–72 h with passivate or e-coat | 10–16 µm | 0.10 mm bands and wider; appearance secondary |
| Conventional zinc, barrel or rack | 8–13 µm | about 140 h without a sealer | 16–26 µm | General housings, comfortable band |
| Zinc plus e-coat | zinc 5–8 µm + e-coat 15–25 µm | 48 h for the e-coat scheme | zinc 10–16 µm + 30–50 µm | Cosmetic black plus corrosion resistance |
| Zinc-nickel, 12–15% nickel | 8–13 µm | 240 h target; 500 h+ with a sealer | 16–26 µm | Tight bands, high corrosion target |
| Zinc-nickel, heavy deposit | 80 µm and above | not quoted as a salt-spray advantage | 160 µm and above | Almost never viable on a drawn shell |
| Zinc-phosphate | 2–5 µm | fails before 240 h internally | 4–10 µm | Paint pre-treatment only |
| Zinc plus powder coat over assembly | zinc 8 µm + 60–100 µm powder | 500 h+ achievable | coated faces only | Sealed assemblies; mask threads |
Two things follow. A 5 µm zinc-nickel scheme is not simply a cheaper 15 µm one; it is a different tolerance proposition in a different band. And the large jumps in salt-spray hours come from a sealer or a topcoat, not from adding zinc — and higher hours are claimed for zinc-nickel at low thickness, which is worth questioning.
Salt-spray hours are the currency, and the ladder is steep
Salt-spray hours function as the negotiating unit between buyer and supplier. They are quoted, traded and occasionally trimmed to reach a target, and the ladder in real use is wide: 24 h basic, 48 h where an e-coat is specified, 72 h for a mid-tier project, around 140 h for conventional zinc without a sealer, about 240 h for a zinc-nickel target, and 500 h and above with a sealer.
- Do not accept a thickness reduction on a verbal assurance that the salt spray will still pass. Ask for the report on the same geometry, coating and sealer state.
- Ask whether the quoted hours include a sealer. That one word moves the result from roughly 140 h to 500 h and changes the joining options.
- Establish whether the figure applies to a visible outer face or an internal surface. On a deep drawn cap they are not the same result.
A salt-spray report normally sits in the documentation package alongside PPAP, ISIR and material certificates — see our quality and certification scope — but it only means something if it names the thickness range and the sealer state it was run with.
The sealer trade: 500 hours that costs you the weld
The sealer deserves its own heading because it is the clearest example of a surface treatment decision that breaks something else. A bath with a sealer leaves a thin film over the zinc, and corrosion resistance improves by a large factor: a scheme that reached roughly 140 h without the sealer moved past 500 h with it. The same film destroyed weldability. Earth pins could no longer be welded to the housings, and the sealer had to come out of the specification. There was no partial version of the trade. List every joining and contacting operation on the part — welding, riveting, staking, press-fitting, crimping — before accepting a sealer, and check each one against the film.
Blind geometry: the surface a plating bath cannot reach
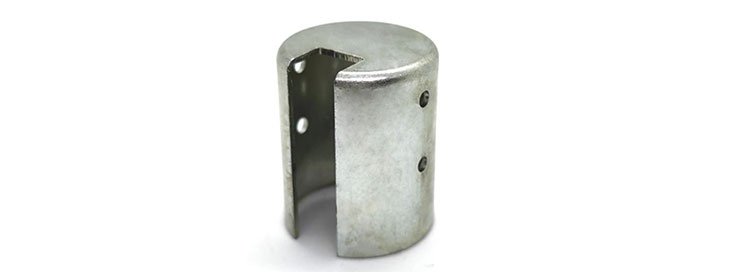
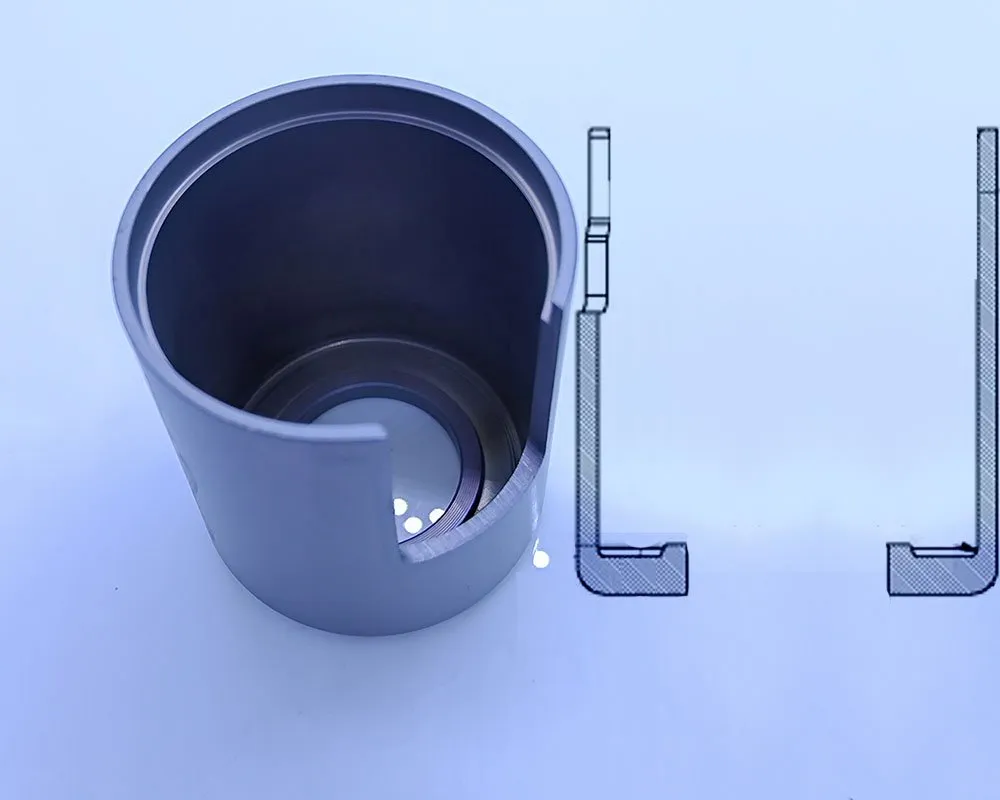
A deep drawn cap has an internal surface at the innermost end that the plating bath cannot reach reliably. The coating looks complete outside and is thin or absent at the deepest internal point. Under salt-spray testing the rust starts there and the part fails while the visible exterior is still intact. This is an intrinsic disadvantage of a one-piece drawn housing against a two-piece design that is plated and then assembled. The assembled route solves coverage but reintroduces two others: the joining operation damages the coating, and the extra operations cost more. The practical options are:
- Split the part. Plate the two halves separately and join afterwards, accepting that the joint needs its own protection or must not sit in a corrosion-critical zone.
- Mask selectively and treat the unreachable faces another way, accepting that masking adds handling and is not perfectly repeatable at volume.
- Powder coat over the assembly. Powder reaches some surfaces the bath does not, at the price of a thicker film and masked threads.
- Move the corrosion-critical surface out of the blind region, so the face that must survive 240 h or more is one the bath can see.
Sequence the surface treatment against the joining
Once a part carries both a joint and a coating, the order is a hard constraint: join then coat, or coat then join, but not both. Each order fails in a different way.
- Join then coat: plating reaches the exterior consistently but not into the crevice at the joint, and the crevice is exactly where a salt-spray test finds water. A staked or riveted interface left unplated becomes the initiation site.
- Coat then join: coverage is good on both parts before assembly, but riveting, staking or pressing breaks the layer locally and leaves a bare-steel path. Post-plating operations damaging the coating is an observed cause of salt-spray failure, not a theoretical risk.
Where a design needs both a sealed joint and 240 h or better, the workable sequence is usually to plate separately, join, then apply a final powder coat that bridges the joint and covers the damage. It is the most expensive route and should be chosen deliberately. The same question appears on deep drawn solenoid valve housings, where the joint, the seal face and the coating compete for the same real estate.
Specifying appearance without sending a reference part
Appearance causes more avoidable rework than any other line on a plating specification, because the usual words do not map onto a deposit. Blue-white and transparent bright describe a trivalent passivate with a slight iridescent cast; white zinc describes a flatter, more matte finish. A requirement written as anything other than white zinc leaves the plating shop to interpret, and the interpretation is frequently wrong. Name the finish by passivate type rather than colour word, and where colour matters send a physical reference part.
Rack or barrel plating: the cost spread you are choosing between
The spread matters as much as the average. A ±2 µm bath tolerance on a nominal 10 µm coating is a 4 µm swing, which becomes an 8 µm swing on a diameter — a meaningful share of a 50 µm band. Specify the range, not the nominal. Rack plating gives a more uniform deposit and a better appearance on visible faces; barrel plating tumbles parts in bulk, is faster and cheaper, but can leave contact marks and a wider thickness spread. Where the driver is anti-rust performance on a part that is not visible in service, barrel plating is often acceptable, and that choice belongs in the drawing pack rather than with the plating shop.
What to put on the drawing
Drawing note: All dimensions apply after plating. Zinc-nickel, 8–13 µm per surface, trivalent passivate, no sealer unless stated. Plating adds to both the ID and the OD: every diametral feature changes by twice the coating thickness, and every wall thickness increases by twice the coating thickness. Dimensions toleranced at 0.05 mm or tighter shall be identified as pre-plate or post-plate, and the as-drawn dimension shall be pre-compensated by 2t on all coated surfaces.
That note does three jobs. It fixes a thickness range instead of a nominal. It forces the pre-plate or post-plate question to be answered on the drawing rather than in a meeting. And it tells the die designer how much of the band is already spent. General dimensioning practice is covered in our engineering drawing guide, and the interaction between wall thinning, ironing and the tolerance left over for coating is set out in ironing tolerances and surface finish. Where the coating budget turns out to be the binding constraint, revisit the drawing before revisiting the plating specification; our note on capability boundaries sets out the limits we work within.
Related reading on deep drawn stamping
These companion notes go deeper on the same engineering decisions:
- Drawing Lines, Die Marks and Galling on Drawn Parts
- The Deep Drawing DFM Checklist Before Cutting Steel
- Interstage Annealing Distortion in Deep Drawn Parts
- Deep Drawn vs Welded Housing: Is It Actually Sealed?
FAQ: FAQ: plating thickness and tolerance on deep drawn housings
Q: Does a thicker zinc coating really change the dimensions of a drawn housing?
A: Yes, and by twice the thickness on any diametral feature. Plating grows from both sides, so a 10 µm coating removes 20 µm from a bore and adds 20 µm to an outside diameter. On a bore with a 0.05 mm total band that is 40% of the budget before the die has done anything, which is why an over-thick coating scrapped an entire lot rather than merely failing appearance.
Q: How many salt-spray hours should we specify for a plated deep drawn housing?
A: Specify the hours the application actually needs, not the highest figure available, because hours are bought with thickness and thickness is bought with tolerance. The ladder quoted in practice runs from 24 h basic, through 72 h and roughly 140 h for conventional zinc without a sealer, to about 240 h for zinc-nickel and 500 h and above with a sealer. Confirm the number on the real geometry with the sealer state named.
Q: Can a deep drawn cap be plated on the inside?
A: Not reliably at the innermost internal surface. A one-piece drawn cap has a blind region the bath cannot reach, so that face ends up thin or uncoated and rusts first under salt spray while the exterior still looks sound. The alternatives are a two-piece design plated before assembly, selective masking, or a powder coat applied over the assembly.
Q: Should we rivet before or after plating?
A: Either, but not both, and each choice has a cost. Riveting after plating breaks the coating locally and leaves a bare-steel path; plating after riveting cannot reach the crevice at the joint, which is where salt spray finds water. When both a sealed joint and 240 h or better are required, plate the parts separately, join, then powder coat over the assembly.
Q: Why did a sealer that improved salt spray cause a welding problem?
A: The sealer leaves a thin film over the zinc. Corrosion resistance improves by a large factor, from roughly 140 h to over 500 h, but the film also blocks welding, so earth pins could no longer be welded to the housings and the sealer had to be removed from the specification. List every welding, riveting and staking operation on the part before accepting a sealer.
Q: Can we reduce plating thickness from 15 µm to 5 µm to save cost?
A: Sometimes, but treat it as a specification change rather than a saving. A 5 µm zinc-nickel scheme is a different tolerance proposition from a 15 µm one, and the corrosion result depends heavily on whether a sealer is used. Ask for a salt-spray report on the actual housing at the proposed thickness and sealer state before approving the change.
Q: Why did the plating shop produce the wrong colour?
A: Because the specification used colour words rather than finish definitions. Blue-white and transparent bright describe a trivalent passivate with an iridescent cast; white zinc describes a flatter, more matte deposit, so a request written as anything other than white zinc is open to interpretation. Name the passivate type and the reference area, and where colour is critical send a physical reference part.