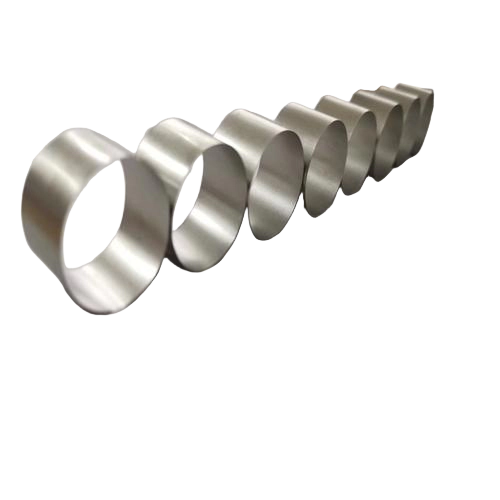
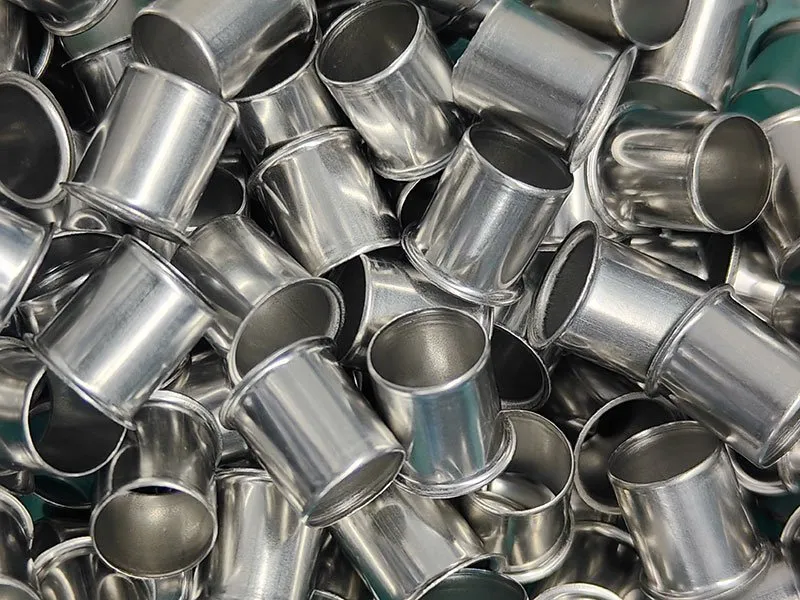
Deep-drawn Magnetic Isolation Sleeve
What is this part? Deep-drawn Magnetic Isolation Sleeve is a Sleeve manufactured from stainless steel by Balford. Production process: Progressive Die Stamping → Deburring → Surface Treatment. Finish: Pickling. Key requirements: Tolerance control when deep drawing extremely thin gauge; grades 304/316 for strength and ductility.

Precision Metal Stamping
| Product Name | Deep-drawn Magnetic Isolation Sleeve |
|---|---|
| Category | Sleeve |
| Process Flow | Progressive Die Stamping→Deburring→Surface Treatment |
| Material | stainless steel |
| Surface Treatment | Pickling |
| Material thickness | Stainless steel disc 0.1-0.3 mm thick |
| Key requirements | Tolerance control when deep drawing extremely thin gauge; grades 304/316 for strength and ductility |
Case Review
The magnetic isolation sleeve for a solenoid valve is typically deep drawn from a stainless steel disc, 0.1–0.3 mm thick. At that gauge, the material is extremely thin, which makes the deep drawing operation genuinely tricky to hold tolerances on. Stainless steel is a solid choice for magnetic sleeves: it gives you good corrosion resistance, consistent mechanical properties, and the magnetic permeability you need. The usual grades are 304 and 316—both have enough strength and ductility to handle deep drawing without cracking or excessive thinning.
What this case is
The magnetic isolation sleeve for a solenoid valve is typically deep drawn from a stainless steel disc, 0.1–0.3 mm thick. At that gauge, the material is extremely thin, which makes the deep drawing operation genuinely tricky to hold tolerances on. Stainless steel is a solid choice for magnetic sleeves: it gives you good corrosion resistance, consistent mechanical properties, and the magnetic permeability you need. The usual grades are 304 and 316—both have enough strength and ductility to handle deep drawing without cracking or excessive thinning.
At a glance
| Field | Published value |
|---|---|
| Application | Sleeve |
| Industry | Solenoid valves |
| Material | stainless steel |
| Surface treatment | Pickling |
| Manufacturing route | Progressive die stamping → Deburring → Surface treatment |
| Material thickness | Stainless steel disc 0.1-0.3 mm thick |
| Key requirements | Tolerance control when deep drawing extremely thin gauge; grades 304/316 for strength and ductility |
Manufacturing route
The published sequence for this part:
- Progressive die stamping
- Deburring
- Surface treatment
What decides the engineering
The route starts with progressive die stamping, which suits a part formed in the strip: coil feeding, piercing, forming and cut-off inside one tool. Strip layout and die stations are the engineering content of the job, and the annual volume decides whether a progressive tool is the right answer.
Two things are settled before tooling: which dimensions actually matter to the assembly - a sealing face, a bearing seat, a coaxial diameter - and what tolerance the process can hold at those features. Everything else follows the general tolerance, which keeps tooling effort where it buys function.
Surface treatment sits at the end of the route. Cleaning and deburring are done in house; plating, phosphating, passivation, electropolishing and coating are placed with qualified external processors and recorded on the inspection plan, and batch heat treatment is handled the same way when the drawing calls for it.
Documentation and first article
A part like this is released with a first article inspection report against the confirmed drawing and a PPAP-aligned package at the level the customer's quality department asks for. Material certificates are kept per heat and IMDS entries are filed on request. The quality system is ISO 9001:2015 with process controls aligned to IATF 16949 requirements.