Magnetic solenoid valve housing specialist
Most of these housings are drawn first and stamped to finish; where the wall is reduced on purpose, the operation is described under deep draw stamping.
Solenoid Housing Specialist
Precision housings for switching and proportional solenoid valves. Pure iron sourcing advantage. Two proven manufacturing routes. Magnetic annealing expertise. Precision machining. High-quality plating.
05 · Every Route We Quote
Every Way a Solenoid Housing Can Be Made
Deep drawing, cold extrusion, cold heading, hot forging, casting with full turning, bar turning and tube turning all produce a working solenoid housing — but not at the same cost, wall thickness or magnetic performance. Balford quotes the route that fits your geometry and volume, and states which steps run in our factory and which are subcontracted.
| Route | How the housing is formed | Raw material | Where it runs |
|---|---|---|---|
| Deep drawing | A sheet blank is drawn into a cup; the bore and bottom are formed in the same press, so there is no longitudinal weld. | Pure iron or 10# steel sheet, 1.0–3.0 mm | In-house: presses 25–350 t, draw dies built in-house |
| Cold extrusion | A bar slug is extruded backwards into a cup; wall and bottom thickness are set by the die, not by turning. | Pure iron or 10# steel bar | In-house |
| Cold heading | Bar is cut and upset; best for short, thick housings where drawing would need too many stages. | Pure iron or 10# steel bar | In-house |
| Hot forging | Bar is heated and forged, then machined; used for heavy sections and coarse geometry. | Pure iron or 10# steel bar | Forged at a qualified partner, finished in-house |
| Casting + full turning | A cast blank is turned inside and out to final size — no forming of the body. | Iron or steel castings | Castings from qualified foundries; all turning in-house |
| Bar turning | The housing is machined from solid bar; OD and bore are produced from one setup, so concentricity is easy to hold. | 1215 free-machining steel bar | In-house CNC turning |
| Tube turning | Tube is cut to length and machined; there is no bottom wall to form. | 10# steel tube or pure iron tube | In-house CNC turning |
Raw material and process route
The material form decides which processes are available: bar can be extruded, headed or forged; tube can be turned but has no bottom to form; sheet is what deep drawing and stamping start from.
| Raw material | Process route | Used for |
|---|---|---|
| 1215 free-machining steel bar | CNC turning | Turned housings with no bottom wall |
| 10# steel tube | CNC turning | Turned housings from tube |
| Pure iron tube | CNC turning | Turned housings where magnetic response matters |
| Pure iron sheet | Deep drawing / stamping | Deep drawn and stamped housings |
| Pure iron bar | Cold extrusion, cold heading or hot forging | Extruded, headed or forged housings |
| 10# steel bar | Cold extrusion, cold heading or hot forging | Extruded, headed or forged housings |
Not sure which route your part needs? Send the drawing and annual volume and we will compare the routes for cost and for magnetic performance before quoting.
06 · Standard Series & Size Range
Solenoid Housing Series We Already Produce
These are the housing series and sizes already running in our tooling and press lines — 37, 45, 54 and 63 series, HydraForce-fit housings, cold extruded housings, roll-clinched, deep drawn parts and deep drawn housings. Use them as a starting point for wall thickness, bottom thickness and center bore; custom sizes are quoted from your drawing.
| Series | Photo | Outer diameter | Height | Wall thickness | Bottom thickness | Center hole |
|---|---|---|---|---|---|---|
| 37 series | 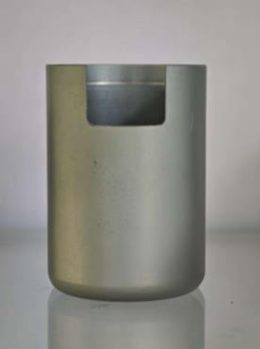 | 37mm | 50mm | 2mm | 4mm | 19mm |
| 37 series | 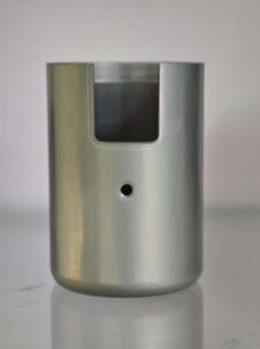 | 37mm | 50mm | 2mm | 4mm | 19mm |
| 37 series | 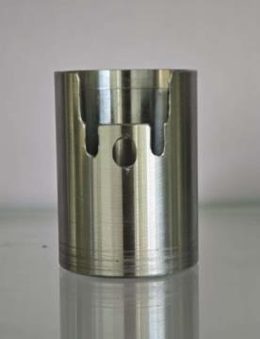 | 37mm | 50mm | 2mm | 4mm | 19mm |
| 37 series | 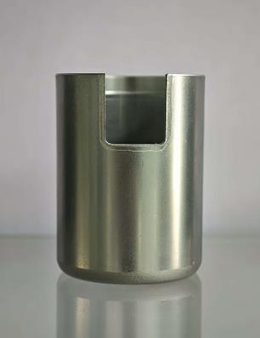 | 37mm | 50mm | 2mm | 4mm | 19mm |
| 45 series | 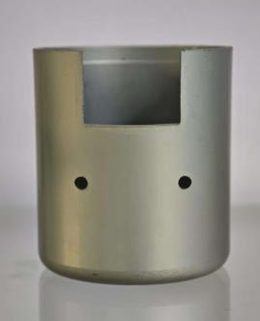 | 45mm | 50.5 | 2mm | 4mm | 23.1mm |
| 45 series | 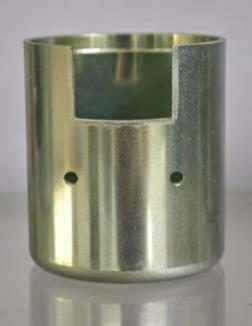 | 45mm | 50.5 | 2mm | 4mm | 23.1mm |
| 45 series | 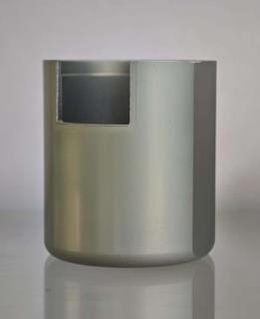 | 45mm | 50.5 | 2mm | 4mm | 23.1mm |
| 45 series | 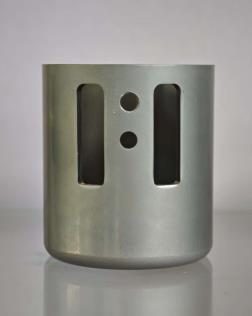 | 45mm | 50.5 | 2mm | 4mm | 23.1mm |
| 45 series | 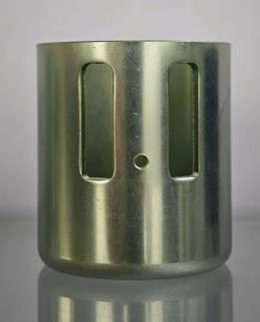 | 45mm | 50.5 | 2mm | 4mm | 23.1mm |
| 45 series | 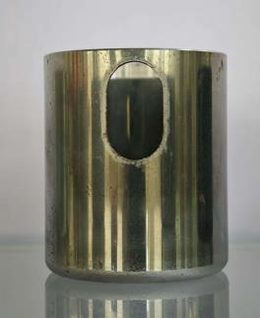 | 45mm | 50.5 | 2mm | 4mm | 23.1mm |
| 54 series | 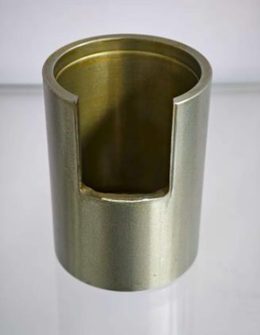 | 54mm | — | 3mm | — | — |
| 63 series | 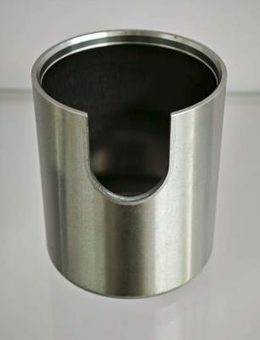 | 63mm | 74mm | 3mm | 6mm | 31.6mm |
| 63 series | 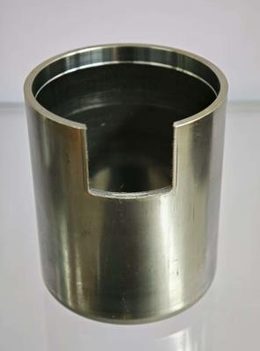 | 63mm | 74mm | 3mm | 6mm | 31.6mm |
| HydraForce series | 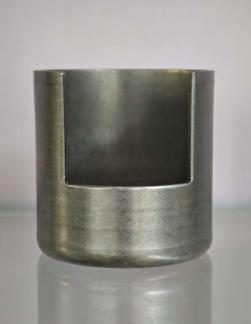 | 46mm | 42.5mm | 2mm | 2mm | none |
| HydraForce series | 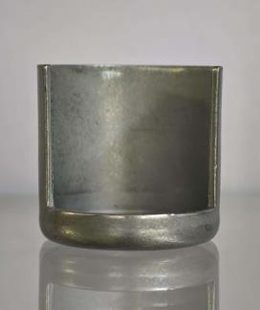 | 36mm | 32mm | 2mm | 2mm | none |
| Cold extrusion series | 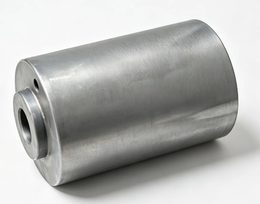 | 37 | 58mm | 2.5mm | 10mm | 10mm |
| Cold extrusion series | 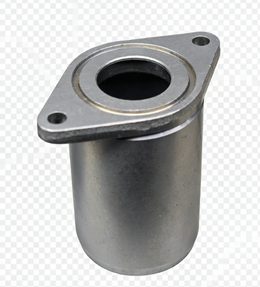 | 32mm | 51mm | 2mm | 4.5mm | 16mm |
| Cold extrusion series | 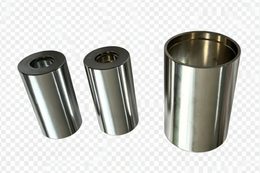 | 24mm | 49mm | 1.5 | 6mm | 9mm |
| Cold extrusion series | 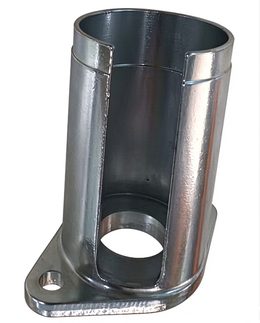 | 33mm | 58mm | 2 | 5mm | 12mm |
| Roll-clinch | 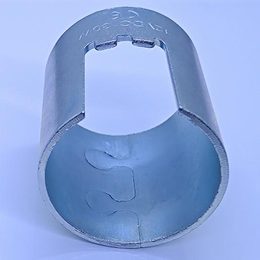 | 45 | 50 | 2 | none | none |
| Deep drawn | 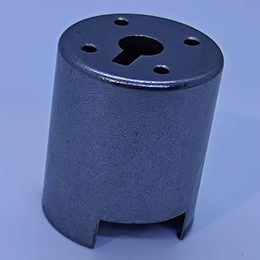 | 27mm | 30mm | 2mm | 2mm | 6mm |
| Deep drawn | 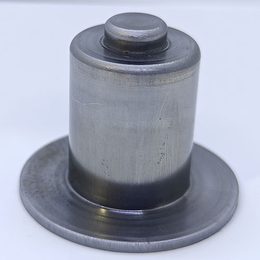 | 32mm | 46mm | 1.5mm | 2mm | none |
| Deep drawn | 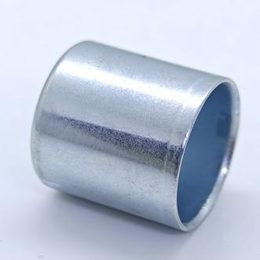 | 18mm | 18.9mm | 1mm | 1.2mm | 8mm |
| Deep drawn | 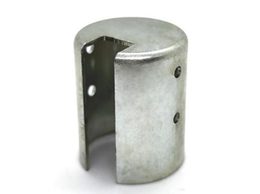 | 18mm | 25mm | 1mm | 1.2mm | none |
| Deep drawn housing | 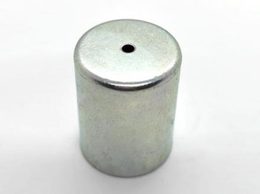 | 20mm | 30mm | 1mm | 1.2mm | 2mm |
| Deep drawn housing | 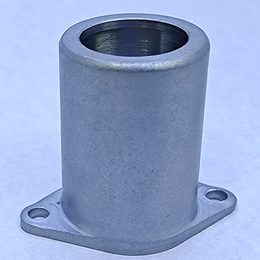 | 29.5mm | 42.4mm | 1.75 | 2.2mm | 21mm |
“None” means the drawing does not call for that feature (for example no center hole on a closed housing). Dimensions are millimetres and are finished-part sizes.
Why the housing is critical
The Solenoid Housing Carries the Whole Function
A solenoid housing — also called a solenoid valve housing or a solenoid can — is not an ordinary metal shell. It carries the coil, guides the armature, seals the working fluid and completes the magnetic circuit. Every one of those functions depends on material, geometry and surface quality that Balford controls from the first forming step to final inspection.
Carries the Coil
The OD defines coil fit, external appearance and assembly interface. Dimensional consistency here decides how cleanly the coil assembly drops into production.
Guides the Armature
The ID controls armature and plunger guidance, internal clearance and the magnetic circuit. Tight, repeatable ID geometry is what makes valve response predictable.
Seals & Performs
Sealing interfaces, roundness and concentricity determine leak-tight assembly — and for proportional valves, magnetic performance decides force, response and repeatability.
01 · Material Advantage
Competitive Pure Iron Sourcing
Balford has an exceptionally strong sourcing network for the pure iron used in magnetic solenoid housings. Our purchasing advantage flows directly into the material cost of your program.
Our sourcing advantage can reduce pure-iron material cost by approximately 40% versus typical market purchasing levels in comparable programs.
Internal sourcing analysis — savings vary by grade, specification and program volume. Please discuss your exact material requirements with our engineers.
02 · Magnetic Engineering
Coercivity Matters
For magnetic solenoid valve housings, dimensional accuracy is only part of the story — magnetic performance matters. One of the key magnetic indicators is coercivity (Hc). Cold rolling, cold extrusion and deep drawing can increase residual stress and consequently increase coercivity. This is particularly important for proportional solenoid valves, where magnetic characteristics directly influence force, response and repeatability.
From forming stress to magnetic performance
- Forming introduces plastic deformation and residual stress into magnetic materials.
- Residual stress can increase coercivity and reduce magnetic performance.
- For critical applications Balford uses controlled magnetic annealing to restore magnetic properties after forming and machining.
- Lower coercivity means more stable force and more repeatable proportional-valve behaviour.
03 · Process Expertise
Magnetic Annealing: From Forming Stress to Magnetic Performance
Why annealing matters
- Forming creates residual stress.
- Residual stress increases coercivity.
- Magnetic annealing relieves internal stress and improves magnetic properties.
- For proportional valves this can be critical to achieving stable magnetic force and repeatable performance.
Balford has developed dedicated in-house magnetic annealing know-how for solenoid valve components — process windows, demagnetisation behaviour and magnetic-property changes across materials and forming states. Our in-house capability can provide substantial processing-cost savings compared with outsourced or conventional annealing solutions.

04 · Two Manufacturing Routes
Cold Extrusion or Deep Drawing — Both In-House
Balford evaluates both routes for every solenoid housing and recommends the more economical manufacturing solution based on geometry, wall thickness, material, volume, dimensional requirements and magnetic performance.
Cold Extruded Housing
for demanding proportional valves- High dimensional consistency
- Excellent concentricity
- Strong structural integrity
- Suitable for demanding proportional valves
- Excellent control of ID / OD geometry
- Good surface quality after precision machining
* Magnetic annealing is typically required for proportional-valve applications where magnetic performance is critical.
Deep Drawn Housing
efficient high-volume production- High material utilization
- Efficient for high-volume production
- Competitive manufacturing cost
- Excellent repeatability with controlled tooling
- Suitable for switching valve housings
- Can be optimized for proportional valve applications
* Magnetic annealing is typically applied for proportional-valve applications. Switching-valve housings generally do not require the same magnetic annealing process. Final process selection depends on material, valve design and magnetic requirements.
07 · Engineering Comparison
Switching Valve vs Proportional Valve Housing
Not every solenoid valve housing needs the same process. Balford selects the process from the valve application — not from a fixed template.
| Requirement | Switching Solenoid Valve | Proportional Solenoid Valve |
|---|---|---|
| Housing | Critical | Critical |
| Dimensional accuracy | High | Very High |
| Magnetic properties | Important | Extremely important |
| Forming stress | Needs control | Needs strict control |
| Magnetic annealing | Often not required | Typically required |
| Coercivity control | Important | Key parameter |
| CNC machining | Required | Required |
| Plating | Application dependent | Application dependent |
Applications
Where these housings are used
Most enquiries in this family arrive from four places. The drawings differ, the process logic does not.
- Transmission and shift solenoids — see the automatic transmission solenoid valve housing case.
- Brake and stability control — the brake solenoid magnetic shield case.
- Air suspension ride height — the air suspension solenoid housing case.
- ESC and ABS coil housings — the coil housing for the ESC/ABS solenoid case.
- Hydraulic and pneumatic valve bodies — directional, proportional and pilot-operated housings follow the same drawing rules; the process comparison for proportional housings is in section 05.
08 · Surface & Geometry
A Solenoid Housing Should Look Like a Precision Tube
Deep drawing can leave visible circumferential marks on the outside diameter. For solenoid valve manufacturers, this is not always acceptable. Balford controls tooling, material condition, forming parameters, machining and surface finishing to achieve a cleaner, more continuous OD appearance.
Our target: Smooth. Bright. Continuous. Consistent.
Not: Heavy drawing rings. Uneven surface. Visible forming marks.
The OD affects
- Coil fit
- External appearance
- Assembly interface
- Dimensional consistency
The ID affects
- Armature / plunger guidance
- Internal clearance
- Magnetic circuit
- Sealing / assembly & function
Balford controls the complete housing geometry — not just the outside diameter. OD appearance and ID precision are engineered together.
09 · Complete Capability
One Supplier. The Complete Solenoid Housing Process.
Balford is not a general metal parts supplier that happens to make solenoid housings. We are a specialist manufacturer built around solenoid valve housings and the magnetic manufacturing technologies behind them.
Pure Iron Sourcing
Significant material-cost advantage through our sourcing network.
Cold Extrusion
For high-performance, precision housings with excellent concentricity.
Deep Drawing
For efficient high-volume production with high material utilization.
Precision CNC Machining
Critical OD / ID / concentricity control after forming.
Magnetic Annealing
For proportional-valve magnetic performance.
Plating & Inspection
Controlled protection and appearance, plus dimensional, visual and magnetic performance control.
10 · Total Cost
Why Balford Can Be Cost Competitive
Cost advantage through manufacturing expertise — we are cost-efficient because we control the process better, not because quality is compromised.
Strong pure-iron sourcing — potentially ~40% material-cost advantage in comparable programs.
In-house process expertise — potentially ~50% of conventional external processing cost in applicable programs.
Two process routes — cold extrusion or deep drawing, selected according to product geometry, magnetic requirements and volume.
Lower Total Cost Without Treating Quality as a Commodity
Material → Forming → Machining → Magnetic Treatment → Plating → Inspection — one integrated process under one roof.
11 · Proof
Solenoid Housing Case Studies
Real programs, documented engineering decisions — application, material, manufacturing route, machining, magnetic treatment, plating and critical requirements for each housing.
12 · FAQ
Solenoid Housing — Engineering Answers
What materials are used for solenoid valve housings?
Balford works with magnetic steels and pure iron grades such as DC04, SPHE, DT4 and DT4C, depending on the valve design and magnetic requirements.
Does a solenoid valve housing require magnetic annealing?
Not always. Switching valve housings may not require magnetic annealing. For proportional valves, magnetic annealing is typically much more important because coercivity and magnetic permeability directly affect magnetic performance.
Why does cold extrusion or deep drawing increase coercivity?
Plastic deformation introduces residual stress and changes the magnetic domain structure of the material, which can increase coercivity.
Which is better: cold extrusion or deep drawing?
Neither is universally better. The correct route depends on geometry, wall thickness, material, production volume, dimensional requirements and magnetic performance. Balford can evaluate both routes and recommend the more economical manufacturing solution.
Can Balford control both the ID and OD?
Yes. Balford combines forming and precision CNC machining to control critical internal and external dimensions.
Can Balford achieve a smooth OD surface after deep drawing?
Yes. Surface quality is a major consideration for solenoid housings. Balford optimizes tooling, material condition, forming and secondary machining to reduce visible drawing marks and achieve a smoother, more continuous OD appearance.
Can Balford provide magnetic annealing?
Yes. Balford has dedicated magnetic annealing process expertise for solenoid valve components and can evaluate the required process based on material, forming history and magnetic requirements.
Your Solenoid Housing Starts Here.
Whether you need a switching-valve housing or a high-performance proportional-valve housing, Balford can help you select the right material, forming process, machining route and magnetic treatment.
Cold Extrusion · Deep Drawing · CNC Machining · Plating · Magnetic Annealing
One manufacturing partner. One complete housing solution.
BALFORD — THE SOLENOID HOUSING SPECIALIST
Next steps for this part family
- Solenoid valve housing guide — material, forming route, coercivity and magnetic annealing in one document (also as a 10-page PDF).
- DFM review — send the drawing and get the process route and risk list before quoting.
- In-house tooling design & build — the dies behind these parts are built in our own tool room.
- Deep drawing capability — presses up to 350 t and draw diameters up to Ø250 mm.
- PPAP capability — Level 3 documentation for automotive programs.
- Aluminium stamping & deep drawing — grades, formability and what changes versus steel.
Related: ironing in deep drawing — how a thinned wall holds both the inside and the outside diameter · ironing instead of turning · ironing for solenoid valve housings (DT4E, DC04) · ironing tolerances and surface finish
Related reading: if you arrived from a repair question rather than a sourcing one, the failure modes and the diagnostic sequence for the fuel metering unit valve are written up in fuel metering unit valve failure and treatment.
These housings are drawn on presses up to 350 t — see the equipment list and the transfer press stamping process page.
Tolerance and appearance questions on drawn housings are answered here: housing tolerances and cosmetic standards.
Capacity at a glance: press capacity up to 350 t · maximum deep draw diameter Ø250 mm · full machinery and inspection list.
Most solenoid housings start as a prototype on single-operation tooling before moving to transfer or progressive production — see low volume stamping and prototyping.
The choice between DC04 and pure iron, and what the drawing route does to the magnetic result, is set out on the DC04 and pure iron material guide.